Understanding the operational mechanics and distinctive attributes of a multi-functional powder handling system is crucial for industries that rely on efficient material transfer and processing. This article delves into the core components, working principles, and key features that define such systems, providing a comprehensive overview for professionals seeking reliable solutions for their powder handling needs.
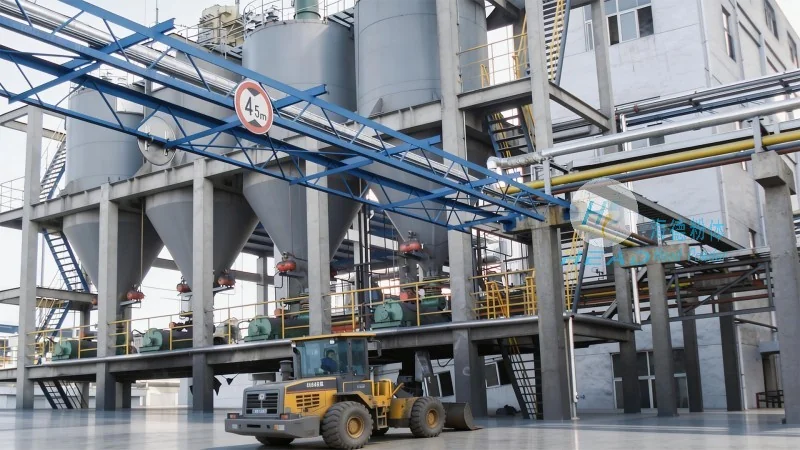
Working Principle of the Multi-functional Powder Handling System
The multi-functional powder handling system operates on a sophisticated mechanism designed to manage the entire lifecycle of powder materials, from storage to discharge. At its core, the system integrates several key components, including a hopper for material storage, a feeder to control the flow rate, and a conveyor or pneumatic transport system for movement. The working principle involves the following sequential steps:
First, the powder is loaded into the hopper, which is typically equipped with a lid to prevent contamination and maintain material integrity. The feeder, often a rotary valve or a vibratory feeder, regulates the flow of powder from the hopper to the transport section. This controlled feeding ensures consistent material delivery, which is critical for maintaining process stability and preventing overloading or underloading of downstream equipment.
Next, the powder is transferred through the conveyor or pneumatic system. For systems utilizing pneumatic transport, compressed air is used to create a flow of powder particles, moving them from the source to the destination. The velocity and pressure of the air are carefully controlled to ensure efficient transport without causing particle degradation or excessive wear on components. In contrast, mechanical conveyors rely on rotating belts or screws to move the powder, offering a more direct and energy-efficient method for certain applications.
The system also incorporates monitoring and control features to optimize performance. Sensors are used to track the level of material in the hopper and the flow rate through the feeder, providing real-time data that can be used to adjust operational parameters. This feedback loop enhances the system's adaptability, allowing it to respond to changes in material characteristics or process demands.
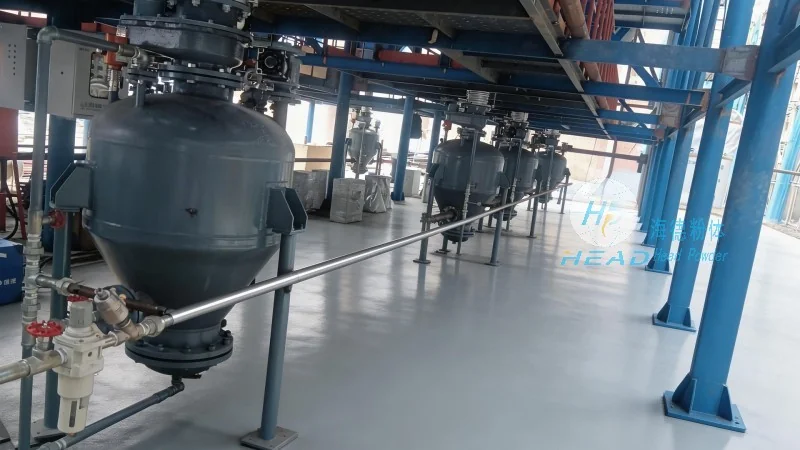
Key Features and Advantages of the System
The multi-functional powder handling system is characterized by several features that set it apart from traditional handling solutions, making it an ideal choice for diverse industrial applications. These features include:
1. **Versatility in Material Handling**: The system is designed to handle a wide range of powder types, including fine powders, granules, and bulk materials. This versatility is achieved through adjustable parameters such as feeder speed, air pressure, and conveyor speed, allowing the system to accommodate different material properties and sizes.
2. **Efficient and Low Maintenance Operation**: The system is engineered for minimal maintenance, with components that are durable and resistant to wear from abrasive powders. Regular maintenance is reduced through the use of high-quality materials and robust design, ensuring long-term reliability and cost-effectiveness.
3. **Safety and Environmental Compliance**: Safety is a top priority in the design of the system. Features such as dust collection systems, explosion-proof components, and enclosed structures help to minimize the risk of dust explosions and ensure compliance with environmental regulations. The system also reduces material loss and contamination, contributing to a cleaner and more sustainable operation.
4. **Customization and Scalability**: The system can be customized to meet specific customer requirements, including different sizes, material capacities, and integration with existing production lines. Its modular design allows for easy expansion or modification as production needs evolve, providing a flexible solution for growing businesses.
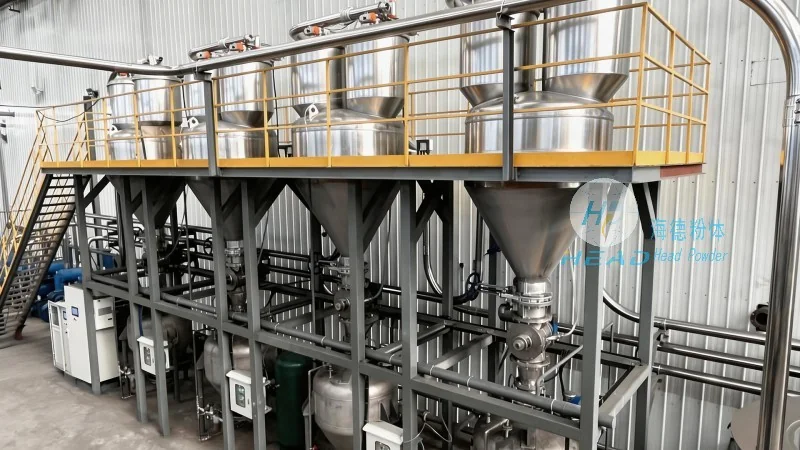
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of advanced powder handling systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for industries requiring reliable and efficient material transfer solutions. HeadPowder's products are designed to meet the highest standards of performance, safety, and durability, ensuring that customers receive systems that are tailored to their unique needs.
HeadPowder's team of engineers and technicians brings extensive experience in powder technology, ensuring that each system is developed with a deep understanding of the challenges faced by industrial users. The company's focus on research and development has led to the creation of cutting-edge solutions that address the evolving demands of modern manufacturing processes.
HeadPowder's facilities are located in Shandong, China, where the company leverages its local resources and expertise to deliver high-quality products and services. The company adheres to strict quality control measures throughout the manufacturing process, from raw material selection to final assembly, ensuring that every system meets the rigorous standards of the industry.
By combining advanced technology with a customer-centric approach, HeadPowder has built a reputation for delivering solutions that not only meet but exceed customer expectations. The company's dedication to excellence and continuous improvement has made it a preferred choice for businesses seeking to enhance their powder handling operations and improve overall productivity.




