For industrial applications that require efficient and reliable material handling, the powder silo pneumatic conveying system stands out as a sophisticated solution. This system is designed to transport bulk powders and granular materials from storage silos to processing units or other destinations with minimal human intervention. The technology behind this system leverages the principles of air movement to create a seamless flow of materials, ensuring consistent performance and operational efficiency.
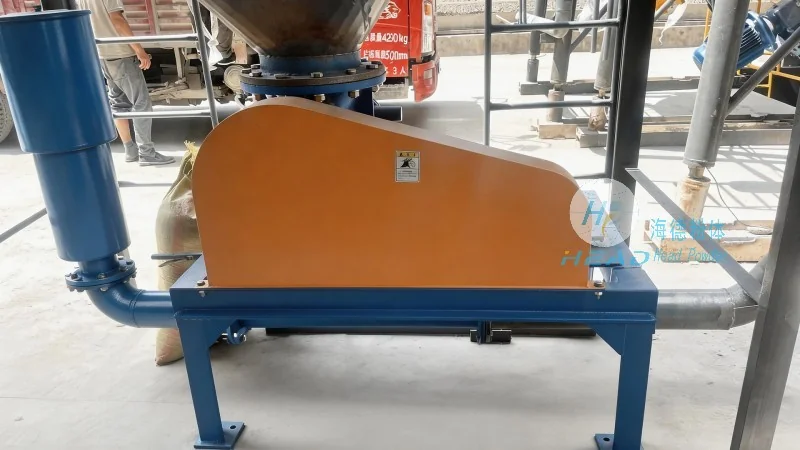
Working Principle of the Powder Silo Pneumatic Conveying System
The core mechanism of the powder silo pneumatic conveying system revolves around the use of compressed air to create a pressure differential that propels material through a network of pipes. At the heart of the system is the powder silo, which serves as the storage container for bulk materials. The system typically operates in two main modes: dilute phase and dense phase, each tailored to different material characteristics and application requirements.
In the dilute phase operation, compressed air is introduced into the silo at a relatively high velocity, creating a cloud of material suspended in the air. This mixture is then drawn through the conveying line by the pressure differential, moving the material from the silo to the discharge point. The velocity of the air is carefully controlled to ensure that the material particles remain suspended without settling or clogging the system. This mode is ideal for materials that are free-flowing and non-abrasive, such as flour, cement, or powdered chemicals.
Conversely, the dense phase operation uses a lower air velocity and higher material concentration, resulting in a more compact flow of material. This method is particularly effective for handling materials that are abrasive, sticky, or prone to bridging in the silo. The dense phase system reduces the risk of material degradation and equipment wear, making it suitable for applications involving sensitive or high-value powders.
Key Features of the Powder Silo Pneumatic Conveying System
The powder silo pneumatic conveying system offers several distinct advantages that make it a preferred choice in various industries. One of the most notable features is its ability to handle a wide range of materials, from fine powders to coarse granules, without the need for mechanical components like screws or belts. This eliminates the risk of material contamination and reduces maintenance requirements, as there are fewer moving parts in the system.
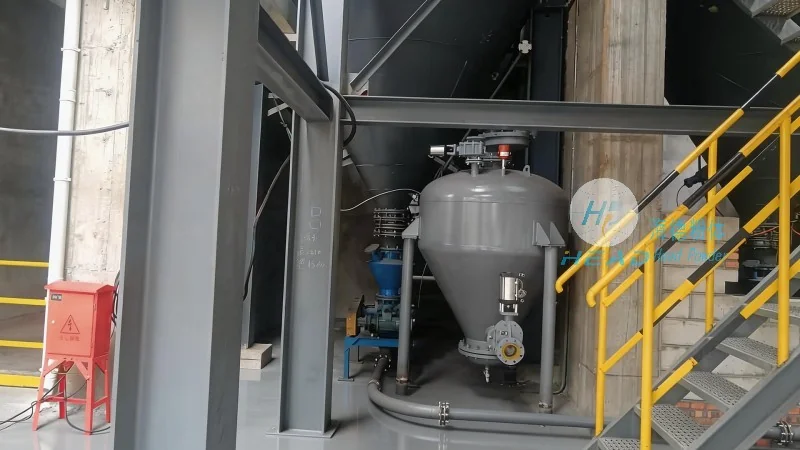
Another key feature is the system's flexibility in terms of layout and integration. The conveying lines can be configured in various configurations, including straight, curved, or even vertical and horizontal combinations, to accommodate the specific spatial constraints of a facility. This adaptability allows for seamless integration with existing processing equipment, minimizing the need for extensive modifications to the plant layout.
The system also provides excellent control over material flow, enabling precise dosing and dosing rates. This is achieved through the use of control valves and pressure sensors that regulate the air flow and material discharge. The ability to adjust the conveying rate in real-time allows operators to match production demands and maintain consistent product quality, which is critical in industries such as pharmaceuticals, food processing, and chemical manufacturing.
Furthermore, the powder silo pneumatic conveying system offers enhanced safety and hygiene. By eliminating the need for manual handling of powders, the system reduces the risk of dust exposure and cross-contamination. The enclosed conveying lines prevent dust from escaping into the environment, ensuring compliance with occupational health and safety regulations. This feature is particularly important in industries where product purity and worker safety are paramount.
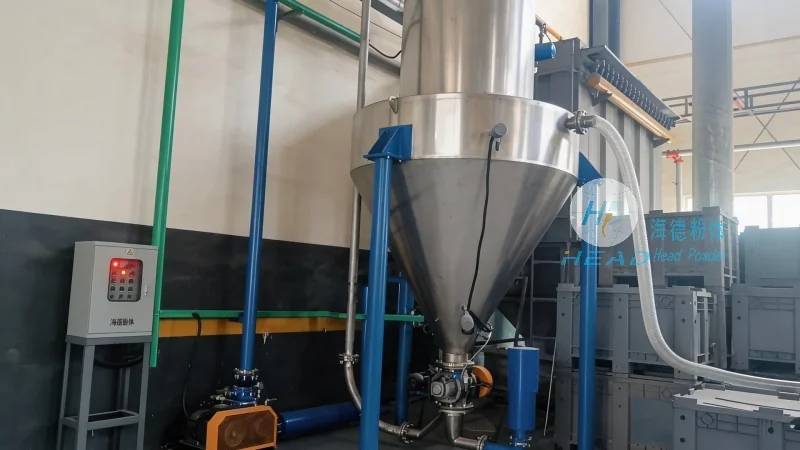
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of advanced material handling solutions. With its headquarters located in Shandong, China, the company specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the unique needs of various industries. HeadPowder's commitment to innovation and quality has established it as a trusted partner for businesses seeking reliable and efficient material transport solutions.
The company's team of experienced engineers and technicians works closely with clients to understand their operational requirements and develop customized solutions that optimize material flow, reduce downtime, and enhance overall productivity. By leveraging cutting-edge technology and rigorous quality control processes, HeadPowder ensures that its systems meet the highest standards of performance and durability.
HeadPowder's product portfolio includes a wide range of pneumatic conveying equipment, from basic dilute phase systems to advanced dense phase and pressure vessel systems. The company also provides comprehensive after-sales support, including installation, commissioning, and maintenance services, to ensure that its clients receive long-term value from their investments.
With a strong focus on customer satisfaction and technical excellence, Shandong HeadPowder Engineering Co., Ltd. continues to set new standards in the material handling industry. Its dedication to innovation and quality has earned it a reputation as a reliable and innovative partner for businesses worldwide.




