Manganese carbonate is a critical industrial chemical widely utilized in battery manufacturing, steel production, and various chemical processes. The efficient and reliable transportation of this material is essential for maintaining production efficiency and ensuring product quality. This article explores specialized equipment designed for handling manganese carbonate, focusing on the key design principles that underpin these systems.
Introduction to Manganese Carbonate Material Handling Equipment
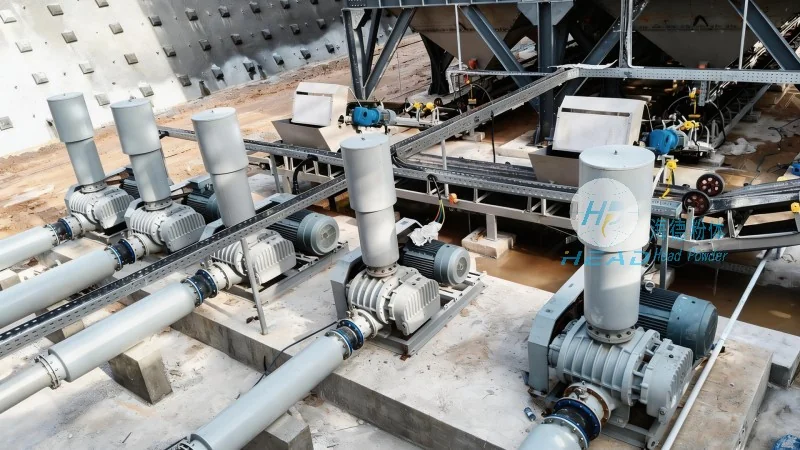
Manganese carbonate material handling equipment is specifically engineered to manage the unique properties of manganese carbonate, such as its fine particle size, potential for dust generation, and chemical reactivity. These systems are designed to minimize material loss, prevent contamination, and ensure safe operation in industrial settings. The equipment typically includes components like feeders, conveyors, and storage silos, all tailored to the demands of manganese carbonate processing.
Key Design Principles of Manganese Carbonate Handling Systems
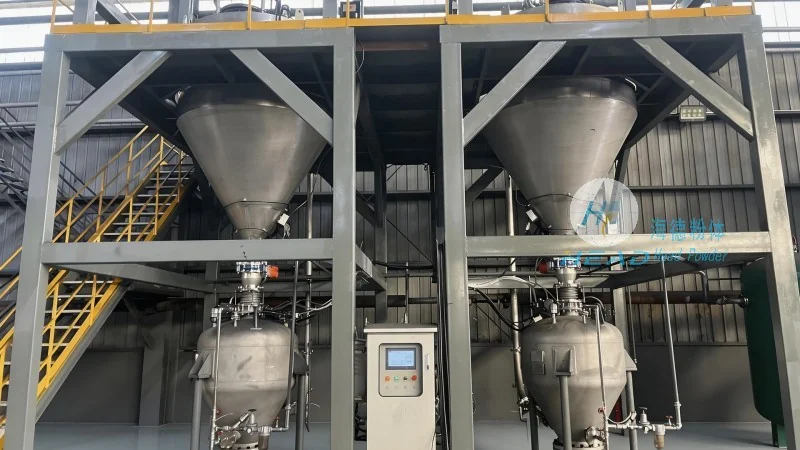
The design of manganese carbonate material handling equipment revolves around several critical principles to ensure optimal performance. First, durability and wear resistance are paramount due to the abrasive nature of the material. Components such as hoppers, chutes, and conveyor belts are constructed from high-quality materials like stainless steel or specialized alloys to withstand continuous exposure to manganese carbonate particles. Second, airtight and dust-proof designs are essential to prevent dust emissions and maintain a safe working environment. This often involves the use of sealed systems and advanced filtration technologies. Third, efficiency and low maintenance are key considerations. The equipment is engineered to minimize energy consumption while maximizing throughput, with features like variable speed drives and automated controls to optimize operation. Additionally, safety is a top priority, with integrated safety features like emergency stops and overload protection to safeguard operators and equipment.
HeadPowder's Approach to Manganese Carbonate Material Handling Solutions
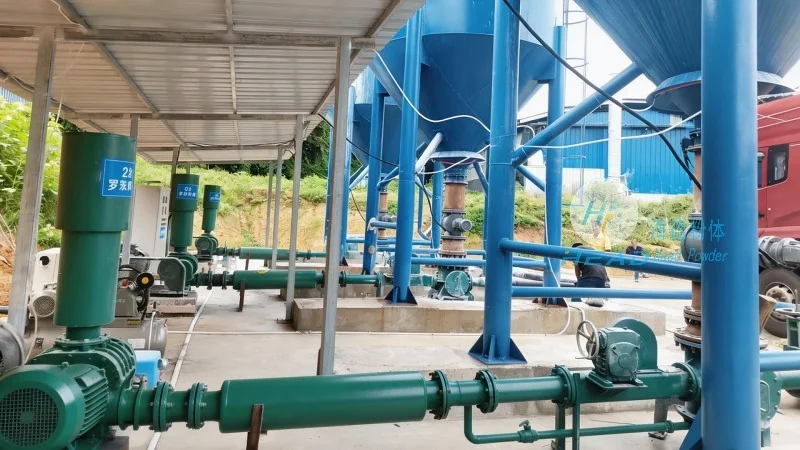
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in providing customized material handling solutions for manganese carbonate and other industrial materials. With years of experience in the field, HeadPowder understands the unique challenges associated with handling manganese carbonate and designs equipment that addresses these challenges effectively. The company's approach emphasizes a combination of robust engineering, advanced materials, and customer-centric design. For instance, their conveyor systems are designed with adjustable speed controls to accommodate varying production rates, while their storage silos feature integrated dust collection systems to maintain air quality. HeadPowder also offers comprehensive after-sales support, including maintenance services and technical assistance, to ensure long-term reliability of their equipment.
Practical Applications and Operational Benefits
Manganese carbonate material handling equipment is widely used in various industrial applications, including battery production facilities, chemical plants, and mining operations. In battery manufacturing, for example, the equipment is used to transport manganese carbonate from storage to processing lines, where it is converted into other chemical forms for battery production. The benefits of using specialized equipment include improved production efficiency, reduced material loss, and enhanced safety for operators. Additionally, the equipment's design minimizes the risk of dust-related health issues and environmental contamination, aligning with modern industrial safety standards. The reliability of these systems also contributes to consistent product quality, which is crucial for meeting customer specifications and regulatory requirements.
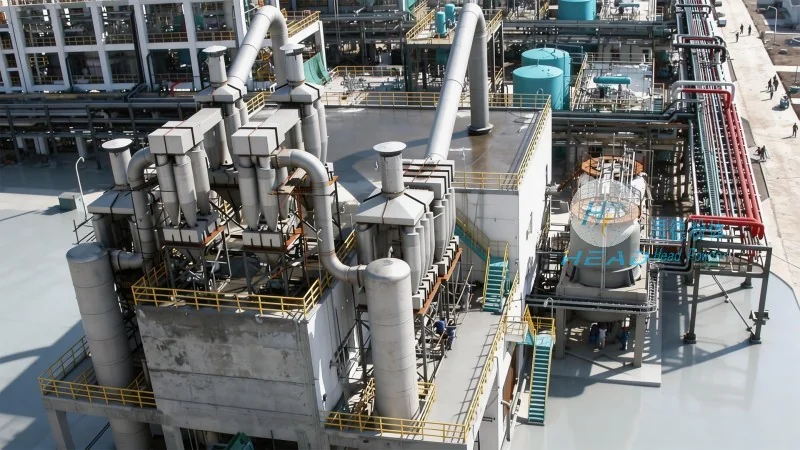
In conclusion, manganese carbonate material handling equipment is a vital component of modern industrial operations, and its design is guided by principles that prioritize durability, safety, and efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in developing and providing these specialized systems, ensuring that industries can handle manganese carbonate safely and effectively. The continued advancement of material handling technology will further enhance the performance and reliability of these systems, supporting the growth of industries that rely on manganese carbonate as a key raw material.




