HeadPowder, a prominent name in the field of powder and capsule handling, specializes in advanced conveying technologies. Based in Shandong, China, the company has established itself as a key player in providing efficient and reliable solutions for capsule transportation. This article explores the various methods of capsule conveying and highlights the benefits of pneumatic conveying systems, a preferred choice for many industries.
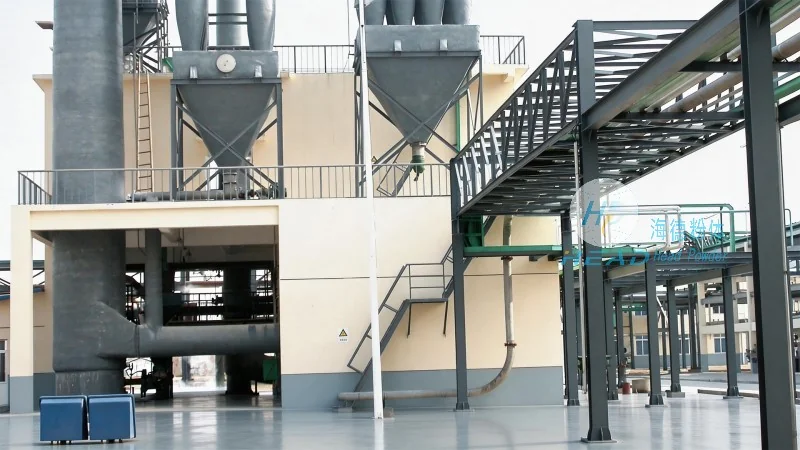
Understanding Capsule Conveying Methods
Capsule conveying is a critical process in pharmaceutical and food industries, where the safe and efficient transport of capsules from one location to another is essential. There are several conventional methods used for capsule handling, including manual handling, belt conveyors, and mechanical screw conveyors. However, these methods often face challenges such as product damage, contamination risks, and limited throughput. In contrast, pneumatic conveying offers a more sophisticated approach to address these issues.
Introducing Pneumatic Conveying for Capsules
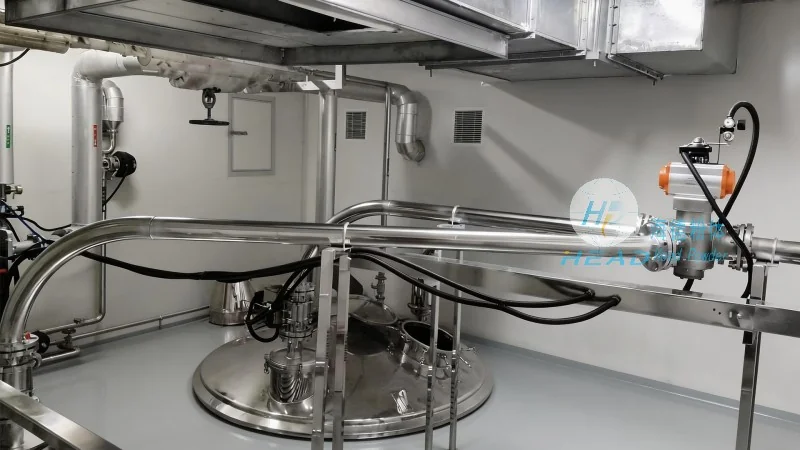
Pneumatic conveying, also known as air conveying, utilizes compressed air to transport capsules through a pipeline system. This method is widely adopted due to its ability to handle delicate products like capsules without causing breakage or deformation. The system typically consists of a hopper, a venturi or rotary valve, and a receiver, all connected by a network of pipes. The compressed air creates a flow that propels the capsules through the system, ensuring a smooth and controlled movement.
Advantages of Pneumatic Conveying for Capsules
One of the primary advantages of pneumatic conveying for capsules is its gentleness. Unlike mechanical conveyors that can exert pressure on capsules, pneumatic systems use air pressure to move products, minimizing the risk of damage. This is particularly important for pharmaceutical capsules, which may contain sensitive ingredients that require careful handling. Additionally, pneumatic conveying systems are highly flexible, allowing for easy integration into existing production lines and the ability to transport capsules over long distances without the need for multiple transfer points.
Key Features of Pneumatic Capsule Conveying Systems
Modern pneumatic capsule conveying systems from HeadPowder are equipped with several features that enhance their performance and reliability. These systems are designed to handle a wide range of capsule sizes and shapes, ensuring compatibility with various product specifications. The use of high-quality materials, such as stainless steel, ensures durability and resistance to corrosion, which is crucial for maintaining product purity. Furthermore, advanced control systems allow for precise regulation of air pressure and flow rates, optimizing the conveying process and reducing energy consumption.
Applications and Industries
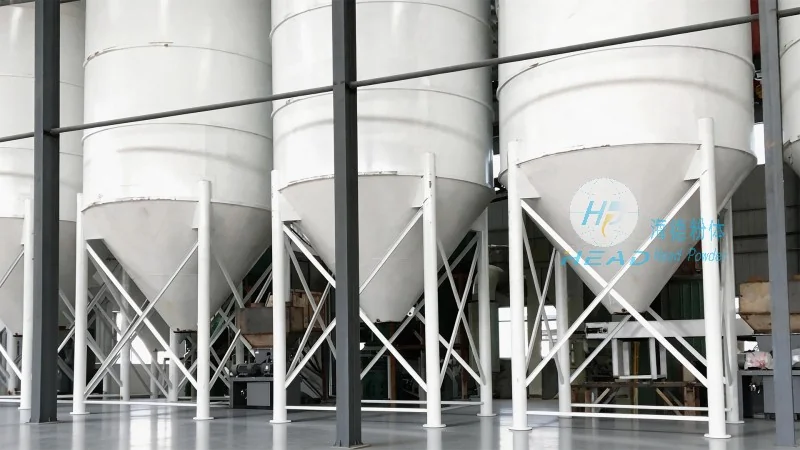
Pneumatic capsule conveying is widely used in the pharmaceutical, food, and nutraceutical industries. In pharmaceutical manufacturing, it is essential for transporting finished capsules from the filling line to packaging units. The system ensures that capsules are delivered in a clean and hygienic manner, meeting stringent regulatory requirements. In the food industry, pneumatic conveying is used for handling capsules containing vitamins, minerals, or other dietary supplements, where maintaining product integrity is paramount. The versatility of pneumatic systems makes them suitable for various applications, from small-scale production to large-scale industrial operations.
Conclusion
HeadPowder's expertise in pneumatic conveying technology provides industries with a reliable and efficient solution for capsule transportation. By leveraging the advantages of air-based systems, companies can improve product quality, reduce operational costs, and enhance overall production efficiency. With a strong presence in Shandong, China, HeadPowder continues to innovate and deliver cutting-edge conveying solutions that meet the evolving needs of the market. For businesses seeking to optimize their capsule handling processes, pneumatic conveying remains a top choice, offering a balance of performance, reliability, and cost-effectiveness.




