HeadPowder, a leading provider in the material handling industry, specializes in advanced conveyor systems designed to enhance efficiency and safety in material transport. This article delves into the concept of negative pressure suction material handling conveyors, exploring their design principles and operational benefits.
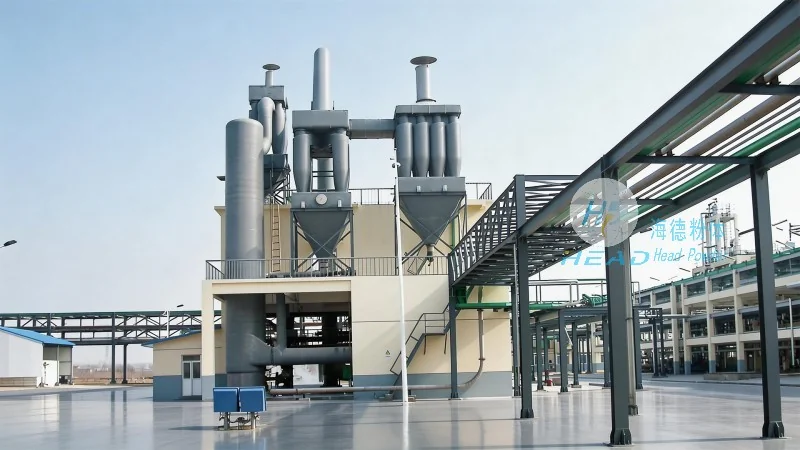
Understanding Negative Pressure Suction Material Handling Conveyors
A negative pressure suction material handling conveyor is a specialized system that uses a vacuum or negative pressure to draw materials from a source and transport them to a destination. Unlike traditional conveyor systems that rely on mechanical force, such as belts or rollers, this type of conveyor leverages the principle of suction to move bulk materials, powders, or granules with minimal friction and reduced risk of contamination. The system operates by creating a low-pressure environment at the intake point, which pulls the material into the conveyor pipe, and then transports it to the discharge point through a sealed system.
Key Design Principles of Negative Pressure Suction Conveyors
The design of a negative pressure suction conveyor is centered around several critical principles that ensure optimal performance and reliability. First, the system must maintain a consistent negative pressure throughout the pipeline to ensure continuous material flow. This is achieved through the use of high-efficiency vacuum pumps and carefully engineered suction nozzles that minimize pressure drop and air leakage. Second, the conveyor pipe is typically made of durable materials, such as stainless steel or food-grade plastic, to withstand the abrasive nature of the materials being transported and to prevent contamination. The pipe is also designed with smooth internal surfaces to reduce friction and prevent material buildup, which can lead to blockages or reduced efficiency.
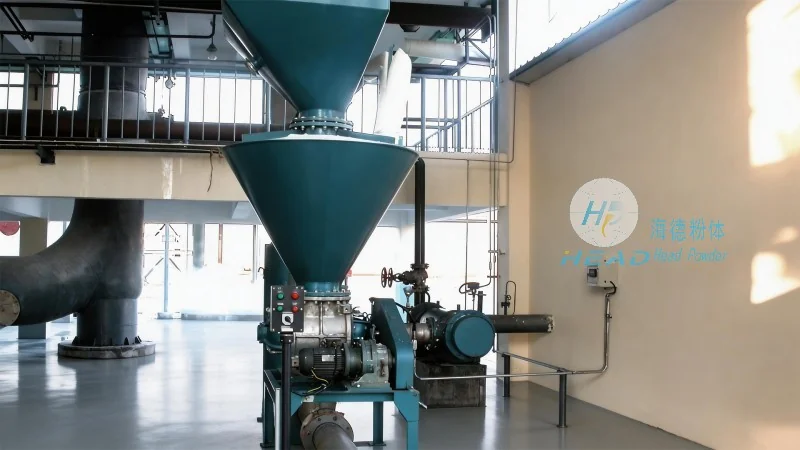
Third, the system incorporates advanced control mechanisms that monitor and regulate the pressure and flow rate. These controls ensure that the conveyor operates within safe and efficient parameters, preventing overloading or underperformance. Additionally, the design includes features such as automatic shut-off valves and pressure sensors that detect any anomalies, such as blockages or leaks, and trigger appropriate responses to maintain system integrity. The integration of these design elements results in a conveyor system that is both reliable and user-friendly, requiring minimal maintenance and downtime.
Operational Benefits and Applications
Negative pressure suction material handling conveyors offer several advantages over traditional conveyor systems, making them ideal for a wide range of industrial applications. One of the primary benefits is the ability to transport materials in a sealed environment, which prevents dust, debris, or contaminants from escaping into the air. This is particularly important in industries such as pharmaceuticals, food processing, and chemical manufacturing, where product purity and environmental safety are paramount. The sealed system also reduces the risk of cross-contamination between different materials, ensuring that each product remains clean and free from impurities.
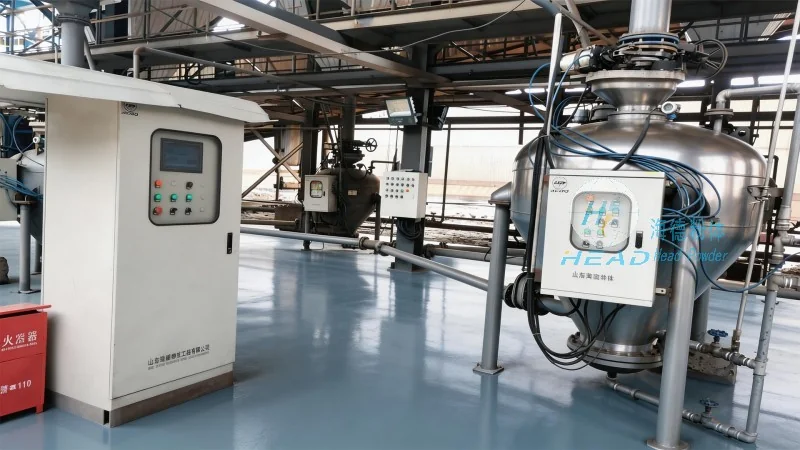
Another significant advantage is the reduced noise and vibration compared to mechanical conveyors. The suction-based operation is much quieter and less disruptive, making it suitable for use in environments where noise control is a concern. Additionally, the system is highly flexible and can be easily adapted to different layouts and production requirements. The conveyor pipes can be bent and routed around obstacles, allowing for customized solutions that fit the specific needs of a facility. This flexibility makes negative pressure suction conveyors a versatile choice for various material handling tasks, from small-scale operations to large-scale industrial plants.
Conclusion
HeadPowder's negative pressure suction material handling conveyors represent a cutting-edge solution for efficient and safe material transport. By leveraging the principles of negative pressure and advanced engineering, these systems provide reliable, low-maintenance, and environmentally friendly solutions for a wide range of industrial applications. With a focus on quality and innovation, HeadPowder continues to lead the industry in developing state-of-the-art conveyor systems that meet the evolving needs of modern manufacturing and processing facilities.




