For the production of fermented grain products, efficient and reliable material handling is crucial. The air-powered conveyor, specifically designed for transporting fermented grain, plays a vital role in optimizing the workflow and ensuring consistent quality. This article provides an overview of the fermented grain air-powered conveyor, focusing on its structural design and operational principles, while highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. as a leading manufacturer in this field.
Overview of Fermented Grain Air-Powered Conveyor
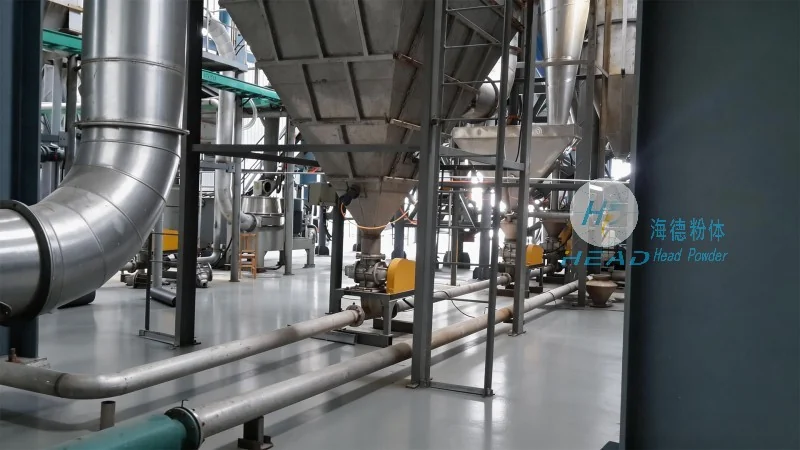
The fermented grain air-powered conveyor is a specialized piece of equipment used in the fermentation industry to transport bulk materials like fermented grain from one location to another. It operates on the principle of pneumatic conveying, utilizing compressed air to move the material through a pipeline system. This method offers several advantages over traditional mechanical conveyors, including reduced contamination risk, lower maintenance requirements, and the ability to handle materials with high moisture content or fine particles.
Structural Components of the Conveyor System
The fermented grain air-powered conveyor consists of several key components that work in tandem to ensure smooth operation. These components include the hopper, which serves as the material inlet, feeding the fermented grain into the system. The hopper is equipped with a discharge valve to control the flow rate. The pipeline system, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the acidic environment of fermented grain and maintain hygiene standards. The conveyor also features a series of bends and elbows to navigate the path, with appropriate support structures to prevent sagging or damage to the pipeline. At the discharge end, a receiver or silo collects the material, and a venting system is integrated to manage air pressure and prevent dust accumulation.
Operating Principle and Working Mechanism
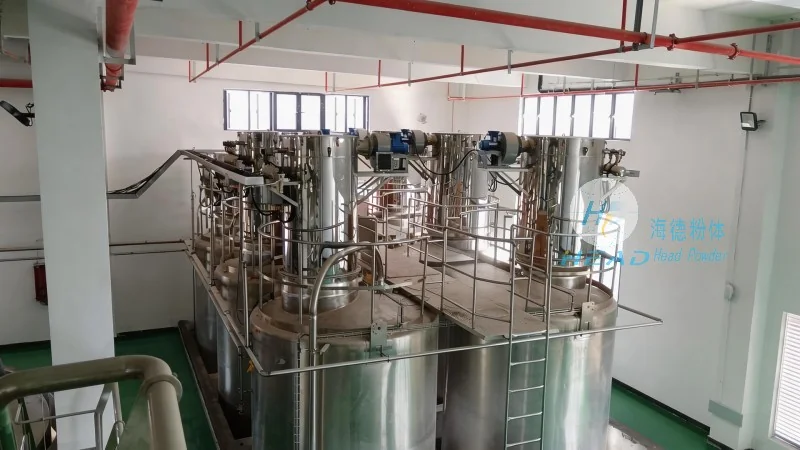
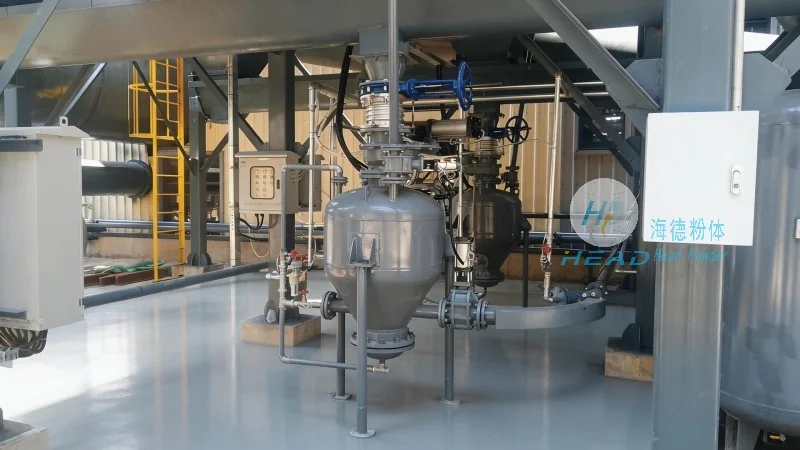
The operation of the fermented grain air-powered conveyor is based on the differential pressure created by compressed air. When the system is activated, compressed air is introduced into the pipeline, creating a low-pressure zone at the discharge end. This pressure difference causes the fermented grain to be drawn into the pipeline and transported to the receiving point. The air velocity is carefully controlled to ensure that the material is conveyed without causing excessive wear or degradation. The system may also incorporate a rotary valve or feeder at the inlet to regulate the flow of material, preventing blockages and maintaining consistent performance. The venting and filtration systems are essential for maintaining air quality and preventing the buildup of dust or particles that could affect the conveyor's efficiency or the quality of the fermented grain.
Advantages and Applications
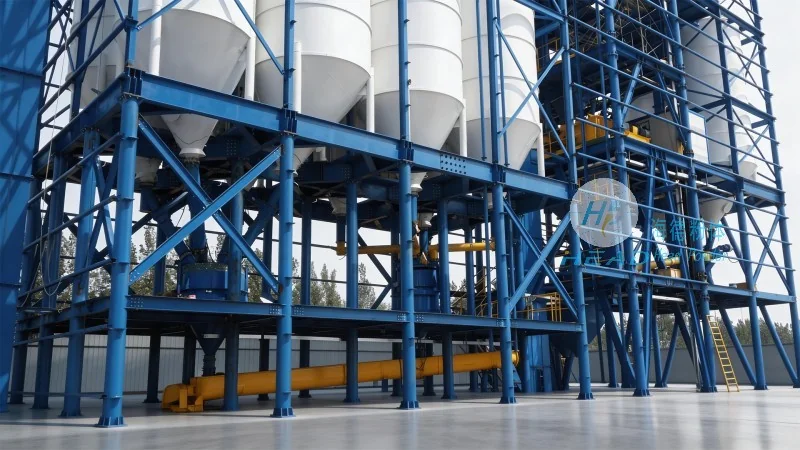
The fermented grain air-powered conveyor offers numerous benefits for industrial applications. Its hygienic design and ability to handle wet or sticky materials make it ideal for use in breweries, distilleries, and other fermentation facilities. The system's compact size and flexibility allow for easy integration into existing production lines, reducing the need for extensive modifications. Additionally, the low maintenance requirements and energy efficiency of pneumatic conveying contribute to long-term cost savings. This equipment is commonly used for transporting fermented grain from fermentation tanks to storage silos, or for moving it between different processing stages, ensuring a seamless workflow and minimizing downtime.
About Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer of specialized engineering equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in the design and production of air-powered conveyors for the fermentation industry. With years of experience and a commitment to quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder's products are engineered to meet the specific needs of the fermentation sector, with a focus on durability, hygiene, and performance. The company's headquarters is located in Shandong, China, where it maintains state-of-the-art manufacturing facilities and a dedicated team of engineers and technicians. By leveraging advanced technology and adhering to strict quality control standards, HeadPowder ensures that its air-powered conveyors deliver optimal performance and contribute to the success of its clients' operations.
Conclusion
In conclusion, the fermented grain air-powered conveyor is a critical component in modern fermentation processes, offering efficient and hygienic material handling solutions. Its structural design and operational principles are tailored to the unique requirements of fermented grain, ensuring reliable performance and consistent quality. With the expertise of manufacturers like Shandong HeadPowder Engineering Co., Ltd., businesses can access high-quality equipment that meets their specific needs and contributes to the optimization of their production workflows. The continued development and refinement of such equipment will undoubtedly play a significant role in enhancing the efficiency and sustainability of the fermentation industry.




