HeadPowder, as the professional manufacturer based in Shandong, China, specializes in the design, development, and production of advanced pneumatic conveying systems. Our company, Shandong HeadPowder Engineering Co., Ltd., is committed to providing reliable and efficient solutions for material handling in various industrial applications. The Red Bean Pneumatic Conveying System is one of our flagship products, engineered to meet the demands of modern powder and bulk material transportation.
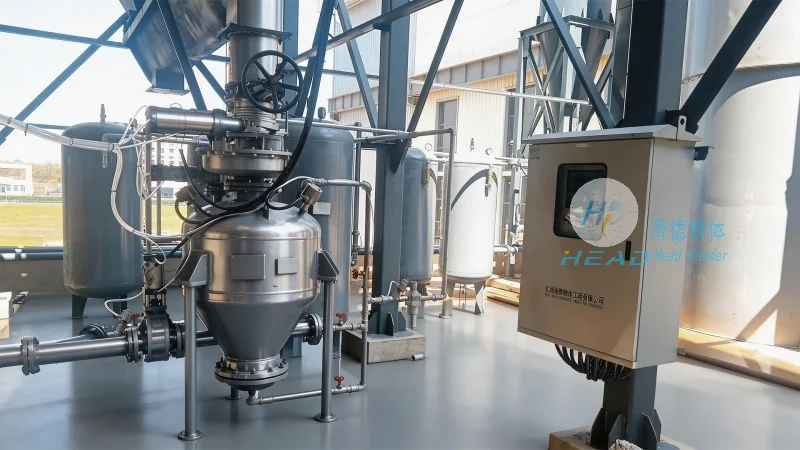
Overview of the Red Bean Pneumatic Conveying System
The Red Bean Pneumatic Conveying System is a sophisticated piece of equipment designed to transport bulk materials, such as powders and granules, through a pipeline using air or gas as the conveying medium. This system offers a flexible and efficient alternative to traditional mechanical conveying methods, which often involve complex machinery and high maintenance costs. The system's design emphasizes durability, energy efficiency, and ease of operation, making it suitable for a wide range of industrial sectors including food processing, pharmaceuticals, chemicals, and more.
Structural Components and Working Principle
The Red Bean Pneumatic Conveying System comprises several key components that work in harmony to achieve effective material transport. The main components include the feeding unit, the conveying pipeline, the separation and cleaning system, and the receiving container. The feeding unit is responsible for introducing the material into the system, typically through a hopper or a rotary valve. The conveying pipeline, often made of stainless steel or other corrosion-resistant materials, transports the material and air mixture. The separation system, which may include a cyclone separator or a bag filter, separates the material from the air, allowing the air to be recirculated or discharged while the material is collected in the receiving container.
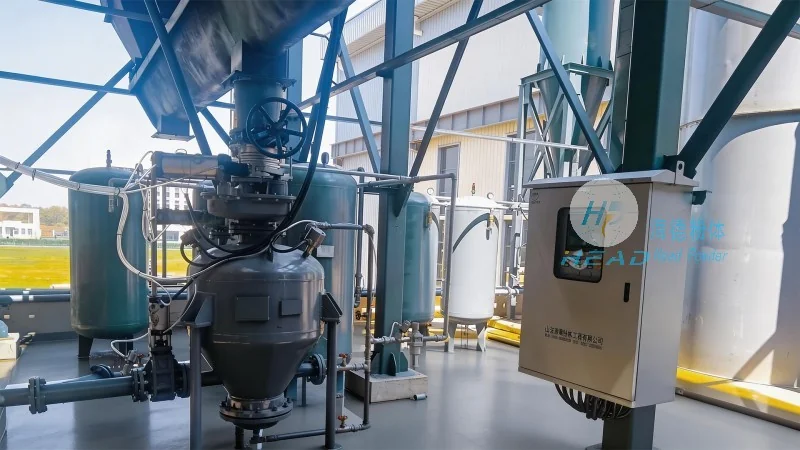
The working principle of the system is based on the principle of pneumatic transport, where the material is suspended in the air stream and carried through the pipeline. The system can operate in either positive pressure or negative pressure modes. In positive pressure mode, air is blown into the pipeline, creating a high-pressure environment that pushes the material forward. In negative pressure mode, air is drawn out of the pipeline, creating a vacuum that pulls the material along. The choice between these modes depends on the material properties, the distance to be conveyed, and the system's design. The Red Bean system is equipped with advanced control systems that allow for precise regulation of air flow, pressure, and material feed rate, ensuring optimal performance and minimizing energy consumption.
Key Features and Advantages
One of the standout features of the Red Bean Pneumatic Conveying System is its ability to handle a wide variety of materials, from fine powders to coarse granules, without causing degradation or contamination. The system's design minimizes material degradation due to its gentle handling and low shear forces. Additionally, the system is highly customizable, allowing customers to tailor the equipment to their specific needs, including the length of the pipeline, the type of separation system, and the control system. The Red Bean system also offers significant advantages in terms of space efficiency, as it can be installed in a compact footprint compared to traditional conveying systems. This makes it ideal for facilities with limited space or where a clean and hygienic environment is required.
Another key advantage is the system's energy efficiency. By utilizing air as the conveying medium, the Red Bean system reduces the need for mechanical components such as conveyors or elevators, which can be energy-intensive. The system's control systems are designed to optimize air usage, further reducing energy costs. Furthermore, the Red Bean system is designed for low maintenance, with easy access to components for cleaning and replacement. This reduces downtime and maintenance costs, ensuring high availability and reliability. The system also complies with various international standards for safety and environmental protection, providing peace of mind to users.
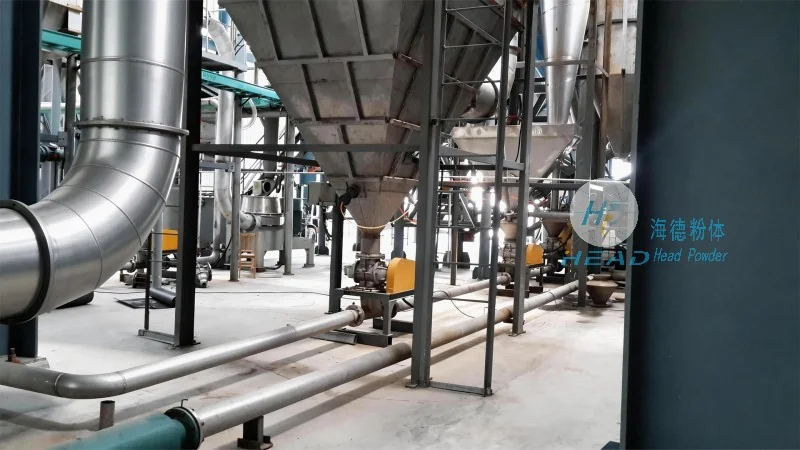
Application Scenarios and Industrial Use
The Red Bean Pneumatic Conveying System is widely used in various industrial applications where bulk materials need to be transported efficiently and safely. In the food industry, the system is commonly used to transport ingredients such as flour, sugar, and spices, ensuring that the materials remain fresh and uncontaminated. In the pharmaceutical industry, the system is used to transport active pharmaceutical ingredients (APIs) and other powders, maintaining strict hygiene and contamination control. In the chemical industry, the system is used to transport chemicals, including powders and granules, while ensuring safety and environmental compliance. The system is also used in the agricultural sector to transport grains and other agricultural products, as well as in the mining industry to transport ore and other bulk materials.
In each of these applications, the Red Bean system provides a reliable and efficient solution for material handling. Its ability to handle different materials and its flexibility in design make it a versatile choice for various industrial needs. The system's performance is consistently high, with minimal downtime and low maintenance costs, making it a cost-effective investment for businesses. By choosing the Red Bean Pneumatic Conveying System, companies can improve their operational efficiency, reduce costs, and enhance the quality of their products.




