HeadPowder, a professional manufacturer based in Shandong, China, specializes in providing advanced pneumatic conveying systems tailored for handling red bean powder and other fine particulate materials. Our products are designed to meet the unique demands of the food processing industry, ensuring efficient, hygienic, and reliable material transport. This article explores the fundamental principles behind pneumatic conveying technology and highlights the key characteristics of working environments where such systems are most effectively utilized.
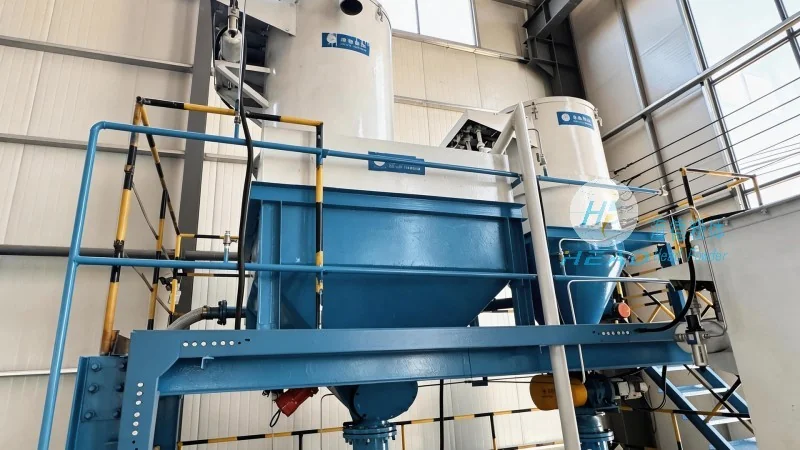
Company Profile: HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd. is a leading enterprise in the field of pneumatic conveying equipment, with its headquarters located in Shandong, China. The company has built a strong reputation for delivering high-quality, customized solutions that enhance operational efficiency in various industrial applications. By leveraging advanced engineering and manufacturing capabilities, HeadPowder ensures that its pneumatic conveying systems meet stringent industry standards, particularly in the food processing sector where product purity and safety are paramount.
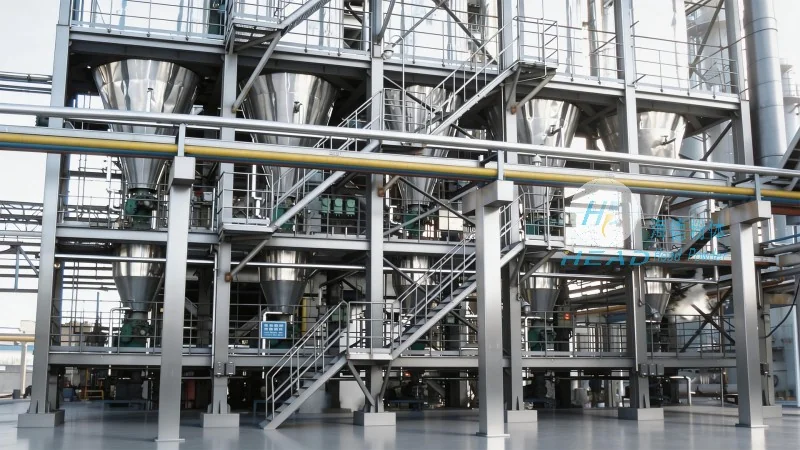
Principle of Pneumatic Conveying for Red Bean Powder Handling
Pneumatic conveying, also known as air conveying, is a method of transporting bulk materials through a pipeline using pressurized or vacuum air. For red bean powder, which typically consists of fine particles with specific flow characteristics, this technology offers several advantages over traditional mechanical conveying methods. The core principle involves generating a flow of air within the pipeline that entrains the powder particles, moving them from the source to the destination. There are two primary types of pneumatic conveying systems: pressure systems, which use positive pressure to push material through the line, and vacuum systems, which use negative pressure to pull material from the source. Both systems are engineered to handle the unique properties of red bean powder, such as its particle size distribution, moisture content, and tendency to agglomerate. The design of the conveying system, including the choice of air velocity, pipeline diameter, and the use of special components like cyclones or rotary valves, is critical to achieving optimal performance and minimizing material degradation.
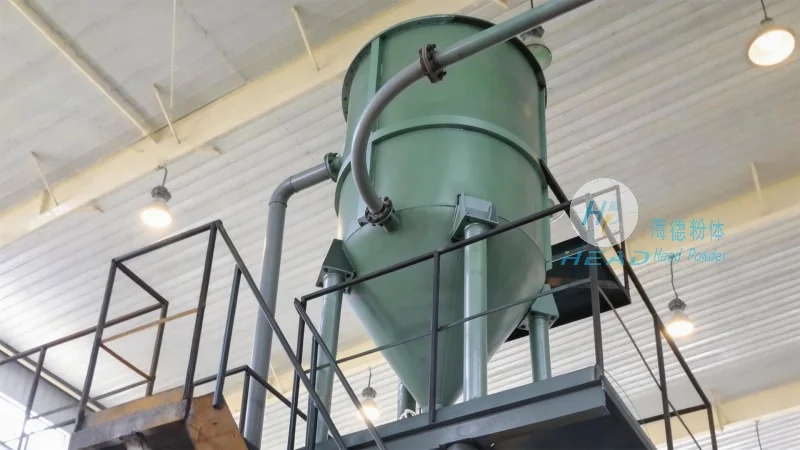
Working Scene Characteristics of Red Bean Powder Pneumatic Conveying Systems
The effectiveness of a pneumatic conveying system for red bean powder is heavily influenced by the working environment and operational conditions. Key characteristics of these working scenes include: 1. **Hygienic and Sanitary Design**: In food processing facilities, the system must comply with strict hygiene standards, featuring smooth, easy-to-clean surfaces and materials that resist contamination. 2. **Efficient Material Handling**: The system is designed to handle large volumes of red bean powder with minimal downtime, ensuring continuous production flow. 3. **Space Optimization**: Pneumatic conveying systems are often used in compact spaces where traditional belt or bucket elevators may not fit, making them ideal for modern, space-constrained processing plants. 4. **Reduced Product Loss and Contamination**: By minimizing direct contact with equipment and using enclosed pipelines, the system reduces the risk of product loss and cross-contamination, which is critical for maintaining product quality and regulatory compliance. 5. **Adaptability to Variable Production Rates**: The system can be adjusted to handle fluctuations in production volume, allowing for flexible operation during different stages of the red bean processing cycle, such as grinding, sieving, and packaging. 6. **Energy Efficiency**: Modern pneumatic conveying systems are designed to operate with lower energy consumption compared to traditional methods, contributing to cost savings and environmental sustainability. These characteristics make pneumatic conveying an ideal solution for red bean powder handling in various industrial settings, from small-scale processing facilities to large-scale food production plants.
Application Scenarios in the Red Bean Processing Industry
Red bean powder is widely used in the food industry for making beverages, desserts, and other products. The pneumatic conveying systems from HeadPowder are particularly well-suited for several key applications within the red bean processing workflow. For instance, in the initial stages of processing, red beans are ground into fine powder, and the pneumatic system efficiently transports this powder from the grinding mills to storage silos or packaging lines. During the sieving and classification process, the system can convey the separated fine and coarse particles to different storage areas, ensuring precise material management. In the packaging stage, the system delivers the final red bean powder to filling machines, maintaining consistent product quality and preventing contamination. Additionally, in the production of red bean-based beverages, the system can handle the powder in the mixing and blending stages, ensuring uniform distribution of the powder in the final product. These applications highlight the versatility and reliability of pneumatic conveying systems in supporting the entire red bean processing chain.
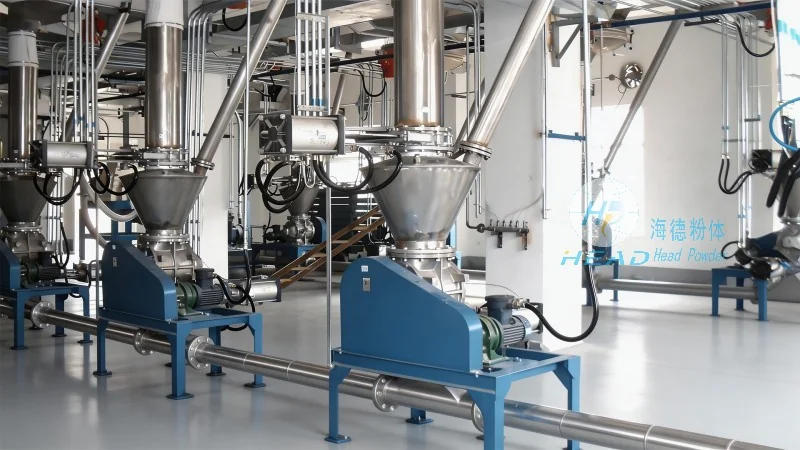
Advantages of Choosing HeadPowder's Pneumatic Conveying Solutions
When selecting a pneumatic conveying system for red bean powder handling, businesses benefit from the expertise and quality of HeadPowder Engineering Co., Ltd. The company’s solutions offer several key advantages: 1. **Customized Design**: Each system is tailored to the specific requirements of the client, including the type and quantity of red bean powder, production capacity, and facility layout. 2. **High Efficiency and Reliability**: The systems are engineered to operate with minimal maintenance and downtime, ensuring consistent performance over long periods. 3. **Hygienic Compliance**: All components are designed to meet food industry standards, such as FDA and EU regulations, ensuring product safety and regulatory compliance. 4. **Energy Efficiency**: Advanced control systems and optimized air flow reduce energy consumption, leading to lower operational costs. 5. **Long-Term Support**: HeadPowder provides comprehensive after-sales support, including maintenance, spare parts, and technical assistance, ensuring the system remains in optimal condition throughout its lifespan. By choosing HeadPowder's pneumatic conveying solutions, companies can enhance their operational efficiency, improve product quality, and meet the demands of a competitive market.




