

Working Principle and Features of Tonne Bag Dust-Free Feeding Station Pneumatic Conveying Line
The tonne bag dust-free feeding station with pneumatic conveying line is a specialized industrial system designed to handle bulk materials from tonne bags in a clean and efficient manner. This system is widely used in industries such as chemical, food, pharmaceutical, and construction, where maintaining a dust-free environment is crucial for product quality and worker safety. The system integrates several key components, including a dust-free feeding station, a pneumatic conveying system, and control mechanisms, to ensure seamless material transfer from the bag to the processing equipment.
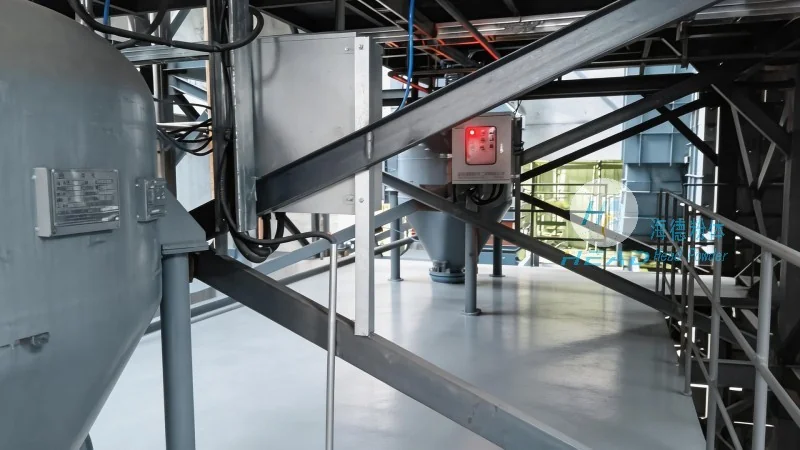
Working Principle of the Tonne Bag Dust-Free Feeding Station
The operation of the tonne bag dust-free feeding station begins with the placement of a tonne bag (typically 1 tonne or 1000 kg) onto the feeding platform. The bag is then secured using a clamping mechanism to prevent any movement during the feeding process. A rotary valve or a bag opening device is used to release the material from the bag into the hopper. The material is then transferred to the pneumatic conveying system through a hopper and a feeding valve. The pneumatic conveying system uses compressed air or other gases to transport the material through a pipeline to the destination point, such as a silo, mixer, or processing machine. The system is equipped with a dust collection system to capture any airborne particles, ensuring that the environment remains clean and safe. The control system monitors the flow rate, pressure, and other parameters to maintain optimal operation and prevent any blockages or overflows.
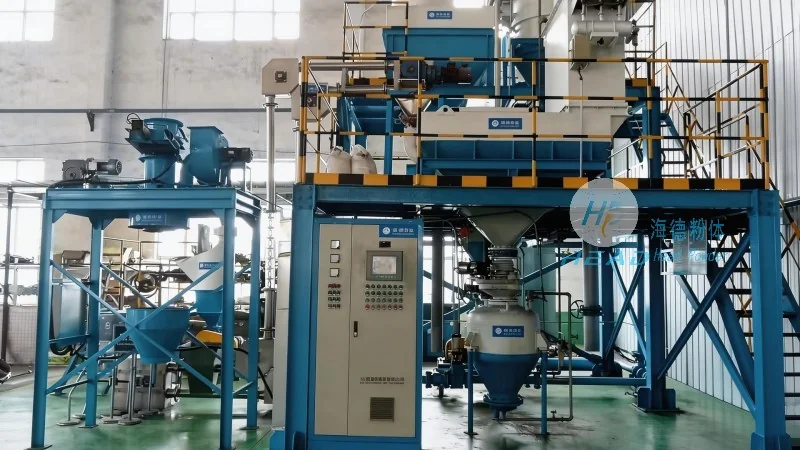
Key Features of the Tonne Bag Dust-Free Feeding Station
One of the primary features of this system is its dust-free operation. The feeding station is enclosed in a sealed housing, which prevents dust from escaping into the surrounding environment. The system uses a combination of filtration and ventilation to maintain a clean air quality inside the enclosure. Another important feature is the ability to handle a wide range of bulk materials, including powders, granules, and pellets. The system is designed to accommodate different bag sizes and types, making it versatile for various applications. The pneumatic conveying system is also capable of handling long distances and multiple transfer points, allowing for flexible material distribution. Additionally, the system is equipped with safety features, such as emergency stop buttons and overload protection, to ensure safe operation. The control system provides real-time monitoring and data logging, enabling operators to track the system's performance and identify any issues promptly.
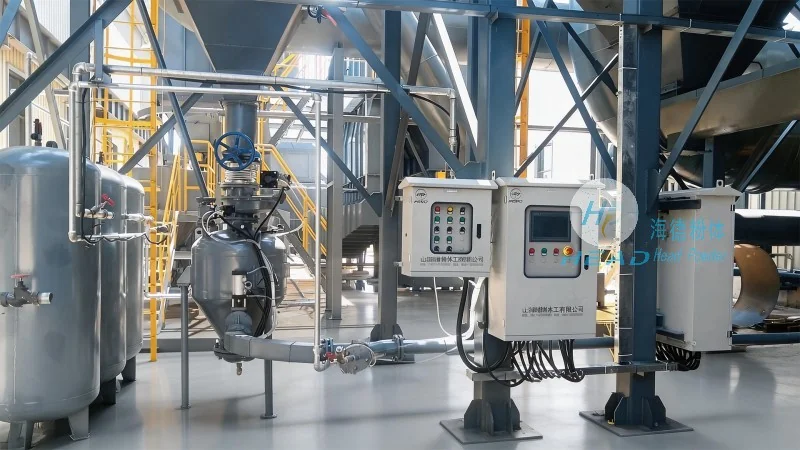
Benefits of Using the Tonne Bag Dust-Free Feeding Station
The use of a tonne bag dust-free feeding station with pneumatic conveying line offers several benefits to industrial operations. Firstly, it improves product quality by preventing contamination from dust and other particles. This is particularly important for products that are sensitive to moisture or impurities, such as food and pharmaceuticals. Secondly, it enhances worker safety by reducing exposure to dust and other hazardous materials. The sealed design of the system minimizes the risk of respiratory diseases and other health issues. Thirdly, it increases operational efficiency by automating the material handling process. The system can handle large quantities of material quickly and consistently, reducing the need for manual labor and minimizing downtime. Finally, it reduces maintenance costs by using durable components and a well-designed system that minimizes wear and tear.
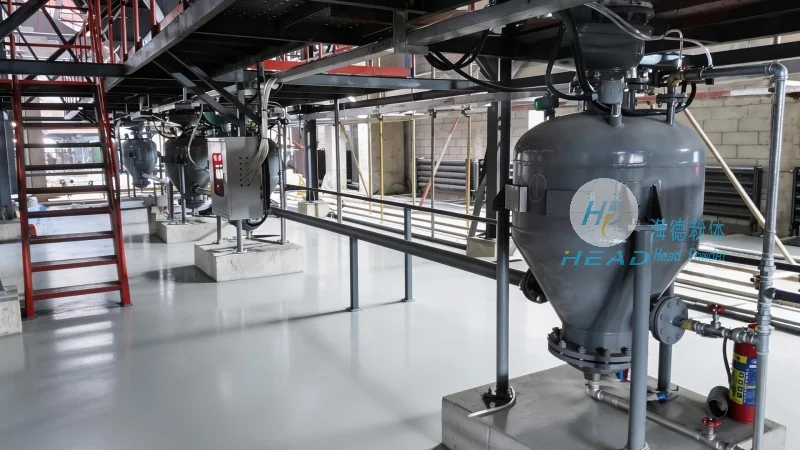
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial material handling equipment. The company specializes in the design, manufacturing, and installation of dust-free feeding stations, pneumatic conveying systems, and other related equipment. With years of experience in the industry, HeadPowder has developed a reputation for producing high-quality, reliable, and efficient systems that meet the needs of various industries. The company's products are known for their durability, ease of maintenance, and user-friendly operation. HeadPowder's team of engineers and technicians work closely with customers to understand their specific requirements and provide customized solutions that meet their needs. The company is committed to providing excellent customer service and support, ensuring that customers get the best possible solution for their material handling needs.