Principles and Application Scenarios of Pharmaceutical Material Handling Equipment
Release time:2026-09-19 11:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Pharmaceutical material handling equipment is a critical component in modern pharmaceutical manufacturing facilities. These systems are designed to efficiently transport raw materials, intermediate products, and finished goods throughout the production process, ensuring compliance with stringent regulatory standards such as Good Manufacturing Practice (GMP). The equipment not only enhances operational efficiency but also maintains product integrity and safety throughout the handling and transportation stages.
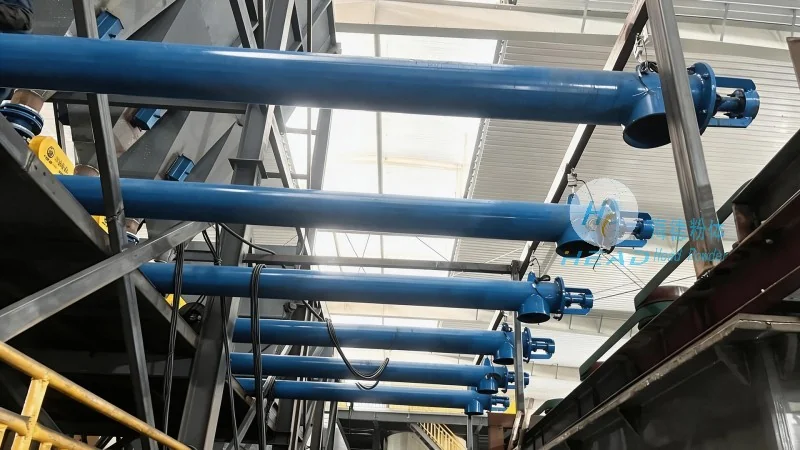
Core Principles of Material Handling Systems
The fundamental principles of pharmaceutical material handling equipment revolve around precision, reliability, and hygiene. These systems are engineered to minimize product contamination, prevent cross-contamination, and ensure consistent handling of sensitive pharmaceutical materials. Key principles include:
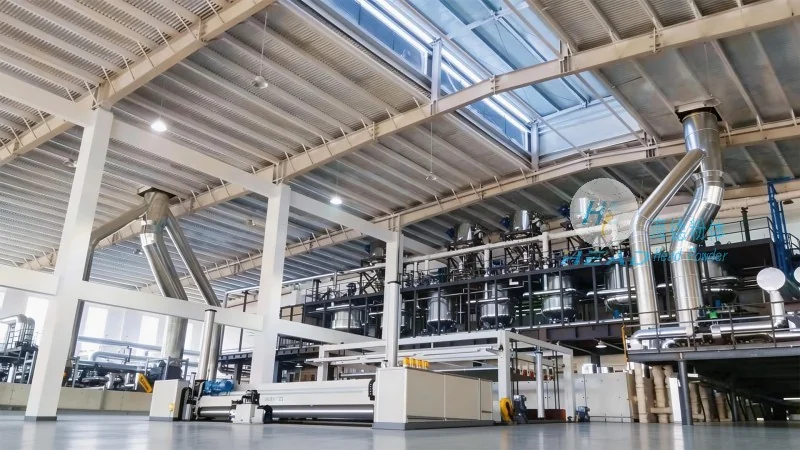
- Hygienic Design: Equipment is constructed with smooth, non-porous surfaces that are easy to clean and sanitize, reducing the risk of microbial growth.
- Modular and Flexible Layouts: Systems are often modular, allowing for easy reconfiguration to accommodate different production batches or product lines.
- Integrated Control Systems: Advanced control systems enable real-time monitoring and adjustment of the handling process, ensuring optimal performance and compliance with production parameters.
Common Application Scenarios in Pharmaceutical Manufacturing
Pharmaceutical material handling equipment is utilized in various critical stages of drug production, each tailored to specific operational needs. The following are common application scenarios:
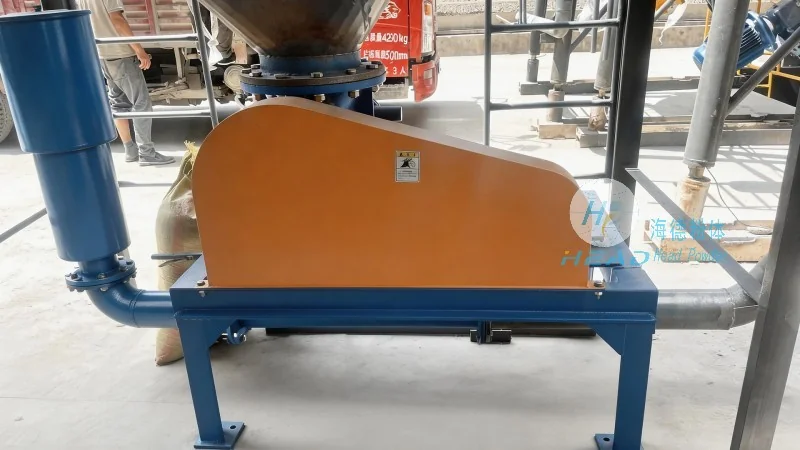
- Raw Material Handling: Systems transport raw ingredients from storage to production lines, ensuring accurate dosing and minimal waste. This stage often involves bulk handling and precise measurement to maintain product consistency.
- Intermediate Product Transport: After initial processing, intermediate products are moved between processing units, such as from mixing to filtration or packaging. This phase requires systems that can handle viscous or semi-solid materials while maintaining sterility.
- Finished Product Packaging: The final stage involves transporting finished pharmaceutical products to packaging lines, where they are sealed, labeled, and prepared for distribution. This step emphasizes speed and accuracy to meet market demands.
Key Features and Advantages of HeadPowder's Solutions
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced pharmaceutical material handling solutions that address the unique challenges of the pharmaceutical industry. Our equipment is designed with the following key features:
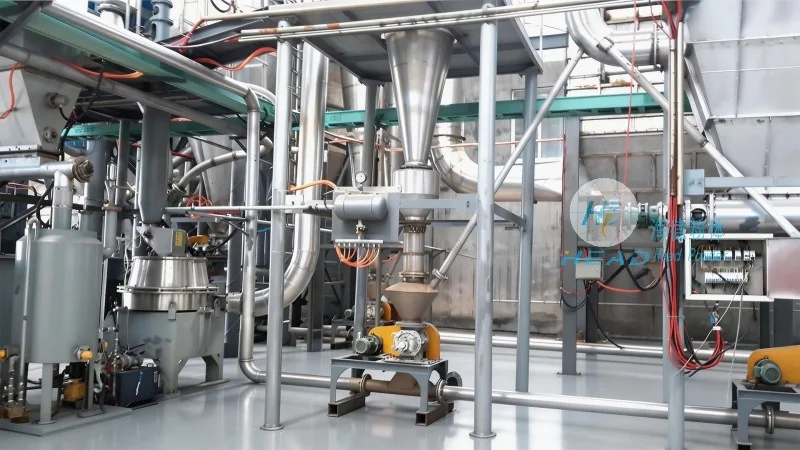
- Customizable Solutions: We offer tailored systems that align with specific production requirements, ensuring optimal performance and cost-effectiveness.
- Robust Construction: Equipment is built with high-quality materials that withstand the demands of continuous operation in a GMP-compliant environment.
- Advanced Automation: Integration of automation technologies enhances operational efficiency, reduces human error, and improves overall productivity.
- Comprehensive Support: From design and installation to maintenance and training, we provide end-to-end support to ensure long-term reliability and performance.
Ensuring Compliance and Efficiency in Pharmaceutical Handling
In the pharmaceutical industry, compliance with regulatory standards is non-negotiable. Our material handling equipment is engineered to meet or exceed GMP requirements, ensuring that every aspect of the handling process is controlled and monitored. By leveraging advanced technology and meticulous design, we help pharmaceutical manufacturers achieve higher levels of efficiency while maintaining the highest standards of product quality and safety.




