Classification and Composition of Coal and Coke Pneumatic Conveying Systems
Release time:2026-09-14 10:38:47
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Coal and coke are essential raw materials in various industrial processes, and efficient transportation of these materials is crucial for maintaining smooth operations. Pneumatic conveying systems offer a reliable and effective method for moving coal and coke from one location to another within industrial facilities. This article provides an overview of the classification and key components of coal and coke pneumatic conveying systems, highlighting the importance of each component in ensuring optimal performance and safety.
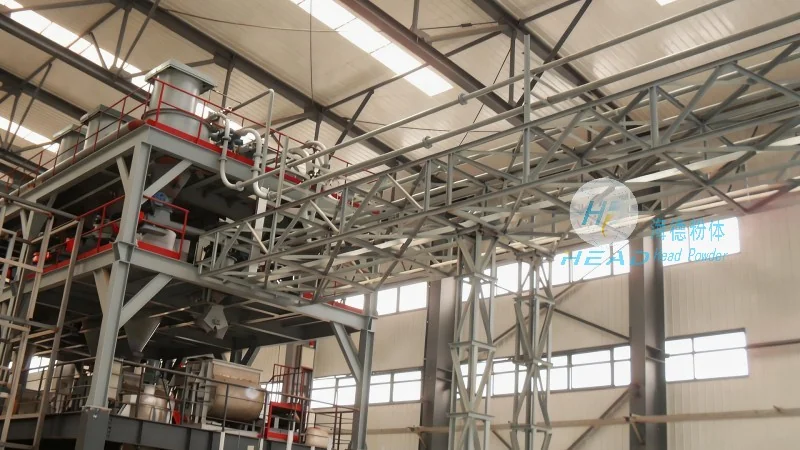
Classification of Pneumatic Conveying Systems
Pneumatic conveying systems for coal and coke can be classified based on several factors, including the type of material being conveyed, the operating pressure, and the system design. The primary classifications include pressure and vacuum systems. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems use a vacuum to draw the material into the system. Additionally, systems can be categorized as dilute-phase or dense-phase, depending on the material's flow characteristics and the desired conveying velocity.
Key Components of Coal and Coke Pneumatic Conveying Systems
The effectiveness of a coal and coke pneumatic conveying system depends on the proper integration of several key components. These components work together to ensure the material is conveyed safely and efficiently. The main components include:
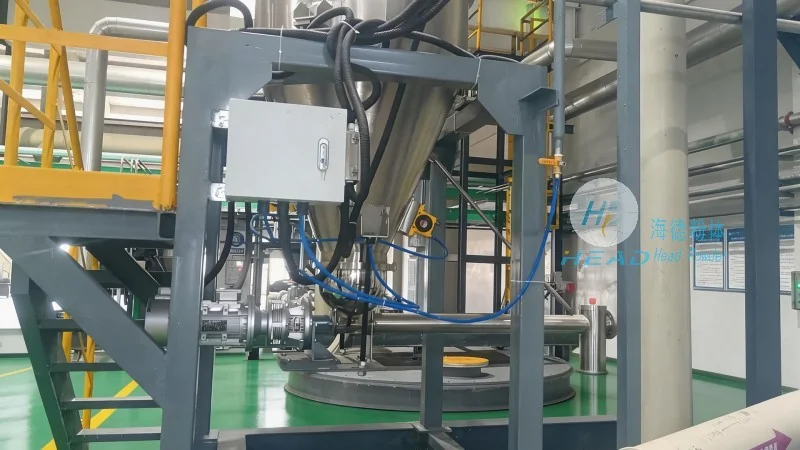
- Feeding Equipment: This component is responsible for introducing the coal or coke into the conveying system. It may include hoppers, feeders, or rotary valves that control the flow rate and ensure a consistent feed.
- Conveying Pipeline: The pipeline is the main channel through which the material is transported. It is typically made of materials such as stainless steel or plastic, depending on the material's corrosiveness and the system's operating conditions. The pipeline design, including its diameter and length, is critical for maintaining the desired conveying velocity and preventing material buildup or blockages.
- Air Supply System: This system provides the necessary air pressure or vacuum to move the material through the pipeline. It includes compressors, vacuum pumps, air filters, and regulators to ensure the air quality and pressure are suitable for the conveying process.
- Separation and Collection Equipment: At the receiving end of the system, this component separates the material from the air and collects it in a designated container. It may include cyclones, filters, or dust collectors to prevent material loss and maintain air quality.
- Control and Monitoring Systems: These systems monitor the operation of the conveying process and adjust parameters as needed to maintain optimal performance. They may include sensors, controllers, and alarms to detect issues such as blockages, pressure drops, or air leaks.
Role of Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of coal and coke pneumatic conveying systems. With years of experience in the industry, the company has developed a comprehensive understanding of the unique challenges associated with conveying coal and coke, including material variability, abrasive properties, and the need for high reliability. headpowder's team of engineers and technicians work closely with clients to understand their specific requirements and provide customized solutions that meet their operational needs and budget constraints.
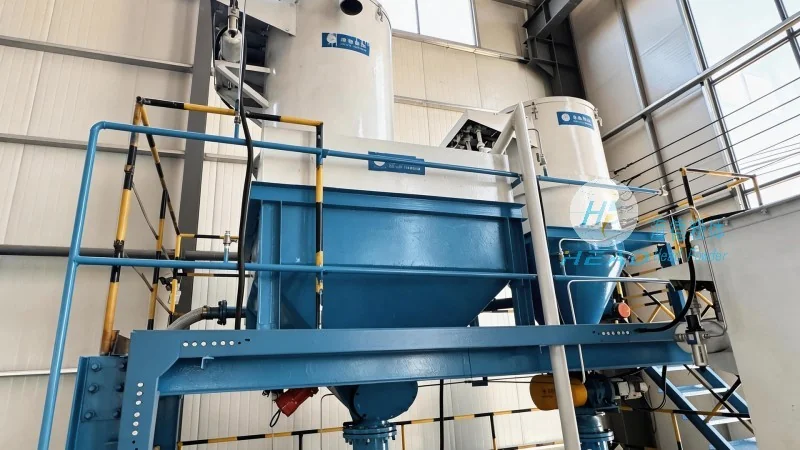
Benefits of Using Coal and Coke Pneumatic Conveying Systems
Implementing a pneumatic conveying system for coal and coke offers several advantages over traditional methods such as belt conveyors or bucket elevators. These benefits include:
- Reduced Labor Costs: Automated systems minimize the need for manual handling, reducing labor costs and improving safety.
- Improved Safety: Pneumatic conveying systems eliminate the need for workers to handle heavy or hazardous materials, reducing the risk of accidents and injuries.
- Increased Efficiency: The continuous operation of pneumatic systems allows for higher throughput and reduced downtime compared to traditional methods.
- Space Efficiency: Pneumatic systems can be installed in tight spaces, making them suitable for facilities with limited floor space.
- Environmental Benefits: Properly designed systems can minimize dust emissions and improve air quality, contributing to a safer and more sustainable industrial environment.
Conclusion
Coal and coke pneumatic conveying systems are a critical component of modern industrial operations, providing efficient and safe transportation of these essential raw materials. The classification and key components of these systems are essential for understanding their functionality and ensuring optimal performance. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., clients can benefit from customized solutions that meet their specific needs and enhance their operational efficiency. By investing in a well-designed pneumatic conveying system, industrial facilities can improve productivity, reduce costs, and maintain a safe working environment.




