For industries dealing with rice husk processing, the challenge of moving bulk powders efficiently and reliably is a critical concern. Traditional methods like manual handling or mechanical conveyors often fall short in terms of speed, hygiene, and operational flexibility. This is where pneumatic conveying systems step in, offering a modern solution that leverages air flow to transport materials with precision and efficiency. The core principle of pneumatic conveying involves using compressed air or gas to move dry, free-flowing materials such as rice husk through a pipeline network. By creating a pressure differential, these systems can transport materials over long distances, even vertically, with minimal maintenance and reduced risk of contamination. This approach not only enhances productivity but also ensures a cleaner and safer working environment, which is particularly important in food processing and agricultural applications.
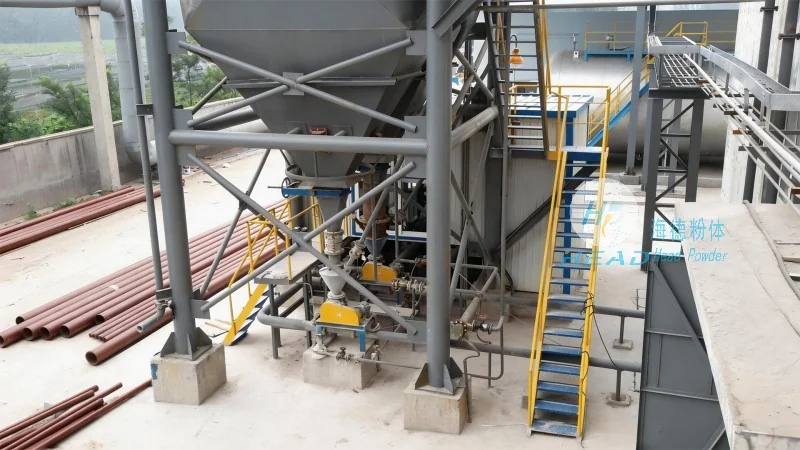
Pneumatic Conveying Solutions from HeadPowder
HeadPowder, a leading provider of engineering solutions for bulk material handling, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of rice husk processing facilities. With years of experience in the industry, the company understands that each rice husk handling operation has distinct requirements, whether it's for drying, storage, or further processing. HeadPowder's expertise lies in integrating advanced technology with practical design to deliver systems that are both efficient and cost-effective. The company's team of engineers works closely with clients to assess their specific processes, material characteristics, and operational goals, ensuring that the final solution meets all technical and regulatory standards. By focusing on tailored solutions, HeadPowder helps clients optimize their rice husk handling operations, reducing downtime and improving overall productivity.
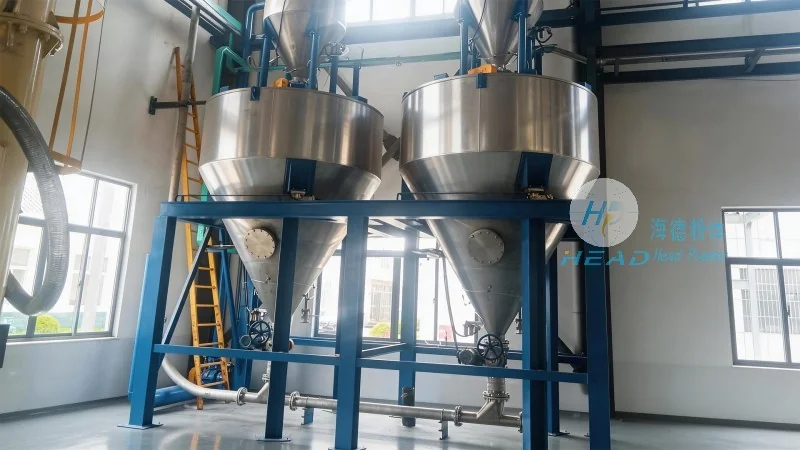
Key Features of HeadPowder's Pneumatic Conveying Systems
HeadPowder's pneumatic conveying systems for rice husk are equipped with several key features that set them apart in the market. First, the systems are designed with high-efficiency air compressors that ensure consistent and reliable air flow, even under varying load conditions. This ensures that the conveying process remains smooth and uninterrupted, minimizing the risk of material blockages or system failures. Second, the use of flexible hoses and rigid pipelines allows for versatile installation, accommodating both horizontal and vertical transport requirements. This flexibility is crucial for rice husk processing plants, where materials may need to be moved from storage silos to processing units or from one processing stage to another. Third, the systems incorporate advanced control mechanisms that allow for real-time monitoring and adjustment of the conveying parameters. This feature enables operators to optimize the system's performance based on the current material flow rate and other operational factors, further enhancing efficiency. Additionally, the materials used in the construction of the conveying components are chosen for their durability and resistance to corrosion, ensuring long-term reliability and minimal maintenance costs.
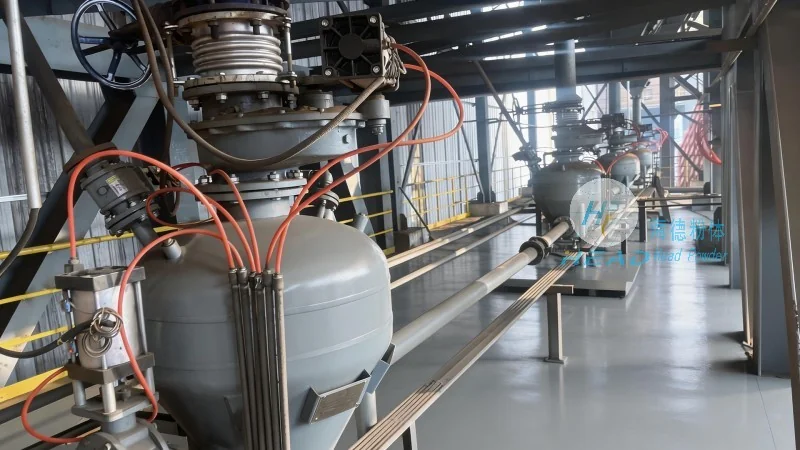
Benefits of Implementing Pneumatic Conveying for Rice Husk
Adopting pneumatic conveying systems for rice husk handling offers numerous benefits that extend beyond mere material transport. One of the most significant advantages is the improvement in operational efficiency. By automating the movement of bulk materials, the system reduces the need for manual labor, thereby lowering labor costs and minimizing the risk of human error. This automation also allows for consistent and repeatable material flow, which is essential for maintaining quality control in rice husk processing. Another key benefit is the enhanced hygiene and cleanliness of the process. Unlike mechanical conveyors that may come into direct contact with the material, pneumatic systems keep the material enclosed within the pipeline, preventing contamination from external sources. This is particularly important in food and agricultural industries where product purity is paramount. Furthermore, the systems contribute to a safer working environment by reducing the need for workers to handle heavy or dusty materials manually. By minimizing exposure to dust and reducing physical labor, the risk of workplace injuries is significantly lowered. Finally, the energy efficiency of pneumatic conveying systems makes them a cost-effective choice in the long run. While the initial investment may be higher than traditional methods, the reduced energy consumption and lower maintenance costs over time result in substantial savings for the business.
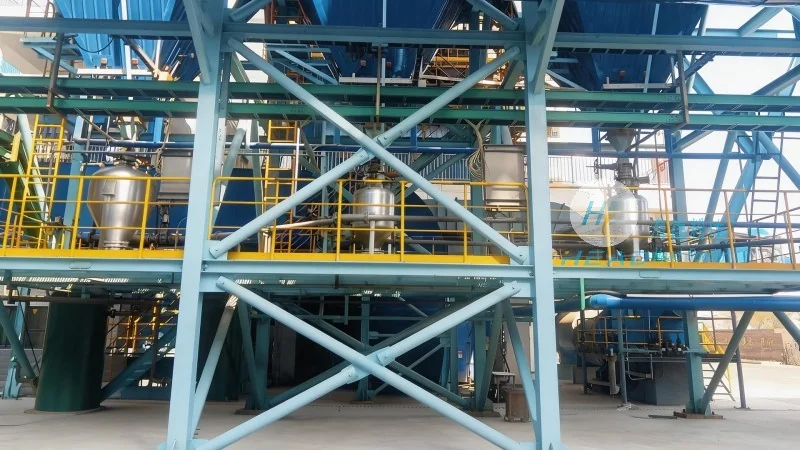
Customization and After-Sales Support from HeadPowder
HeadPowder understands that every rice husk processing facility has unique operational needs, and therefore, the company offers comprehensive customization options for its pneumatic conveying systems. Whether the client requires a simple, low-capacity system for small-scale operations or a high-capacity system for large industrial plants, HeadPowder can design a solution that meets the exact specifications. The company's engineers work closely with clients to analyze their process flow, material characteristics, and space constraints, ensuring that the final system is optimized for performance and space utilization. After the system is installed, HeadPowder provides comprehensive after-sales support to ensure the long-term reliability and efficiency of the equipment. This includes regular maintenance services, technical support, and spare parts availability. The company's commitment to customer satisfaction is reflected in its comprehensive service packages, which are designed to minimize downtime and maximize the system's operational life. By providing both pre and post-sales support, HeadPowder ensures that clients can rely on their pneumatic conveying systems for years to come, delivering consistent performance and value.




