For agricultural processing facilities, efficient and reliable material handling is crucial, especially when dealing with bulk materials like cotton seeds. The cotton seed pneumatic conveying system offers a sophisticated solution that combines technology and engineering to ensure seamless operation. This system is designed to transport cotton seeds from storage to processing units with minimal human intervention and maximum efficiency.
Understanding the Cotton Seed Pneumatic Conveying System
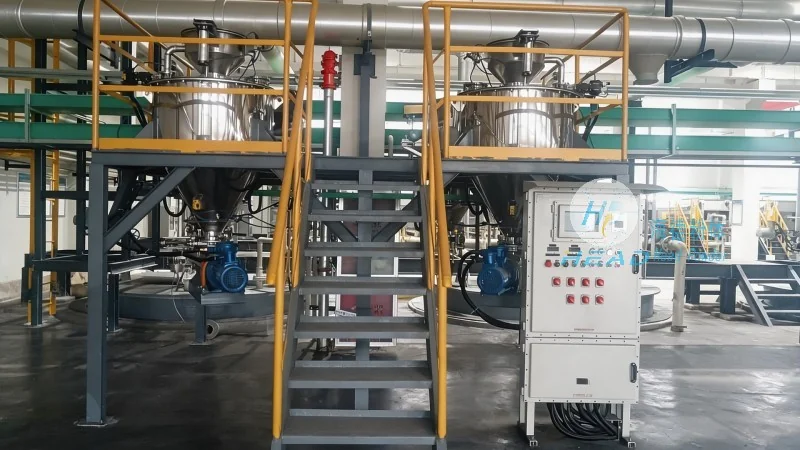
The cotton seed pneumatic conveying system utilizes air pressure to move cotton seeds through a network of pipes and components. Unlike traditional mechanical conveyors, this system relies on the force of compressed air to propel the material, reducing wear and tear on equipment and minimizing the risk of contamination. The system typically includes a hopper for material storage, a rotary valve for controlled discharge, a filter system to capture dust and particles, and a receiver where the material is deposited. Each component is carefully engineered to work in harmony, ensuring consistent performance and optimal material flow.
Key Components and Their Functions
At the heart of the cotton seed pneumatic conveying system are several critical components that work together to achieve efficient material transport. The hopper serves as the primary storage vessel, holding the cotton seeds in a controlled environment. The rotary valve, often called a star valve, regulates the flow of seeds from the hopper to the conveying line, preventing backflow and ensuring a steady supply. The filter system is essential for maintaining air quality and protecting downstream equipment from dust and debris. The receiver, typically a large tank or bin, collects the cotton seeds after they have been conveyed through the system. Additionally, the system may include a pressure regulator to control air pressure and a vacuum pump for suction applications, depending on the specific operational requirements.
Advantages of the Cotton Seed Pneumatic Conveying System
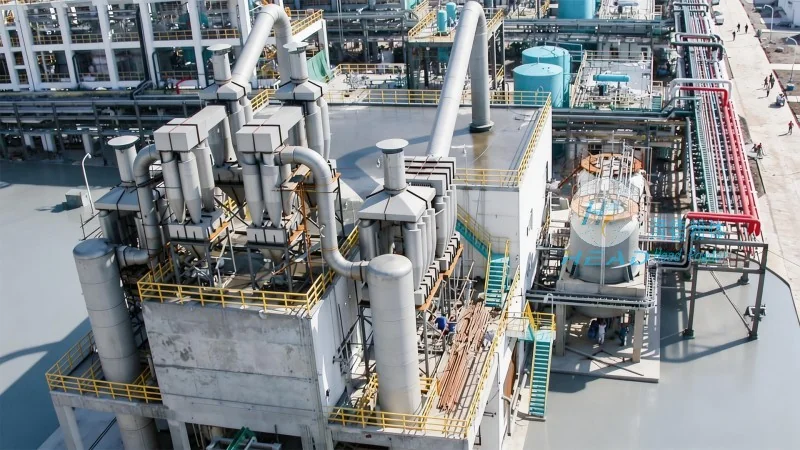
Implementing a cotton seed pneumatic conveying system offers numerous advantages for agricultural processing operations. One of the most significant benefits is the reduction in labor costs, as the system automates the material handling process, minimizing the need for manual labor. Additionally, the system reduces the risk of product damage and contamination, as the enclosed pipeline system prevents exposure to external elements and contaminants. The system also offers flexibility in terms of layout, as the pipes can be installed in various configurations to accommodate different facility designs. Furthermore, the system is energy-efficient, as it uses compressed air efficiently and can be integrated with other processing equipment to streamline operations. The low maintenance requirements of the system also contribute to long-term cost savings, as fewer mechanical parts are involved compared to traditional conveyors.
About Shandong HeadPowder Engineering Co., Ltd.
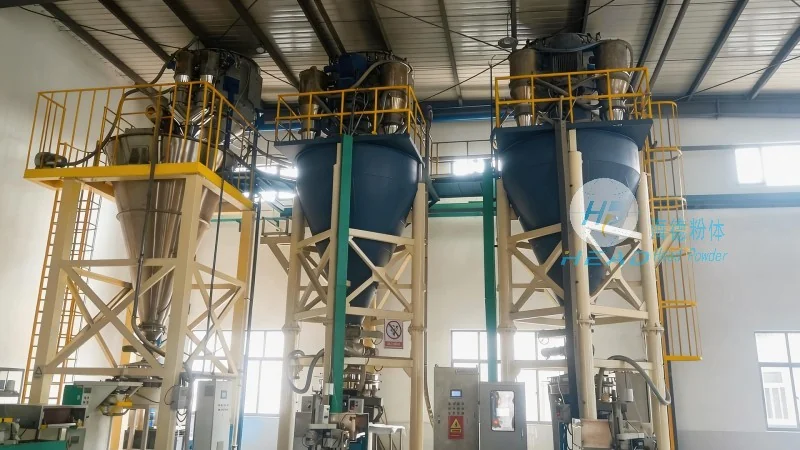
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of pneumatic conveying systems for agricultural and industrial applications. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable material handling solutions. HeadPowder's team of engineers and technicians specializes in designing and manufacturing customized systems that meet the specific needs of each client. The company's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, training, and maintenance services. HeadPowder's systems are built to withstand the rigors of industrial use, ensuring long-term performance and durability. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and quality control measures.
Conclusion
The cotton seed pneumatic conveying system is a vital component of modern agricultural processing, offering efficiency, reliability, and cost-effectiveness. By leveraging the power of compressed air, this system provides a seamless solution for transporting cotton seeds from storage to processing units. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement high-quality pneumatic conveying systems that meet their operational needs and contribute to overall productivity. The system's advantages, including reduced labor costs, minimized contamination risk, and flexible design, make it an ideal choice for agricultural facilities seeking to optimize their material handling processes.




