Phosphate calcium is a critical raw material in various industrial applications, and efficient handling and transportation of this material is essential for maintaining production efficiency and safety. The phosphate calcium pneumatic conveying system is a specialized solution designed to address these needs by utilizing air as the conveying medium to transport phosphate calcium powder or granules from one location to another.
System Overview
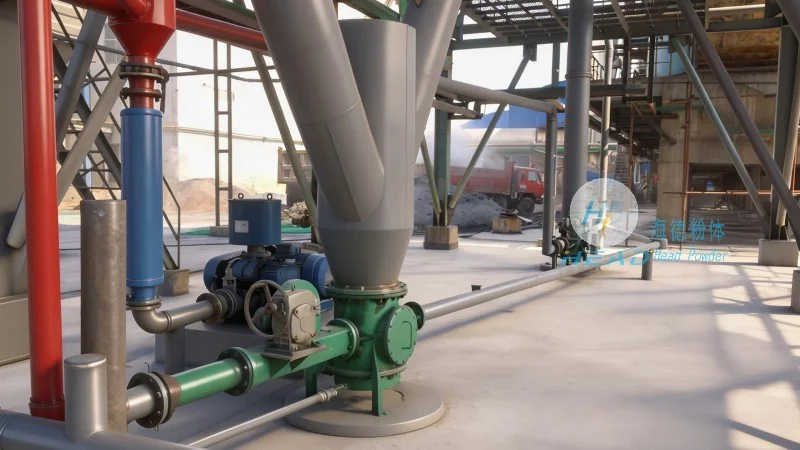
The phosphate calcium pneumatic conveying system operates on the principle of air pressure to move material through a pipeline network. It typically consists of a material feed hopper, a rotary valve or feeder, a conveying pipeline, a dust collector or filter system, and a discharge outlet. The system is engineered to handle the unique properties of phosphate calcium, such as its particle size, moisture content, and potential for dust generation, ensuring reliable and safe operation.
Key Technical Features
One of the primary advantages of the phosphate calcium pneumatic conveying system is its ability to transport material over long distances without the need for mechanical components like belts or chains. This reduces maintenance requirements and operational costs. The system can be configured as either a positive pressure or negative pressure system, depending on the specific application and material characteristics. Positive pressure systems use compressed air to push material through the pipeline, while negative pressure systems use vacuum to pull material. The choice of system type depends on factors such as the distance to be covered, the amount of material to be conveyed, and the need to minimize dust emissions.
Application Scenarios
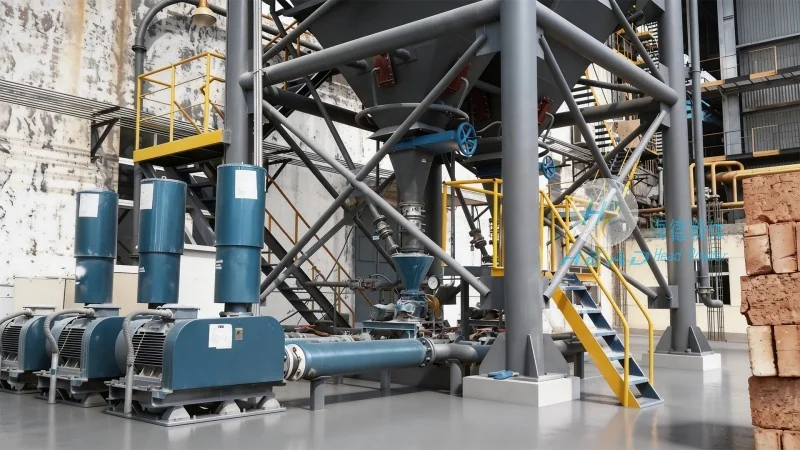
Phosphate calcium pneumatic conveying systems are widely used in industries that process or use phosphate calcium, including fertilizer manufacturing, food processing, and chemical production. In fertilizer plants, these systems are used to transport phosphate calcium from storage silos to processing units or to other parts of the facility. In food processing, they help in moving phosphate calcium used as an additive in various food products. The systems are also employed in chemical plants where phosphate calcium is used as a raw material for the production of other chemicals. The flexibility of the system allows it to be adapted to different production line configurations and material flow requirements.
Advantages of the System
Compared to traditional mechanical conveying methods, the phosphate calcium pneumatic conveying system offers several benefits. It provides a dust-free environment, which enhances workplace safety and reduces the risk of material contamination. The system is also more energy-efficient, as it uses less power to transport material compared to other methods. Additionally, it can handle materials with high moisture content or sticky properties without clogging, thanks to the air flow that keeps the material in suspension. The system's modular design allows for easy expansion or modification as production needs change, making it a cost-effective solution for long-term use.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the company behind the development and manufacturing of phosphate calcium pneumatic conveying systems, is a leading provider of engineering solutions for material handling in the chemical and food industries. With a focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking reliable and efficient conveying systems. The company's headquarters is located in Shandong, China, where it leverages advanced technology and skilled engineering expertise to design and produce high-quality pneumatic conveying systems tailored to the specific needs of its clients.
Customization and Support
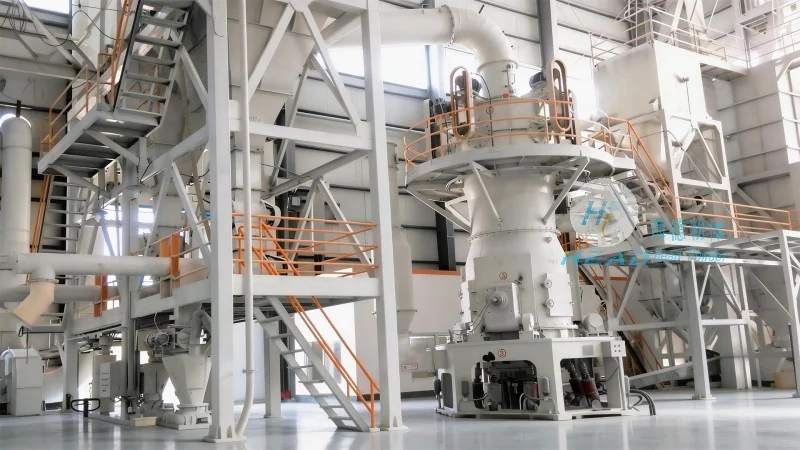
HeadPowder understands that each industrial application has unique requirements, and therefore, the company offers customized solutions for its pneumatic conveying systems. This includes designing systems with specific pipeline lengths, material feed rates, and control systems to match the client's production processes. The company also provides comprehensive after-sales support, including installation, commissioning, and maintenance services. By working closely with clients, HeadPowder ensures that the conveying systems are optimized for performance and longevity, minimizing downtime and maximizing productivity.
Conclusion
The phosphate calcium pneumatic conveying system is a sophisticated and efficient solution for handling phosphate calcium in industrial settings. By leveraging air pressure to transport material, it offers advantages such as dust control, energy efficiency, and adaptability to various material properties. With the expertise and support of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement reliable pneumatic conveying systems that enhance their operational efficiency and safety. As the demand for efficient material handling continues to grow, the phosphate calcium pneumatic conveying system remains a vital component in modern industrial operations.




