For manufacturers in the chocolate industry, efficient material handling is crucial to maintaining production efficiency and product quality. A chocolate material pneumatic conveying system offers a reliable solution for transporting cocoa powders, chocolate masses, and other related ingredients with precision and minimal contamination. This article explores the operation process and working principles of such a system, highlighting its key components and the benefits it provides to chocolate production lines.
Understanding the Core Components of a Pneumatic Conveying System
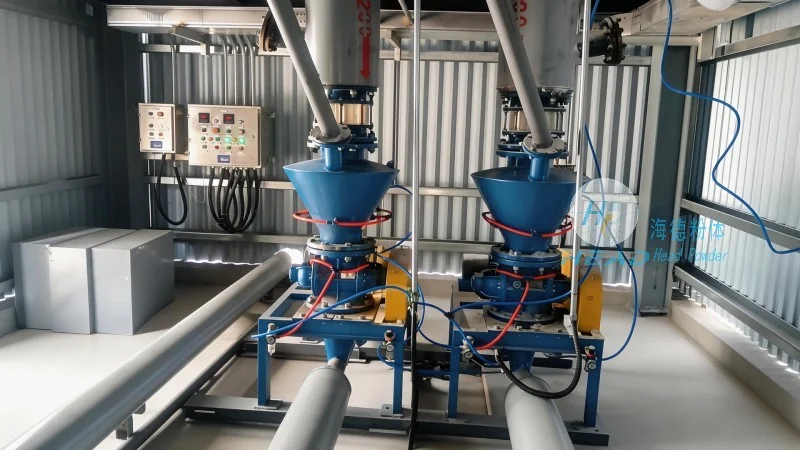
A chocolate material pneumatic conveying system typically consists of several essential components that work in tandem to move materials through the system. The primary elements include a hopper or storage silo for holding the chocolate ingredients, a conveyor line with appropriate tubing or pipes, a blower or air compressor to generate the necessary air pressure, and a series of valves and controls to regulate the flow. In addition, the system may feature filters, cyclones, or separation units to ensure that the conveyed material remains clean and free from contaminants. The design of these components is tailored to handle the specific characteristics of chocolate materials, such as their fine particle size and potential for caking or agglomeration.
The Working Principle: How Pneumatic Conveying Transports Chocolate Materials
The fundamental principle behind a pneumatic conveying system is the use of air pressure to move materials through a closed pipeline. In a positive displacement system, a blower or compressor creates a high-pressure air stream that propels the chocolate particles forward. The material is introduced into the system at a controlled rate, often via a feeder or screw, and is then entrained by the moving air. As the air and material travel through the pipeline, the system maintains a consistent flow rate, ensuring that the material is transported without excessive pressure drops or blockages. The system may use different types of conveying methods, such as dilute phase or dense phase, depending on the material properties and the required transport distance. For chocolate materials, a dilute phase system is commonly used, as it allows for efficient transport while minimizing the risk of material degradation or clogging.
The Operation Process: Step-by-Step Execution of the System
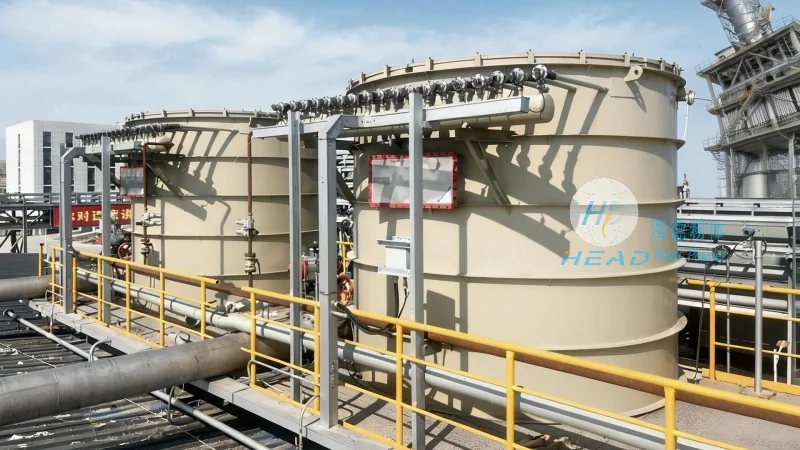
The operation of a chocolate material pneumatic conveying system follows a systematic process that ensures smooth and continuous material transport. The process begins with the loading of the chocolate ingredients into the storage hopper or silo. The system then activates the feeder, which controls the flow rate of the material into the conveyor line. Simultaneously, the blower or air compressor starts, generating the required air pressure to move the material. The material is then drawn into the pipeline and carried to the destination point, such as a mixing tank or processing unit. Throughout the process, the system’s controls monitor pressure, flow rate, and other parameters to maintain optimal performance. If any issues arise, such as a blockage or pressure drop, the system’s safety features will trigger an alarm or automatically adjust the flow to prevent damage to the equipment or the material. The entire operation is designed to be automated, reducing the need for manual intervention and ensuring consistent performance.
Benefits and Applications in Chocolate Manufacturing
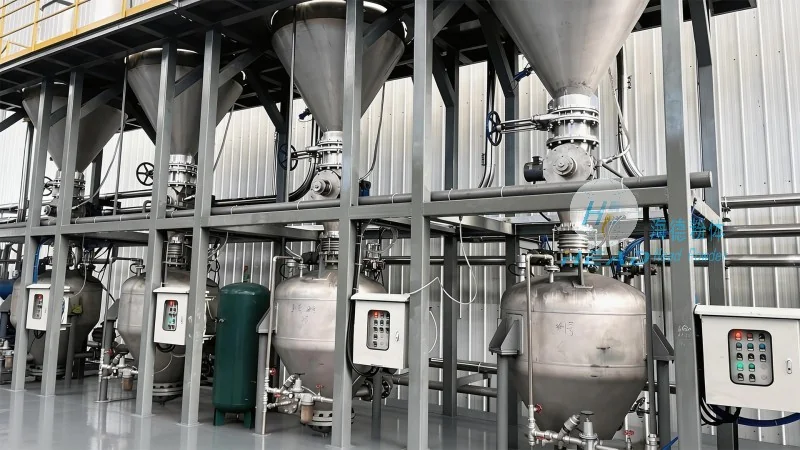
The implementation of a chocolate material pneumatic conveying system offers numerous advantages for chocolate manufacturers. By eliminating the need for manual handling or traditional belt conveyors, the system reduces the risk of contamination and improves product safety. The enclosed pipeline design also minimizes dust exposure, contributing to a cleaner working environment. Additionally, the system’s ability to handle fine and delicate materials without causing damage or degradation enhances product quality. In terms of efficiency, the system can transport materials over longer distances with minimal energy consumption compared to other methods. This makes it an ideal solution for large-scale chocolate production facilities that require consistent and reliable material handling. The system’s flexibility also allows for integration with other processing equipment, such as mixers, ovens, or packaging lines, creating a seamless production workflow.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of material handling solutions, specializes in designing and supplying customized pneumatic conveying systems for various industries, including chocolate production. With a strong commitment to quality and innovation, the company has developed advanced systems that meet the specific needs of chocolate manufacturers. HeadPowder’s systems are engineered to handle the unique challenges of chocolate materials, such as their fine particle size and susceptibility to caking. The company’s team of experts works closely with clients to understand their production requirements and provide tailored solutions that enhance efficiency and product quality. HeadPowder’s facilities are located in Shandong, China, where the company leverages its local expertise and resources to deliver high-quality products and services to customers worldwide.




