Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and installation of advanced material conveying systems. This article provides a detailed overview of the operation process and working principle of their dust-removal ash material conveying system equipment, highlighting the key components, operational flow, and technical aspects that ensure efficient and reliable performance.
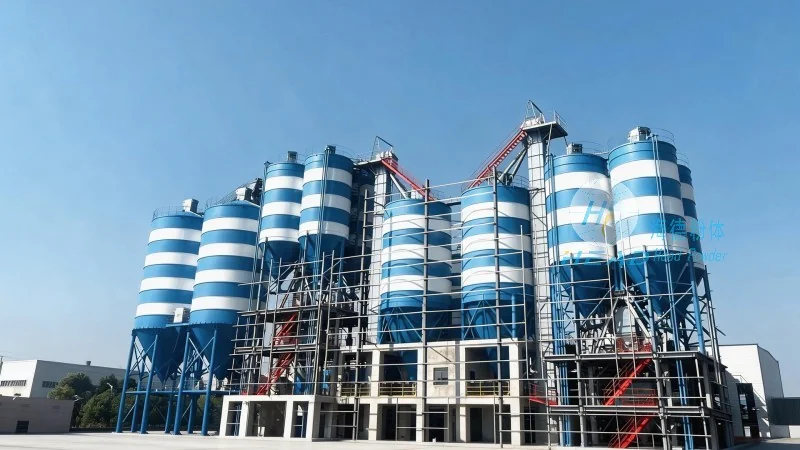
Overview of the Dust-Removal Ash Material Conveying System
The dust-removal ash material conveying system is a critical component in industrial facilities that generate large volumes of ash from dust removal processes. These systems are engineered to handle the transportation of ash from collection points to disposal or recycling locations. The equipment is designed with durability, efficiency, and safety in mind, ensuring it can withstand the harsh conditions often encountered in such environments.
Key Components and Their Functions
The system typically consists of several interconnected components, each playing a vital role in the overall operation. These include ash hoppers, feeding mechanisms, conveyor belts or screw conveyors, control panels, and dust collection systems. The ash hopper is responsible for collecting the ash from the dust removal equipment, while the feeding mechanism ensures a consistent flow of material into the conveyor. The conveyor itself transports the ash to the desired destination, and the control panel allows operators to monitor and adjust the system parameters as needed. The dust collection system is integrated to prevent airborne particles from escaping, maintaining a clean and safe working environment.
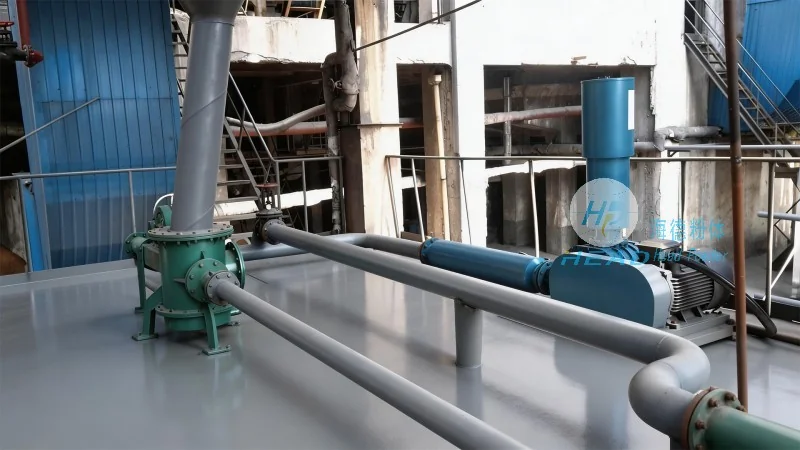
Operation Process of the Conveying System
The operation of the dust-removal ash material conveying system follows a systematic sequence to ensure smooth and continuous material transport. The process begins with the ash being deposited into the ash hopper from the dust removal equipment. The feeding mechanism then activates, gradually releasing the ash into the conveyor. As the conveyor moves, the ash is transported to the discharge point, which may be a storage silo, a truck loading station, or another processing facility. Throughout the process, the control panel continuously monitors parameters such as flow rate, pressure, and temperature, providing real-time feedback to the operators. Any deviations from the set parameters are immediately detected and corrected, ensuring the system operates within optimal conditions.
Working Principle of the System
The working principle of the dust-removal ash material conveying system is based on mechanical energy transfer and material handling technology. The system utilizes either a belt conveyor or a screw conveyor, depending on the specific requirements of the application. In a belt conveyor system, the ash is placed on the moving belt, which transports it through the system. The screw conveyor, on the other hand, uses a rotating screw to push the ash forward. Both systems rely on the principle of gravity and mechanical force to move the material. The control system regulates the speed and direction of the conveyor, ensuring that the ash is transported at a consistent rate. Additionally, the system incorporates safety features such as emergency stop buttons and overload protection to prevent accidents and equipment damage.
Advantages and Benefits of the System
The dust-removal ash material conveying system offers several advantages that make it an ideal solution for industrial applications. Firstly, it provides a highly efficient and reliable method of transporting ash, reducing the need for manual handling and minimizing the risk of accidents. Secondly, the system is designed to be low-maintenance, with components that are easy to replace and service, reducing downtime and operational costs. Thirdly, the integration of dust collection systems ensures that the working environment remains clean and safe, complying with environmental regulations. Finally, the system can be customized to meet the specific needs of different industries, such as power plants, cement factories, and waste management facilities, making it a versatile and adaptable solution.
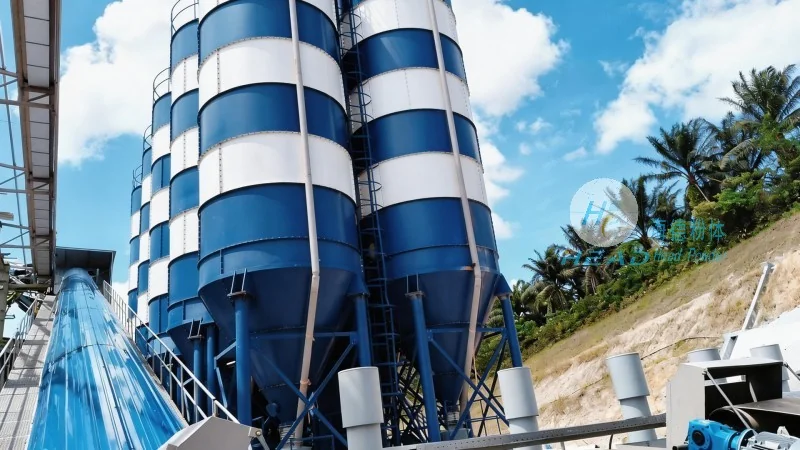
Applications and Industries
The dust-removal ash material conveying system is widely used in various industries that generate significant amounts of ash. These include thermal power plants, where the system is used to transport fly ash from the electrostatic precipitators to storage or disposal sites. In cement factories, the system handles the transportation of raw materials and byproducts, improving the overall efficiency of the production process. Additionally, the system is used in waste management facilities to transport ash from incinerators to landfills or recycling centers. The versatility of the system makes it suitable for a wide range of applications, ensuring that it can be adapted to meet the specific requirements of different industrial settings.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides high-quality dust-removal ash material conveying systems that are designed to meet the demands of modern industrial applications. The system's efficient operation, reliable performance, and safety features make it an essential component in facilities that require the transportation of ash. By understanding the operation process and working principle of the system, users can ensure optimal performance and maximize the benefits of this advanced equipment. With its commitment to quality and innovation, headpowder continues to be a leader in the design and manufacturing of material conveying systems, providing solutions that enhance operational efficiency and safety in various industries.




