HeadPowder, a professional manufacturer based in Shandong, China, specializes in the design and production of pneumatic conveying systems tailored for light calcium powder applications. This article provides an in-depth exploration of the operational principles and typical working scenarios of such systems, offering insights into their efficiency and versatility in industrial settings.
Company Overview
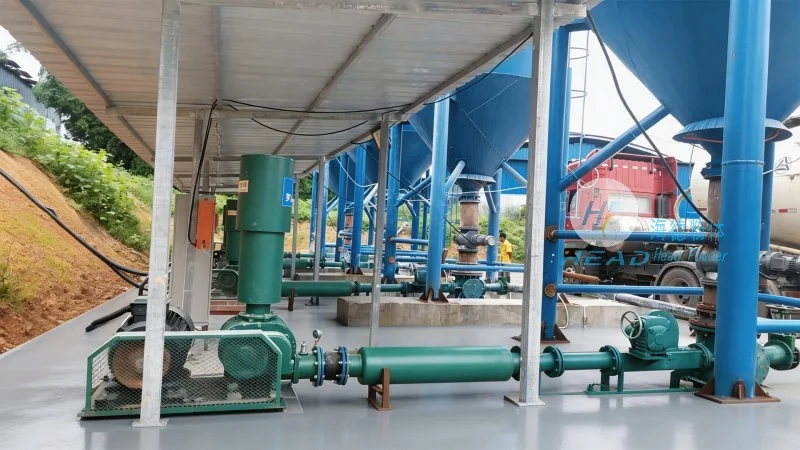
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading enterprise in the field of material handling solutions. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality pneumatic conveying systems that meet the specific needs of various industries. The company's commitment to innovation and precision engineering ensures that their products are reliable and efficient, supporting the smooth operation of industrial processes.
The Principle of Light Calcium Powder Pneumatic Conveying System
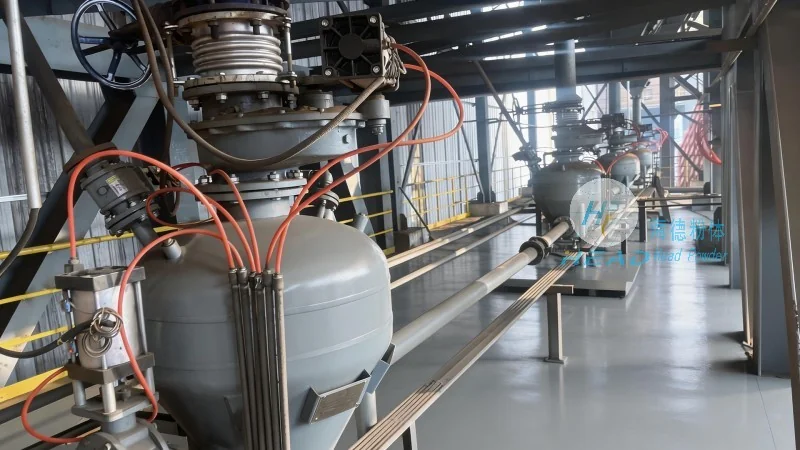
The light calcium powder pneumatic conveying system operates on the fundamental principle of transporting dry powders through a pipeline using a carrier gas, typically air. This method, known as pneumatic conveying, eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and enhancing safety. The system works by creating a pressure differential within the pipeline, which draws the light calcium powder into the air stream and transports it to the desired destination. Key components include a feeding hopper, a conveying pipeline, a gas source (usually a blower or compressor), and a discharge device. The feeding hopper ensures a consistent supply of powder, while the blower generates the necessary air pressure to move the material. The pipeline design, often with bends and valves, is optimized to minimize pressure loss and maintain the flow of powder. The discharge device, such as a rotary valve or a venturi, controls the release of the powder at the end of the pipeline. The entire system is designed to handle the low density and fine particle size of light calcium powder, which can be challenging for traditional conveying methods. By utilizing the air flow to move the powder, the system achieves high efficiency and minimal product degradation, making it ideal for applications where product quality is paramount.
Working Scene Characteristics of the System
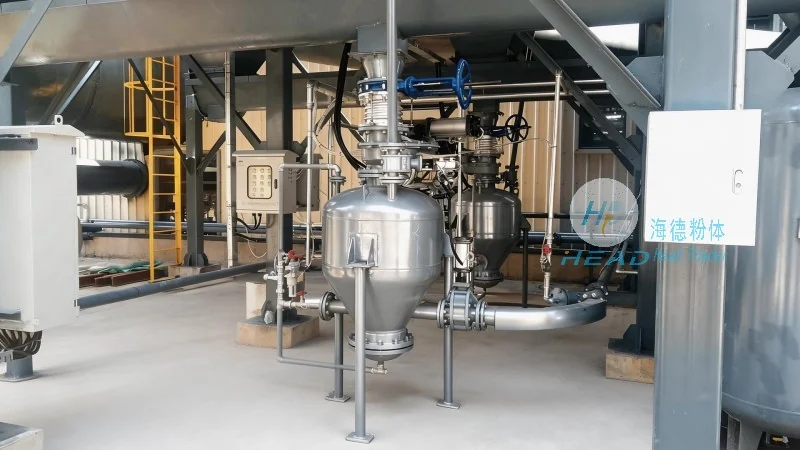
The light calcium powder pneumatic conveying system is particularly well-suited for applications in the chemical, food, and pharmaceutical industries, where the handling of fine powders requires strict control over dust, contamination, and product integrity. In these working scenarios, the system's ability to transport light calcium powder in a closed pipeline is crucial. The closed system prevents dust from escaping into the environment, maintaining a clean and safe working environment. This is especially important in industries where dust can be hazardous or where product purity is critical. The system's flexibility allows it to be integrated into existing production lines, adapting to various production scales and layouts. For example, in a chemical plant, the system can be used to transport light calcium powder from storage silos to mixing equipment, ensuring a continuous and controlled flow of material. In a food processing facility, the system can handle light calcium powder used as an ingredient, maintaining the hygiene standards required by food safety regulations. The system's efficiency also translates into cost savings, as it reduces the need for manual handling and minimizes product loss due to spillage or degradation. Additionally, the system's low maintenance requirements and long service life contribute to its overall economic viability. In summary, the working scene characteristics of the light calcium powder pneumatic conveying system highlight its adaptability and effectiveness in diverse industrial applications, making it a preferred choice for industries that demand high-quality, reliable material handling solutions.




