HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced material handling equipment. This article focuses on the working principle and key features of the bulk bag unloading station material pneumatic conveying machine, a critical solution for efficient bulk material transfer in industrial applications.
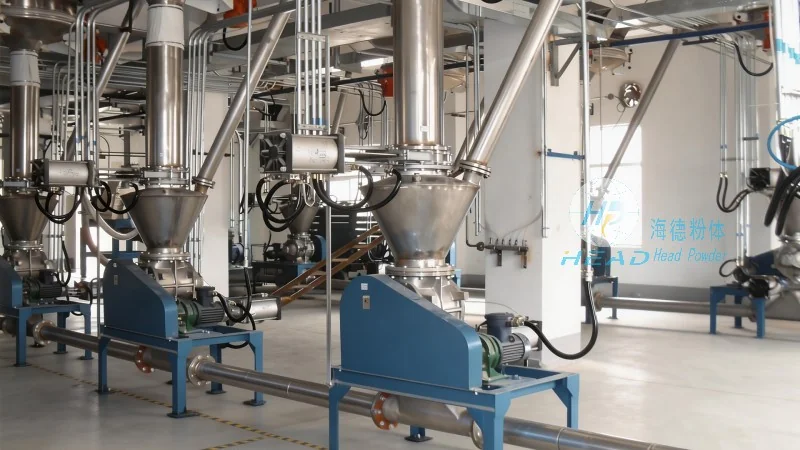
Overview of Bulk Bag Unloading Station Material Pneumatic Conveying Machine
The bulk bag unloading station material pneumatic conveying machine is a specialized system engineered to handle the unloading, conveying, and processing of bulk materials from bulk bags (also known as super sacks or FIBCs) into storage silos, hoppers, or other processing equipment. This equipment is particularly valuable in industries such as chemicals, food, pharmaceuticals, and mining, where large volumes of powders or granules need to be managed safely and efficiently.
Working Principle of the Pneumatic Conveying System
The core of the bulk bag unloading station material pneumatic conveying machine operates on the principle of pneumatic transport, which uses air as the conveying medium to move bulk materials through a pipeline network. The process typically involves several key steps:
1. Unloading and Feeding: The bulk bag is placed on a discharge frame or hopper, and the machine uses a combination of mechanical and pneumatic forces to open the bag and release the material. A hopper or feeder at the bottom of the bag ensures a controlled flow of material into the conveying system.
2. Air Supply and Material Conveying: Compressed air is introduced into the conveying line, creating a pressure differential that propels the material through the pipeline. The air flow is regulated to maintain a consistent velocity, preventing material degradation or blockages. The conveying system may include vertical, horizontal, or inclined sections, depending on the layout of the facility.
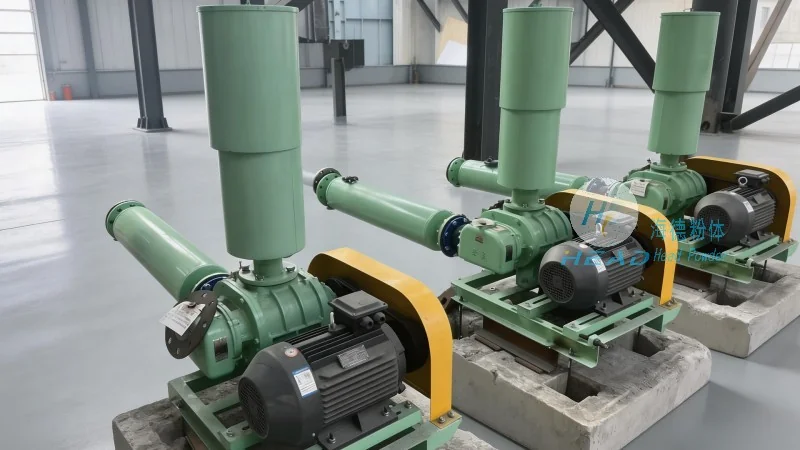
3. Material Delivery and Dosing: The material is transported to the target destination, such as a silo or processing unit. The system can be equipped with dosing mechanisms to control the flow rate, ensuring precise material delivery for downstream processes.
Key Features and Advantages
The bulk bag unloading station material pneumatic conveying machine from HeadPowder offers several distinct features that enhance operational efficiency and safety:
1. Efficient Material Handling: The system minimizes manual labor by automating the unloading and conveying process, reducing the risk of dust exposure and material spillage. It can handle a wide range of bulk materials, including powders, granules, and fine particles, with minimal degradation.
2. Customizable Design: HeadPowder provides tailored solutions based on the specific requirements of the client, including the capacity, material type, and facility layout. The equipment can be configured with vertical or horizontal conveying sections, as well as various inlet and outlet options.
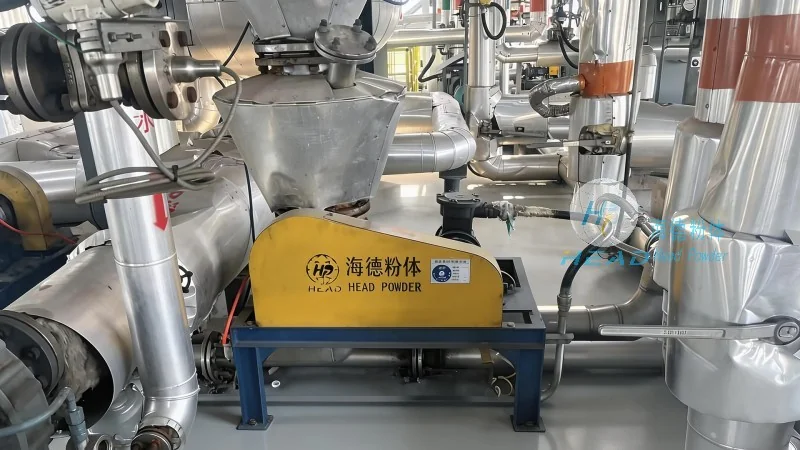
3. Low Maintenance and Durability: The components are constructed from high-quality materials, such as stainless steel and corrosion-resistant alloys, ensuring long-term durability and minimal maintenance. The system is designed for easy cleaning and maintenance, reducing downtime and operational costs.
4. Environmental and Safety Compliance: The machine incorporates dust collection and filtration systems to comply with environmental regulations and ensure a safe working environment. It also features safety interlocks and emergency stop mechanisms to prevent accidents during operation.
Application Examples
The bulk bag unloading station material pneumatic conveying machine is widely used in various industrial sectors. For instance, in the chemical industry, it is used to transfer raw materials such as powders and granules into reactors or storage tanks. In the food and pharmaceutical industries, it ensures hygienic and contamination-free material handling, meeting stringent quality standards. In mining operations, it facilitates the transport of ore and other bulk materials from the mine to processing facilities.
Conclusion
HeadPowder's bulk bag unloading station material pneumatic conveying machine represents a reliable and efficient solution for bulk material handling. By leveraging advanced pneumatic technology and robust engineering, the system enhances productivity, reduces labor costs, and ensures compliance with safety and environmental regulations. As a trusted provider of material handling equipment, HeadPowder continues to innovate and deliver high-quality solutions tailored to the evolving needs of industrial applications.




