Sugar material pneumatic conveying equipment is a critical component in the sugar processing industry, engineered to efficiently transport bulk sugar within processing facilities. This technology leverages compressed air as the primary medium to move sugar particles, offering a clean, dust-free, and hygienic method of material handling that is essential in food processing environments. The evolution of pneumatic conveying systems has provided manufacturers with reliable solutions for handling delicate and high-value sugar products, ensuring operational efficiency and product integrity. This article explores the working principle and key features of such equipment, highlighting its role in enhancing productivity and maintaining quality standards in sugar processing plants.
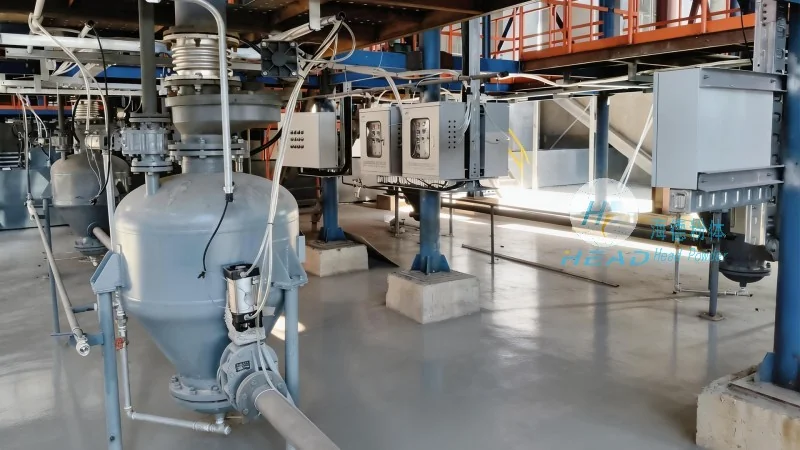
Understanding the Working Principle of Sugar Material Pneumatic Conveying Equipment
The fundamental working principle of sugar material pneumatic conveying equipment centers on the use of compressed air to create a flow of material through a pipeline network. The system typically comprises a hopper for material storage, a blower or air compressor to generate the air flow, a series of pipelines, and a receiver or discharge point. When activated, the blower produces a high-pressure air stream that either pulls (suction) or pushes (blow) the sugar particles into the pipeline. The air flow creates a negative or positive pressure environment, depending on the system design, to move the material. Sugar particles are suspended in the air stream and transported through the pipeline to the designated destination. This process is continuous and can handle various sugar forms—including granulated, powdered, or crystalline sugar—without mechanical components that might cause contamination or damage to the product. The enclosed pipeline design ensures that the material remains contained, preventing exposure to external contaminants and maintaining product purity.
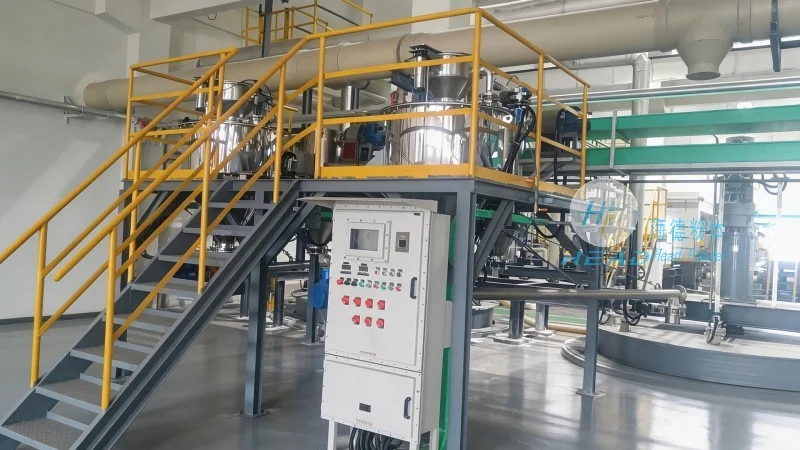
Key Features of Sugar Material Pneumatic Conveying Equipment
Several key features make sugar material pneumatic conveying equipment an ideal choice for sugar processing applications. First, the system offers a hygienic and dust-free operation, which is paramount in food processing environments where contamination control is critical. The enclosed pipeline design prevents exposure to external elements and minimizes the risk of cross-contamination, ensuring compliance with food safety regulations. Second, the equipment provides high efficiency in material transport, capable of moving large volumes of sugar quickly and reliably. This reduces labor costs and increases overall productivity in processing plants. Third, the system is flexible and adaptable to various plant layouts, with the ability to install multiple inlets and outlets to accommodate different processing stages. Additionally, the equipment is easy to maintain, with accessible components that are simple to replace, reducing downtime and maintenance expenses. Finally, the technology offers a clean and safe operation, with no moving parts that come into direct contact with the sugar, ensuring product integrity and enhancing operational safety.
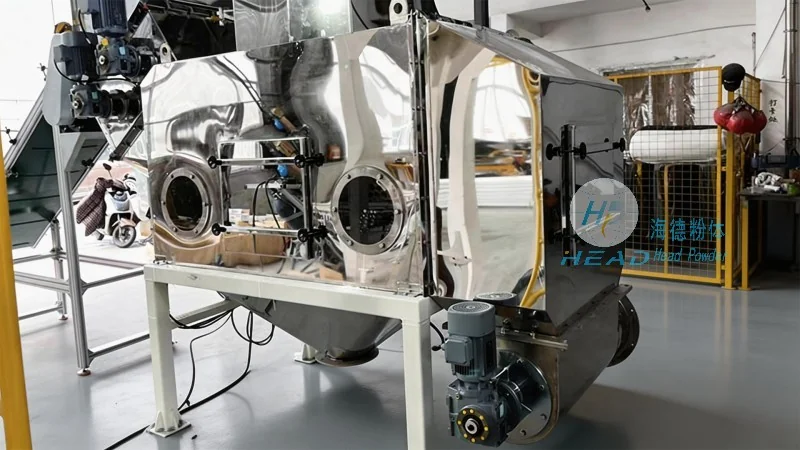
Applications and Benefits in Sugar Processing
Sugar material pneumatic conveying equipment is widely utilized across various stages of sugar processing, from raw sugar handling to final product packaging. In the raw sugar processing stage, the equipment transports raw sugar from storage silos to processing lines, ensuring a continuous supply of material. During the refining process, it moves refined sugar crystals from crystallization tanks to packaging areas. The system is also employed in the production of powdered sugar, efficiently transporting fine particles from grinding and sieving stages to packaging machines. The benefits of using pneumatic conveying systems in these applications include improved product quality, reduced handling time, and enhanced operational safety. The clean and enclosed design of the equipment helps maintain the purity of the sugar, which is essential for meeting high standards of food safety and quality in the industry.
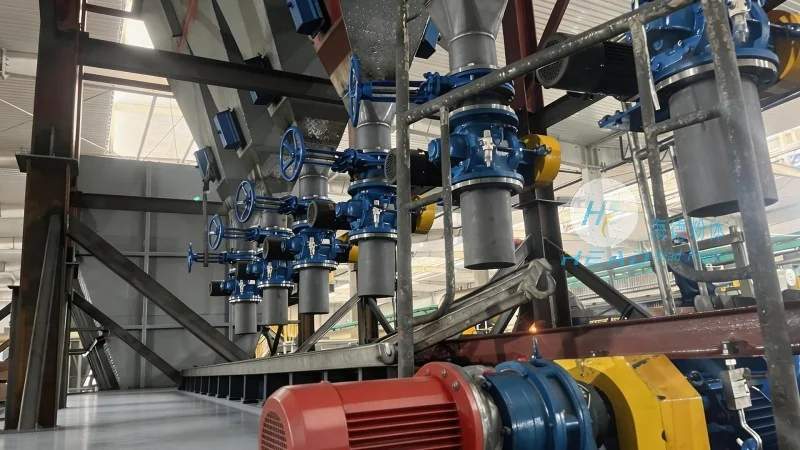
Company Information: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer of pneumatic conveying equipment for the sugar industry. The company is headquartered in Shandong, China, and has established itself as a trusted provider of high-quality, reliable, and efficient sugar material handling solutions. With years of experience in the industry, HeadPowder has developed a range of pneumatic conveying systems tailored to the specific needs of sugar processing plants. The company's products are designed to meet stringent food safety standards, ensuring compliance with international regulations. HeadPowder's commitment to quality and customer satisfaction has made it a preferred choice for sugar manufacturers worldwide, offering tools to optimize operations and improve product quality. The company's expertise in engineering and manufacturing ensures that each system is customized to enhance productivity and maintain the integrity of sugar products throughout the processing chain.




