Food powder pneumatic conveying equipment plays a vital role in the food processing sector, offering an efficient method to transport bulk powders such as flour, sugar, and other food ingredients. This technology utilizes compressed air as the primary medium to move powders through a network of pipes and components, providing a hygienic and adaptable solution for material handling. Understanding the working principle and key features of these systems is essential for appreciating their application and benefits in food production environments.
Working Principle of Food Powder Pneumatic Conveying Equipment
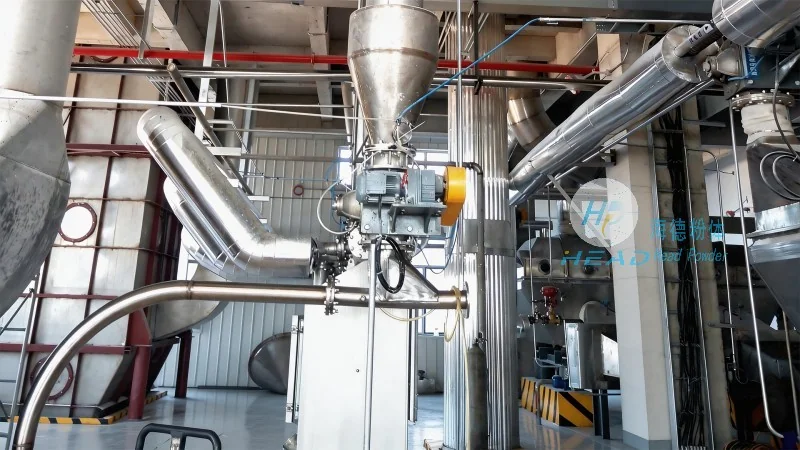
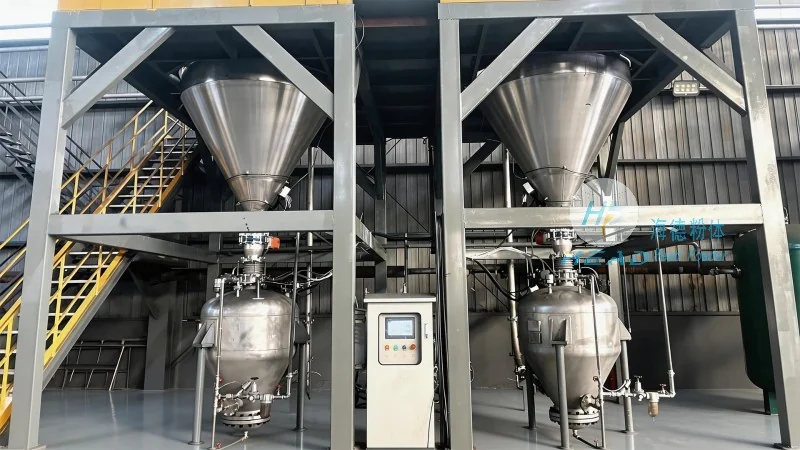
The fundamental operation of food powder pneumatic conveying equipment revolves around the use of compressed air to generate a flow that propels powders through a pipeline. The process typically starts with the powder being fed into a hopper or feeder, where it is then introduced into the conveying line. As compressed air is introduced into the system, it creates a pressure differential that draws the powder particles into the air stream. This air-powder mixture travels through the pipeline, often aided by components like in-line mixers or cyclones, to separate the powder from the air at the discharge point. The air is then typically filtered and recycled back into the system, ensuring energy efficiency and minimal waste. The entire process is engineered to preserve the integrity of the food product, preventing contamination and maintaining consistent quality throughout the conveying operation.
Key Features of Food Powder Pneumatic Conveying Equipment
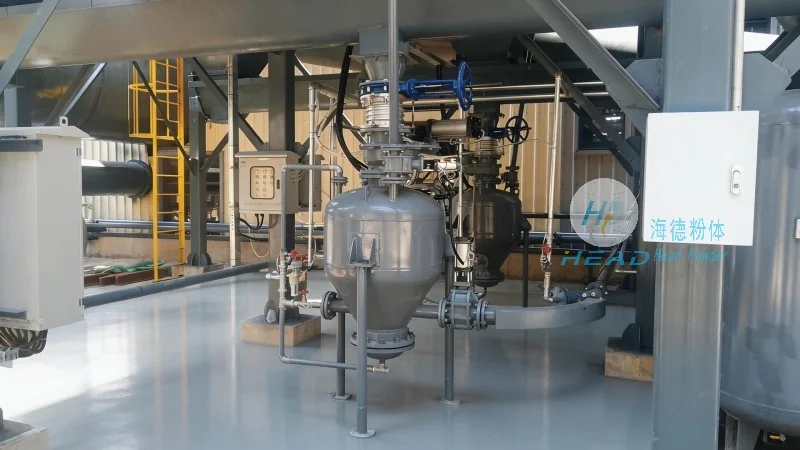
Food powder pneumatic conveying systems exhibit several notable advantages that make them well-suited for food processing applications. A primary feature is their hygienic design, which includes smooth, easy-to-clean surfaces and components that minimize the risk of product contamination. This is critical in the food industry, where maintaining product safety and compliance with regulatory standards is paramount. Additionally, these systems offer high flexibility in terms of layout and integration with existing production lines, allowing for customization to meet diverse operational needs. Another significant feature is the ability to handle a wide range of powder characteristics, including varying particle sizes, densities, and moisture contents, without requiring extensive modifications. This versatility makes them suitable for diverse food products, from fine powders like cocoa to bulkier materials like sugar. Furthermore, the systems are generally compact, optimizing space utilization in food processing facilities. The energy efficiency of pneumatic conveying, particularly with recycling systems, also contributes to cost savings and reduced environmental impact.
Company Information and Expertise
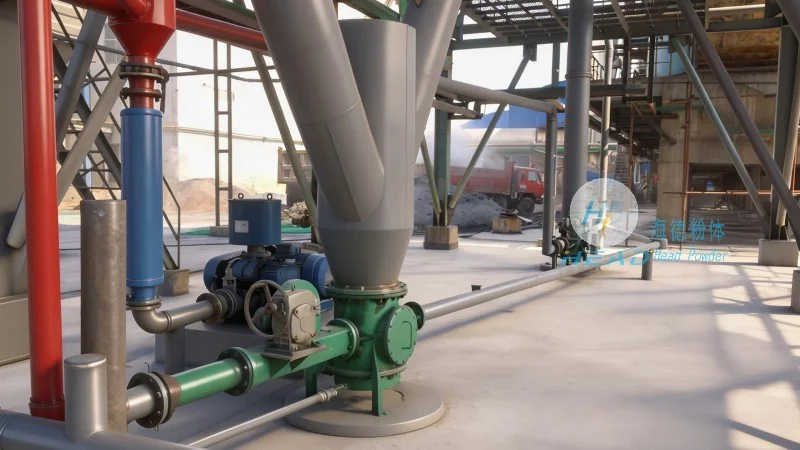
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer specializing in the design and production of food powder pneumatic conveying equipment. With a focus on innovation and quality, the company has established itself as a trusted partner in the food processing industry. Headpowder's expertise lies in developing customized solutions that meet the specific requirements of food manufacturers, ensuring optimal performance and compliance with industry standards. The company's facilities are located in Shandong, China, where advanced manufacturing processes and rigorous quality control measures are employed to produce reliable and durable equipment. By leveraging years of experience and technical expertise, headpowder provides comprehensive support, from initial system design and installation to ongoing maintenance and troubleshooting, helping clients maximize the efficiency and safety of their powder handling operations.




