When it comes to efficient and reliable handling of bulk powders, the bulk bag unpacking powder pneumatic conveying system stands out as a critical solution in industrial operations. This equipment is designed to streamline the process of transferring large quantities of powders from bulk bags into processing systems, ensuring minimal loss and maximum efficiency. The following sections will delve into the working principle and key features of this advanced system.
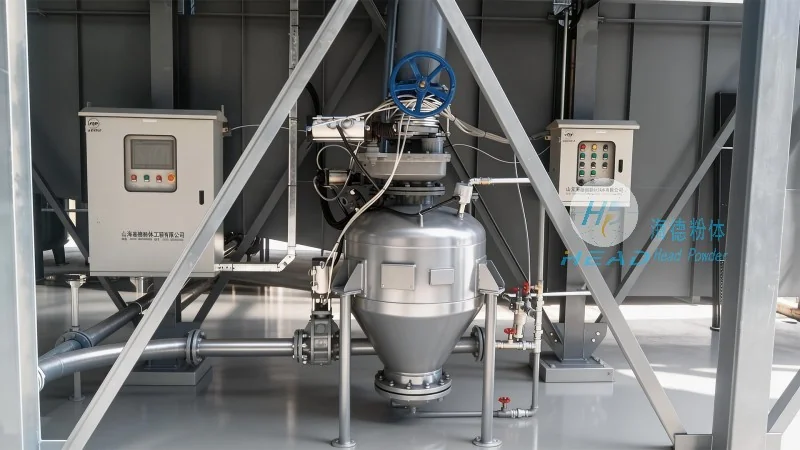
Working Principle of Bulk Bag Unpacking Powder Pneumatic Conveying Equipment
The core of the bulk bag unpacking powder pneumatic conveying system lies in its integrated approach to material handling. The process typically begins with the placement of a bulk bag (also known as a super sack or FIBCs) onto a specialized frame or hopper. The system then uses a combination of vacuum or pressure air flow to draw the powder from the bag and transport it through a pipeline to the desired destination, such as a silo, storage tank, or processing unit. This pneumatic method eliminates the need for manual handling, reducing labor costs and minimizing the risk of dust exposure and material contamination. The equipment is equipped with airtight seals and filtration systems to maintain air quality and prevent dust from escaping into the environment. The conveying line is often equipped with check valves and flow control devices to regulate the speed and direction of the powder flow, ensuring smooth and consistent operation. The entire system is designed to handle a wide range of powder types, from fine powders like cement and flour to bulkier materials such as plastics and chemicals, adapting to various industrial needs.
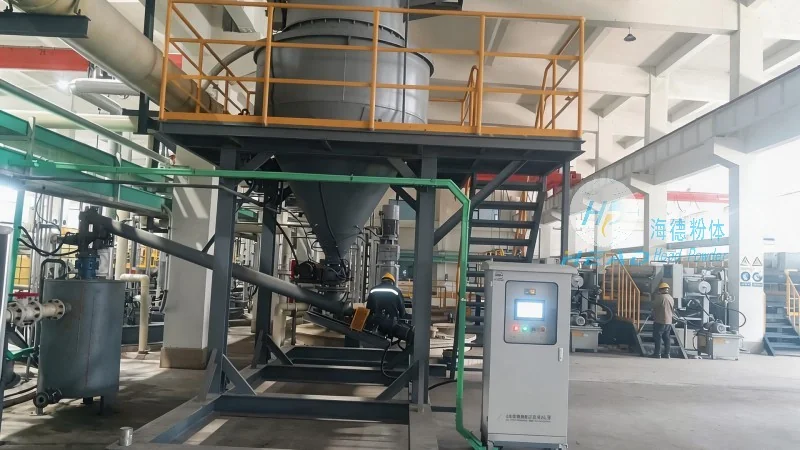
Key Features of the Bulk Bag Unpacking Powder Pneumatic Conveying System
One of the standout features of this equipment is its ability to handle large volumes of material with minimal human intervention. The system is engineered for high throughput, capable of processing several tons of powder per hour, making it ideal for high-demand industrial applications. The design incorporates robust materials and components that can withstand the rigors of continuous operation, ensuring long-term reliability and low maintenance costs. Safety is a top priority, with built-in safety features such as overpressure relief valves and dust suppression systems to protect both personnel and equipment. The system also offers flexibility in terms of layout and integration, allowing it to be customized to fit existing facility configurations without major structural modifications. Additionally, the equipment is equipped with monitoring and control systems that provide real-time data on flow rates, pressure, and material levels, enabling operators to optimize performance and troubleshoot issues quickly. The use of pneumatic conveying technology also minimizes product degradation, as the powder is conveyed in a closed system, protecting it from moisture, contamination, and exposure to air, which is particularly important for sensitive materials like pharmaceuticals or food products.
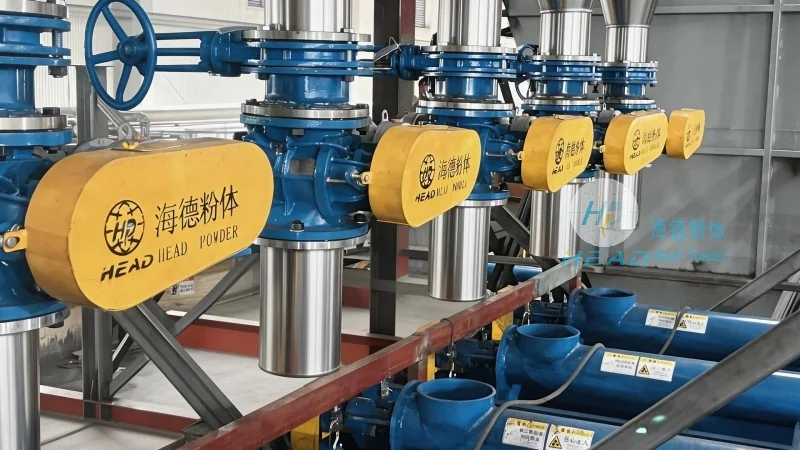
Applications and Benefits in Industrial Settings
The bulk bag unpacking powder pneumatic conveying system finds extensive applications across various industries, including food processing, pharmaceuticals, chemicals, and plastics. In the food industry, it is used to handle ingredients like flour, sugar, and spices, ensuring hygienic and dust-free transfer. In pharmaceutical manufacturing, the system maintains strict contamination control, adhering to GMP (Good Manufacturing Practice) standards. The chemical industry benefits from the system's ability to handle hazardous materials safely, with sealed systems preventing leaks and exposure. The plastics industry uses it for transporting raw materials like polymers and additives, enhancing production efficiency. The primary benefits of this equipment include improved operational efficiency, reduced labor costs, enhanced product quality through minimal contamination, and increased safety for workers. By automating the bulk bag unpacking process, the system also reduces the risk of accidents associated with manual handling, such as spills and dust inhalation. Furthermore, the closed-loop design of the pneumatic conveying system contributes to environmental sustainability by minimizing dust emissions and waste.
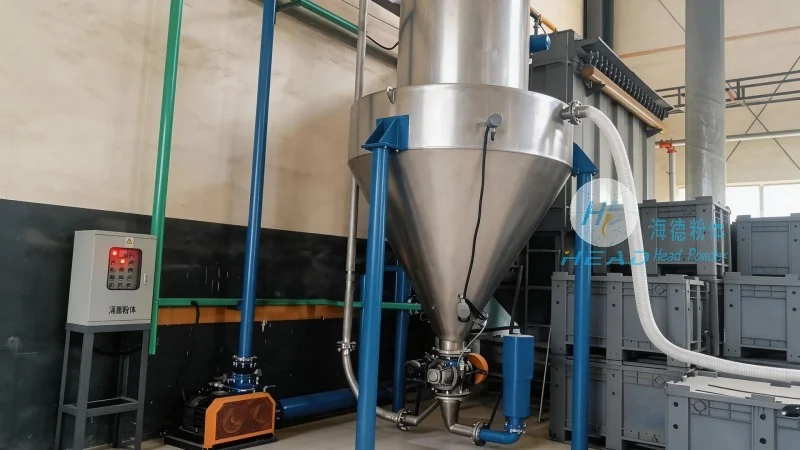
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
As a leading provider of industrial material handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing advanced bulk bag unpacking and pneumatic conveying systems. With a strong commitment to innovation and quality, the company has established itself as a trusted partner for businesses seeking reliable and efficient powder handling equipment. HeadPowder's expertise lies in customizing solutions to meet specific customer requirements, ensuring that each system is tailored to the unique needs of the application. The company's products are built with high-quality materials and components, backed by rigorous testing and quality control processes to guarantee performance and durability. HeadPowder's team of engineers and technicians work closely with clients to understand their operational challenges and develop tailored solutions that enhance productivity and reduce costs. The company's facilities are located in Shandong, China, where it leverages local manufacturing capabilities to deliver cost-effective and high-performance equipment. HeadPowder's dedication to customer satisfaction and technical excellence has earned it a reputation as a leading supplier in the industry, with a focus on providing sustainable and efficient solutions for bulk powder handling.




