What is a cocoa powder bulk material handling system? What are its design principles?
Release time:2026-09-15 18:01:17
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For manufacturers and processors in the cocoa industry, efficient and reliable handling of cocoa powder is crucial to maintaining product quality and operational efficiency. A cocoa powder bulk material handling system is a specialized piece of equipment designed to transport, store, and manage cocoa powder in bulk form. This system is essential for ensuring smooth production workflows and minimizing the risk of contamination or loss during material transfer.
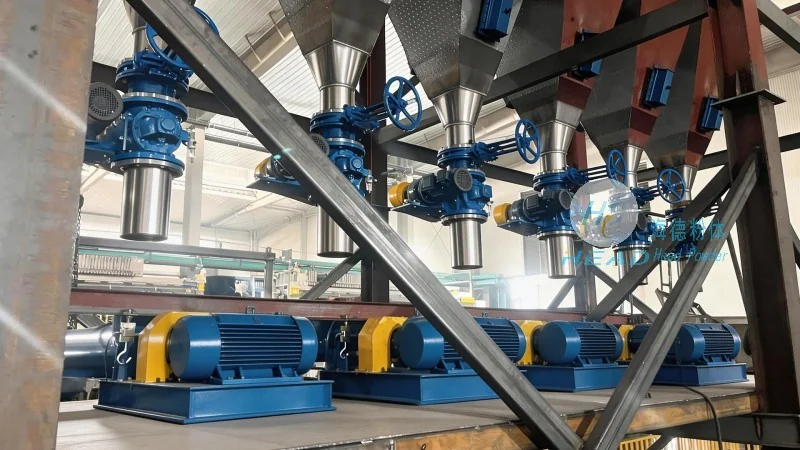
Understanding the Components of a Cocoa Powder Bulk Handling System
A typical cocoa powder bulk material handling system consists of several key components that work together to achieve efficient material flow. These components include bulk storage silos or hoppers, conveying equipment such as screw conveyors or pneumatic systems, and control systems that regulate the flow of material. The system is designed to handle the unique properties of cocoa powder, which can be fine, dusty, and prone to caking under certain conditions.
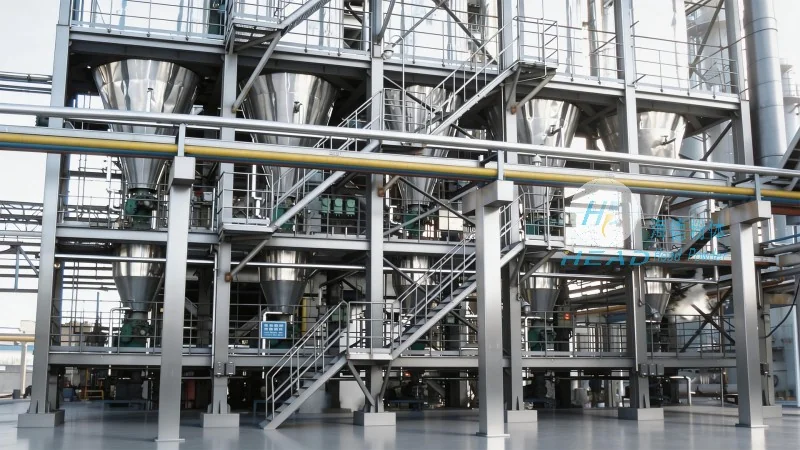
The Design Principles Behind Cocoa Powder Handling Equipment
The design of a cocoa powder bulk handling system is guided by several key principles to ensure optimal performance and safety. First, the system must be constructed from materials that are compatible with cocoa powder and resistant to corrosion or contamination. Stainless steel is commonly used for components that come into direct contact with the product due to its hygienic properties and durability. Second, the system is engineered to minimize dust generation and prevent product degradation. This is achieved through features like airtight seals, dust collection systems, and gentle handling mechanisms that prevent excessive friction or impact.
Key Features of a Professional Cocoa Powder Handling System
Professional systems from companies like Shandong HeadPowder Engineering Co., Ltd. incorporate advanced features to enhance performance and user experience. These features may include automated control panels that allow operators to monitor and adjust system parameters in real-time, as well as integration with other production equipment for seamless workflow management. The system is also designed for easy maintenance and cleaning, with removable parts that can be sanitized to meet food safety standards. Additionally, the equipment is built to handle varying capacities, from small-scale operations to large industrial production lines, ensuring versatility for different business needs.
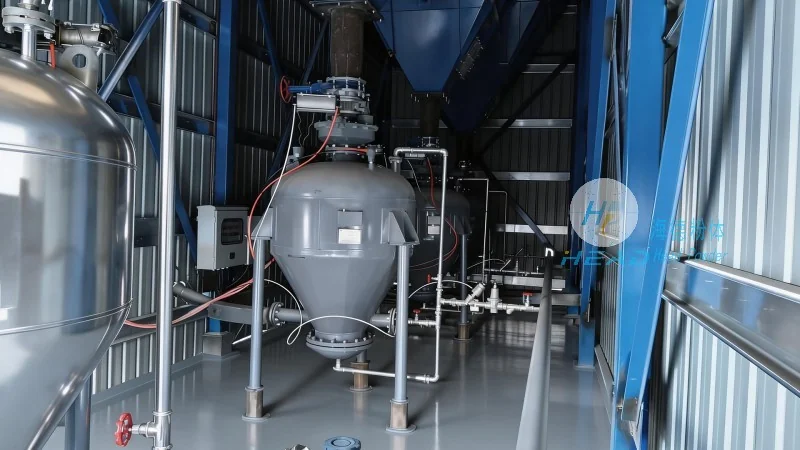
Benefits of Implementing a Bulk Material Handling System for Cocoa Powder
Adopting a cocoa powder bulk material handling system offers numerous benefits for businesses in the cocoa industry. One of the primary advantages is improved operational efficiency, as the system automates the material transfer process, reducing the need for manual handling and minimizing downtime. This leads to increased productivity and cost savings over time. Another benefit is enhanced product quality, as the system minimizes exposure to air and moisture, which can cause caking or spoilage. This helps maintain the consistent texture and flavor of the cocoa powder, which is critical for downstream processing and product quality. Furthermore, the system improves workplace safety by reducing the risk of dust inhalation and accidents associated with manual material handling. By investing in a well-designed bulk handling system, companies can ensure a stable and reliable supply of cocoa powder while maintaining high standards of hygiene and efficiency.




