What is a Dust-Free Automatic Powder Conveying Machine? And What Are Its Design Principles?
Release time:2026-09-15 17:01:19
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
For industries dealing with powders and bulk materials, maintaining a clean and efficient production environment is paramount. A dust-free automatic powder conveying machine plays a crucial role in achieving this goal by ensuring the safe and hygienic transfer of powders while minimizing contamination and dust emissions. This article explores the fundamental design principles behind such machines and their significance in modern industrial applications.
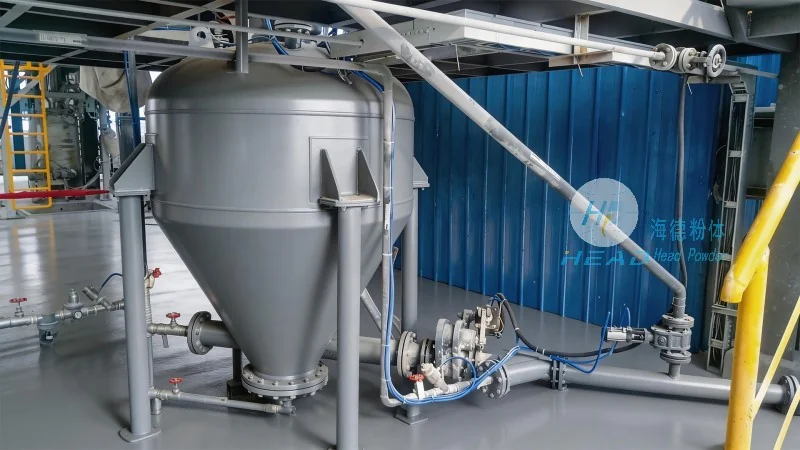
Key Components and Design Features of Dust-Free Powder Conveying Systems
The core of a dust-free automatic powder conveying machine lies in its integrated design that prioritizes containment and control. Key components typically include a sealed hopper for material storage, a conveying mechanism (such as pneumatic or screw conveyors), and a filtration system to capture any airborne particles. The machine is engineered to operate under negative pressure or with enclosed pathways, preventing dust from escaping into the surrounding environment. This design ensures compliance with industrial hygiene standards and reduces the risk of product contamination.
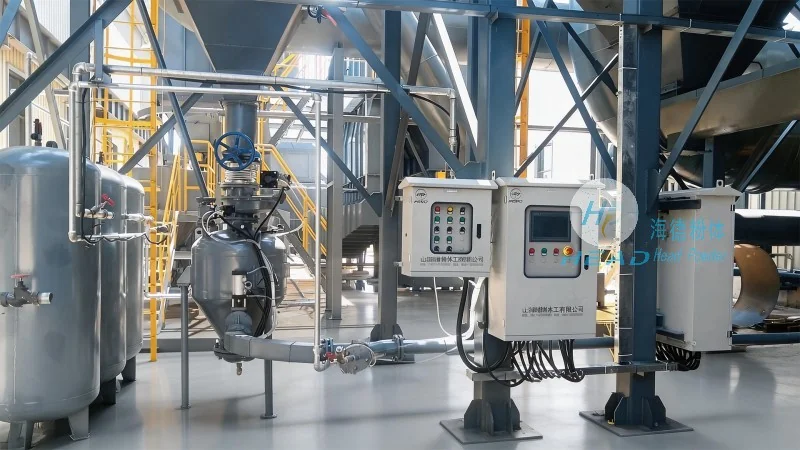
How the Conveying Process Works: From Storage to Delivery
When material is added to the sealed hopper, the conveying system begins its operation. Depending on the specific design, the machine may use compressed air to create a flow of material through the system or utilize a rotating screw to push the powder forward. The enclosed pathways and sealed connections eliminate the possibility of dust leakage, ensuring that the material remains contained throughout the entire process. The filtration system at the discharge end captures any residual particles, further enhancing the dust-free operation. This process not only maintains a clean workspace but also protects equipment and personnel from exposure to harmful powders.
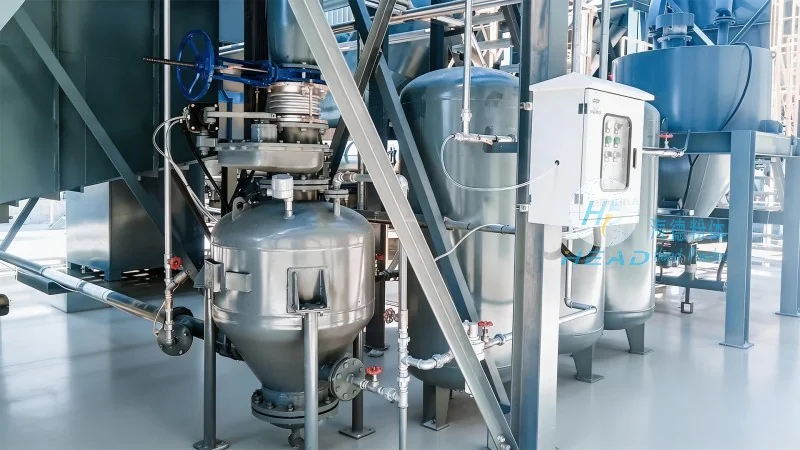
Applications in Various Industries
Dust-free automatic powder conveying machines are widely used across multiple sectors, including pharmaceuticals, food processing, chemical manufacturing, and cosmetics. In the pharmaceutical industry, for example, these machines are essential for handling active ingredients and ensuring product purity. The sealed design prevents cross-contamination and maintains the integrity of sensitive materials. Similarly, in food processing, the equipment helps maintain food safety standards by preventing dust and contaminants from entering the product stream. Chemical manufacturers benefit from the ability to handle hazardous powders without exposing workers to risks, while cosmetics producers ensure that their products remain free from impurities.
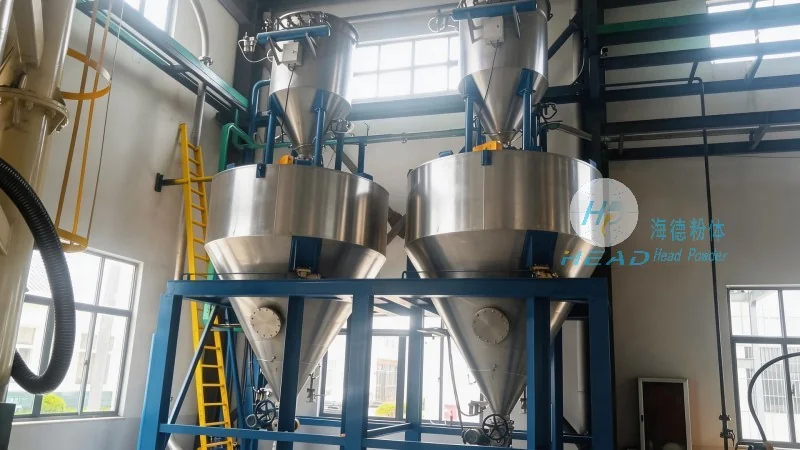
Manufacturing by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of high-quality dust-free automatic powder conveying machines. With years of experience in the industry, the company has developed advanced solutions tailored to meet the diverse needs of various applications. The company’s products are engineered with precision, incorporating robust materials and innovative technologies to ensure durability and reliability. HeadPowder’s commitment to quality and customer satisfaction has made it a trusted name in the market, providing industries with efficient and safe powder handling solutions.




