HeadPowder, a leading provider in the field of material handling solutions, specializes in advanced pneumatic conveying technologies tailored for the efficient transport of flexible coke powder. This article delves into the core principles of vacuum and positive pressure pneumatic conveying systems, offering a comprehensive understanding of their applications and benefits in industrial settings.
Company Overview: HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is dedicated to delivering innovative and reliable material handling solutions. With a strong focus on technological advancement and customer satisfaction, the company has established itself as a trusted partner for industries requiring efficient and safe transport of bulk materials like coke powder. The company's expertise lies in designing and implementing customized pneumatic conveying systems that meet the unique demands of various industrial applications.
In-Depth Analysis of Vacuum Pneumatic Conveying for Coke Powder
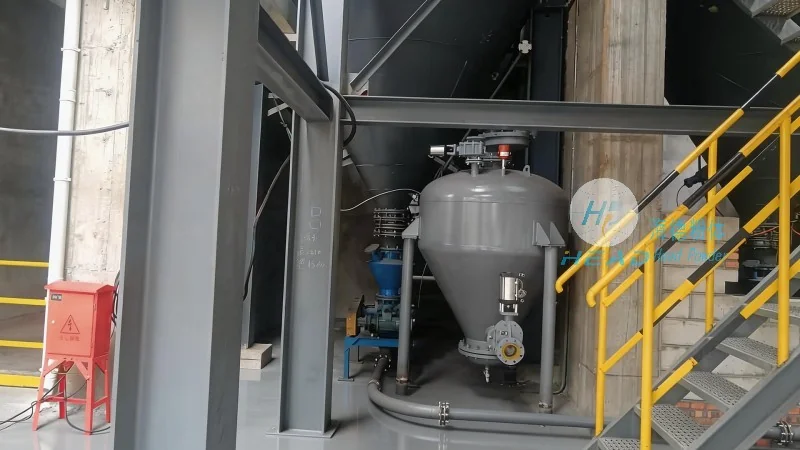
Vacuum pneumatic conveying systems are widely used for the transport of flexible coke powder due to their ability to handle materials over long distances and through complex layouts. These systems operate by creating a negative pressure environment at the inlet, which draws the material into the conveying line using a vacuum pump. The process involves several key components, including a hopper, a rotary valve, a vacuum pump, and a filter system. The hopper serves as the material storage and feeding unit, while the rotary valve controls the flow of coke powder into the conveying line. The vacuum pump generates the necessary suction force to move the material, and the filter system ensures that the conveyed powder is free from contaminants and can be safely discharged at the destination.
A key advantage of vacuum systems is their ability to handle materials with varying moisture content and particle sizes, making them suitable for a wide range of coke powder applications. They are particularly effective in applications where the material needs to be transported from multiple sources or through vertical and horizontal combinations. The flexibility of vacuum systems allows for easy integration with existing production lines, reducing downtime and operational costs. Additionally, these systems are known for their low noise levels and minimal maintenance requirements, contributing to a safer and more efficient working environment.
Positive Pressure Pneumatic Conveying: An Alternative for Coke Powder Transport
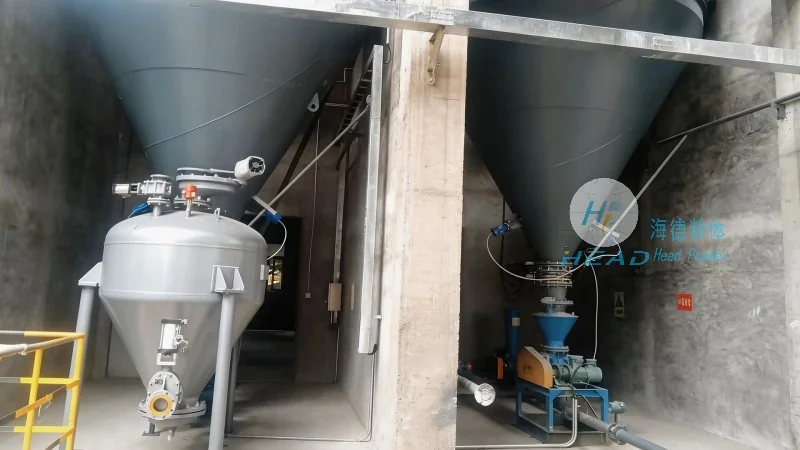
Positive pressure pneumatic conveying systems, on the other hand, operate by generating positive pressure at the discharge end of the conveying line. This method uses a blower or a positive pressure pump to push the material through the system, rather than pulling it as in vacuum systems. The primary components of a positive pressure system include a hopper, a rotary valve, a positive pressure blower, and a discharge unit. The hopper and rotary valve function similarly to those in vacuum systems, but the positive pressure blower provides the necessary force to move the coke powder through the line. The discharge unit then releases the material at the desired location.
Positive pressure systems are often preferred in applications where the material is sensitive to moisture or where the conveying distance is short. They are particularly effective for transporting coke powder in environments where dust control is critical, as the system operates under positive pressure, preventing external air from entering the line and contaminating the material. This feature makes positive pressure systems ideal for applications in food processing, pharmaceuticals, and other industries where product purity is paramount. Furthermore, these systems are capable of handling high volumes of material at high speeds, making them suitable for large-scale production facilities.
Comparative Analysis: Vacuum vs. Positive Pressure Conveying for Flexible Coke Powder
When selecting between vacuum and positive pressure pneumatic conveying systems for flexible coke powder, several factors must be considered. The choice depends on the specific application requirements, such as the distance of transport, the layout of the facility, the material properties, and the environmental considerations. Vacuum systems are generally more suitable for long-distance and complex layouts due to their ability to handle materials over extended distances with minimal pressure loss. They are also more cost-effective for applications where the material is not highly sensitive to moisture or contamination. In contrast, positive pressure systems excel in short-distance and high-volume applications, particularly where product purity and dust control are critical.
The operational costs of vacuum systems are typically lower due to the lower energy consumption of vacuum pumps compared to positive pressure blowers. However, the initial investment for vacuum systems may be higher due to the need for a more complex filter system and additional components. Positive pressure systems, while potentially more expensive to operate, offer advantages in terms of material handling efficiency and product quality, especially in industries where the material must remain dry and free from contaminants.
Applications and Benefits of Flexible Coke Powder Pneumatic Conveying
The application of flexible coke powder pneumatic conveying technology spans across various industries, including steel production, chemical manufacturing, and food processing. In steel production, coke powder is used as a fuel in blast furnaces, and efficient transport is crucial for maintaining production schedules and minimizing material loss. The use of pneumatic conveying systems ensures that coke powder is delivered to the furnaces in a consistent and controlled manner, improving overall operational efficiency.
In chemical manufacturing, coke powder is used as a raw material in the production of various chemicals, and the ability to transport it efficiently is essential for maintaining production continuity. Pneumatic conveying systems allow for the seamless transfer of coke powder from storage to processing units, reducing the risk of material handling errors and improving product quality.
In the food processing industry, the use of positive pressure pneumatic conveying systems is particularly beneficial due to the stringent requirements for product purity and hygiene. These systems ensure that coke powder, which may be used as a flavoring agent or a processing aid, is transported without contamination, meeting the highest standards of food safety.
Technological Advancements and Future Trends in Pneumatic Conveying
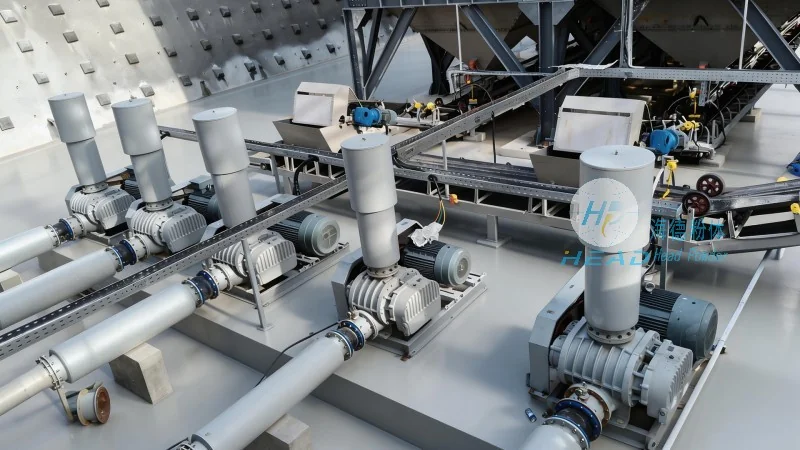
As technology advances, the field of pneumatic conveying continues to evolve, with new innovations aimed at improving efficiency, reducing costs, and enhancing safety. Modern vacuum and positive pressure systems now incorporate advanced control systems, allowing for real-time monitoring and adjustment of conveying parameters. This enables operators to optimize the system performance based on changing conditions, such as material flow rates or pressure levels.
Another trend is the integration of automation and robotics in material handling processes. Automated feeding systems and conveyor controls can be integrated with pneumatic conveying equipment to create a fully automated material transport solution. This not only improves operational efficiency but also reduces the risk of human error and enhances workplace safety.
Furthermore, the development of more energy-efficient components, such as high-efficiency vacuum pumps and blowers, is reducing the operational costs of pneumatic conveying systems. These advancements are making the technology more accessible to a wider range of industries, including small and medium-sized enterprises.
Conclusion: Choosing the Right Pneumatic Conveying Solution for Flexible Coke Powder
Both vacuum and positive pressure pneumatic conveying systems offer effective solutions for the transport of flexible coke powder, each with its own set of advantages and limitations. The choice between the two depends on the specific requirements of the application, including the distance of transport, the material properties, and the environmental considerations. By understanding the operational principles and benefits of each system, industries can select the most suitable pneumatic conveying solution to meet their needs and improve overall operational efficiency.
HeadPowder Engineering Co., Ltd., with its expertise in designing and implementing customized pneumatic conveying systems, is well-positioned to assist industries in selecting and implementing the right technology for their flexible coke powder transport needs. The company's commitment to innovation and customer satisfaction ensures that clients receive tailored solutions that enhance their operational efficiency and product quality.




