HeadPowder, a leading provider in the field of pneumatic conveying systems, specializes in advanced solutions tailored for the efficient handling of peanut kernels. This article delves into the core technologies of vacuum and positive pressure pneumatic conveying, offering a comprehensive understanding of their principles, advantages, and practical applications in the industry.
Vacuum Pneumatic Conveying Systems for Peanut Kernels
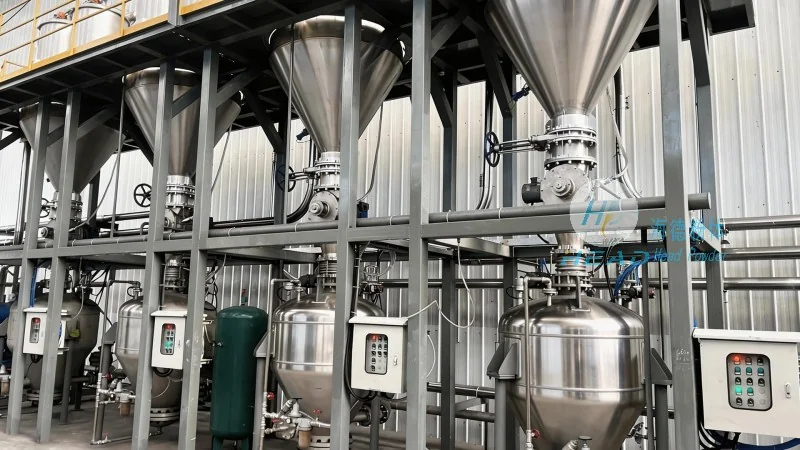
Vacuum pneumatic conveying systems utilize a negative pressure environment to draw material from a source to a destination. In the context of peanut kernels, this method is particularly effective for transporting materials over moderate distances, often within processing facilities or between storage and processing areas. The system operates by creating a vacuum at the inlet, which pulls the peanut kernels through a pipeline using air flow. This approach is known for its ability to handle a wide range of particle sizes and densities, making it suitable for various peanut kernel processing stages, such as from raw storage to cleaning and grading.
Key advantages of vacuum systems include gentle material handling, which minimizes product damage and preserves the quality of peanut kernels. The enclosed pipeline design also reduces dust and contamination risks, ensuring that the product remains clean and free from external pollutants. Additionally, vacuum systems can be integrated with dust collection and filtration systems, enhancing overall operational safety and compliance with environmental regulations. HeadPowder's vacuum conveying solutions are engineered to optimize these benefits, providing reliable and efficient transport for peanut kernels while maintaining product integrity.
Positive Pressure Pneumatic Conveying Systems for Peanut Kernels
Conversely, positive pressure systems operate by generating a positive pressure at the source, pushing material through the pipeline. This method is ideal for longer transport distances and for applications requiring higher material throughput. In peanut kernel handling, positive pressure systems are commonly used for moving large volumes of material from storage silos to processing lines or for transporting finished products to packaging areas. The system works by forcing air and material through the pipeline, ensuring consistent flow and preventing blockages that can occur in vacuum systems under certain conditions.
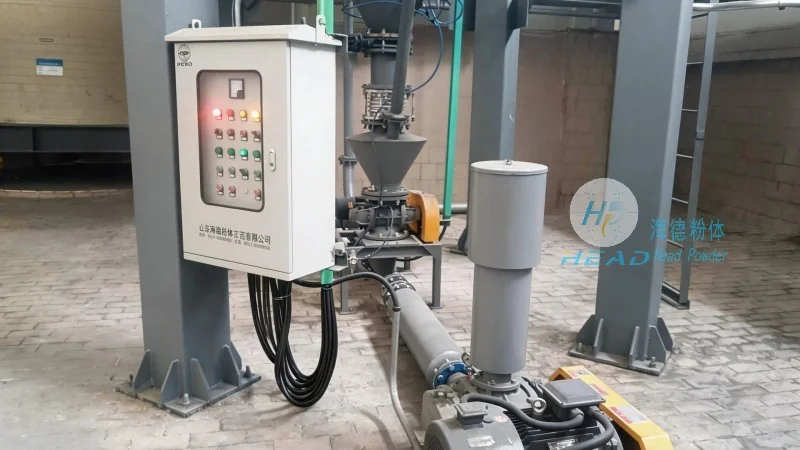
Positive pressure systems offer several benefits, including higher conveying rates and the ability to handle abrasive or sticky materials without excessive wear on components. The positive pressure environment also helps in maintaining product temperature and preventing moisture loss, which is crucial for maintaining the quality of peanut kernels during transport. HeadPowder's positive pressure conveying solutions are designed with robust components, such as high-quality valves and filters, to withstand the demands of continuous operation and ensure long-term reliability. These systems are particularly effective for large-scale operations where efficiency and throughput are critical factors.
Comparative Analysis: Vacuum vs. Positive Pressure Conveying
When selecting a pneumatic conveying system for peanut kernels, it is essential to consider the specific requirements of the application. A comparative analysis of vacuum and positive pressure systems reveals distinct advantages and limitations. Vacuum systems excel in handling delicate materials and over shorter distances, while positive pressure systems are better suited for high-volume, long-distance transport. The choice between the two often depends on factors such as the distance between the source and destination, the volume of material to be transported, and the need for product protection.
HeadPowder's expertise lies in customizing pneumatic conveying solutions to meet these specific needs. By evaluating the operational parameters and material characteristics, the company can recommend the most appropriate system configuration. For instance, a facility processing a large quantity of peanut kernels over a long distance might benefit from a combination of both vacuum and positive pressure components, such as a vacuum pickup system followed by a positive pressure booster to enhance efficiency. This hybrid approach allows for optimized material flow and reduced energy consumption, aligning with modern industrial standards.
Applications and Industry Impact
The application of pneumatic conveying technology in peanut kernel processing has significantly improved operational efficiency and product quality. Vacuum systems are widely used in the initial stages of processing, such as material intake and cleaning, where gentle handling is essential to prevent damage to the kernels. Positive pressure systems, on the other hand, are commonly employed in downstream processes, including packaging and distribution, where high throughput and consistent flow are required.
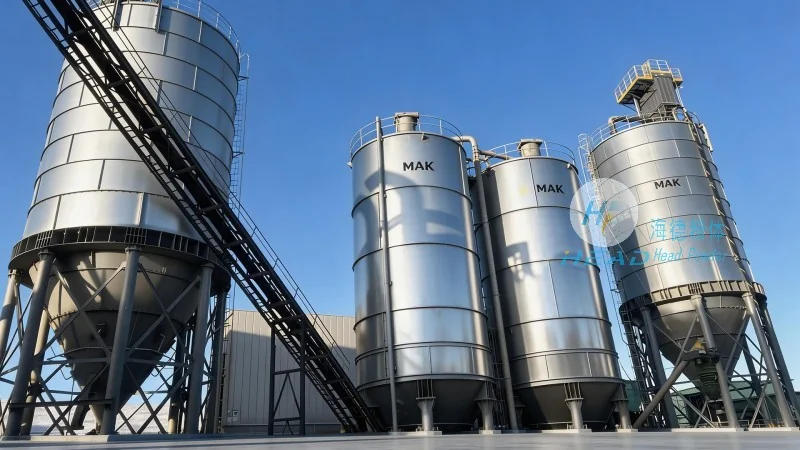
HeadPowder's pneumatic conveying solutions have been implemented in numerous peanut processing facilities across China, including Shandong, where the company is headquartered. The company's commitment to quality and innovation has enabled it to deliver systems that meet the stringent requirements of the food processing industry. By leveraging advanced engineering and materials, HeadPowder ensures that its conveying systems are not only efficient but also compliant with food safety regulations, providing peace of mind to clients operating in the peanut kernel sector.
Conclusion and Future Directions
In conclusion, the integration of vacuum and positive pressure pneumatic conveying systems represents a significant advancement in the handling of peanut kernels. These technologies offer tailored solutions that address the unique challenges of material transport in the food processing industry. HeadPowder, with its extensive experience and expertise, continues to lead the way in developing and implementing advanced pneumatic conveying systems that enhance operational efficiency, product quality, and overall profitability for its clients.
As the demand for efficient and reliable material handling solutions grows, HeadPowder remains dedicated to innovation and customer satisfaction. By staying at the forefront of technological advancements, the company ensures that its pneumatic conveying systems remain the preferred choice for peanut kernel processing facilities worldwide. The future of pneumatic conveying in the food industry is bright, and HeadPowder is poised to play a key role in shaping this evolution.




