Efficient material handling is a critical factor in the fertilizer industry, where the seamless transport of granular and powdered substances directly impacts production efficiency and operational costs. Pneumatic conveying systems have emerged as a sophisticated solution for moving these materials with precision and reliability. This article explores the technology behind pneumatic conveying, focusing on how it enables the efficient transport of fertilizer granules and other similar powders.
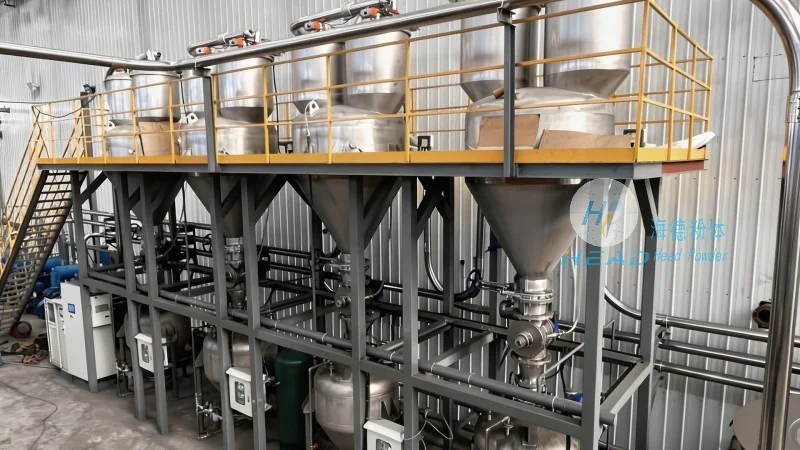
Understanding Pneumatic Conveying Systems for Fertilizer Transport
Pneumatic conveying utilizes air flow to transport bulk materials through a pipeline system. Unlike traditional mechanical conveying methods, such as screw conveyors or belt conveyors, pneumatic systems offer advantages like reduced equipment wear, lower maintenance requirements, and the ability to handle a wide range of particle sizes and moisture contents. The core components of a pneumatic conveying system include a material feed hopper, a conveying line, a dust collector, and a discharge outlet. The system operates by creating a pressure differential, either through suction (negative pressure) or pressure (positive pressure), to move the material along the pipeline.
Key Benefits of Pneumatic Conveying for Fertilizer Granules
For fertilizer manufacturers, pneumatic conveying offers several key benefits that enhance operational performance. First, it minimizes product degradation by avoiding direct contact with mechanical parts, which is particularly important for sensitive fertilizers that can be affected by friction or heat. Second, the system provides a hygienic and dust-free environment, reducing the risk of contamination and improving safety in the workplace. Third, pneumatic conveying allows for flexible layout designs, as the pipeline can be installed in various configurations to suit the plant layout, and can even transport materials over long distances without the need for intermediate storage or transfer points.
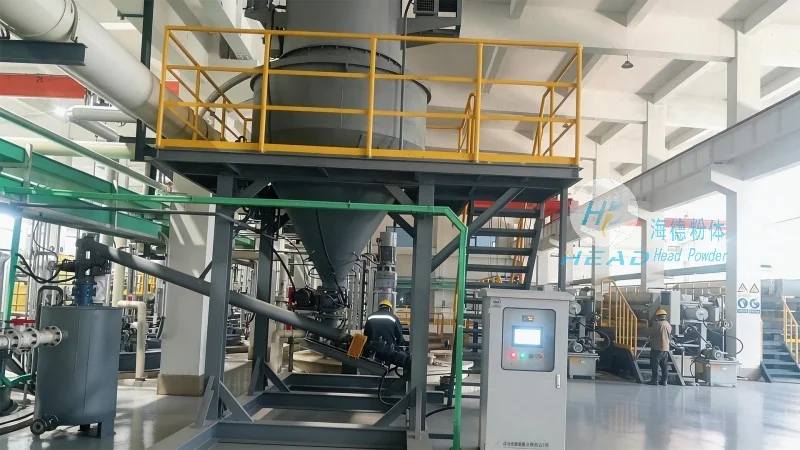
How Shandong HeadPowder Engineering Co., Ltd. Specializes in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the unique needs of the fertilizer industry. With years of experience in the field, the company has developed a deep understanding of the challenges faced by fertilizer producers, including material variability, process efficiency, and safety standards. HeadPowder engineers work closely with clients to assess their specific requirements, such as the type of fertilizer (e.g., nitrogen, phosphorus, potassium, or specialty blends), the required conveying capacity, and the distance to be covered. Based on this analysis, they design systems that optimize performance while minimizing energy consumption and operational costs.
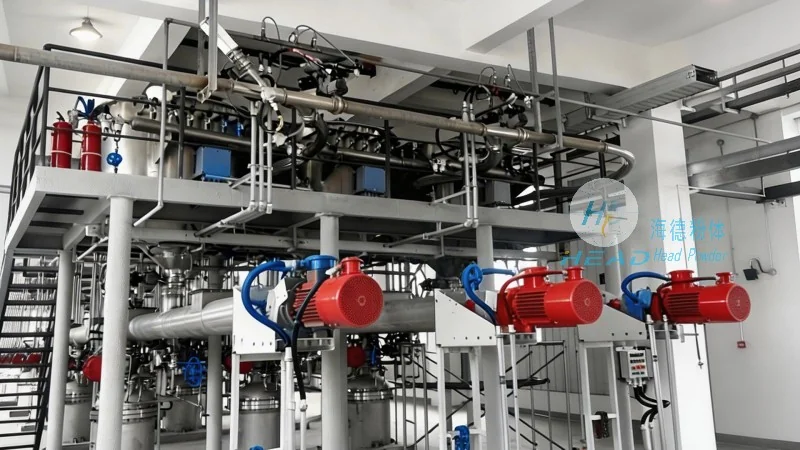
Customization and Innovation in Pneumatic Conveying Technology
HeadPowder Engineering Co., Ltd. takes pride in its commitment to innovation and customization. The company offers a range of pneumatic conveying technologies, including dilute phase and dense phase systems, to suit different material characteristics and application scenarios. Dilute phase systems are ideal for transporting fine powders over short to medium distances, while dense phase systems are more suitable for handling bulk granules over longer distances with higher pressure. Additionally, the company integrates advanced control systems and monitoring tools into its designs, enabling real-time tracking of material flow, pressure, and temperature. This allows for proactive maintenance and ensures optimal system performance. The engineering team at HeadPowder also considers factors such as material abrasiveness, moisture content, and potential dust explosion risks when designing the system, ensuring compliance with industry safety standards.
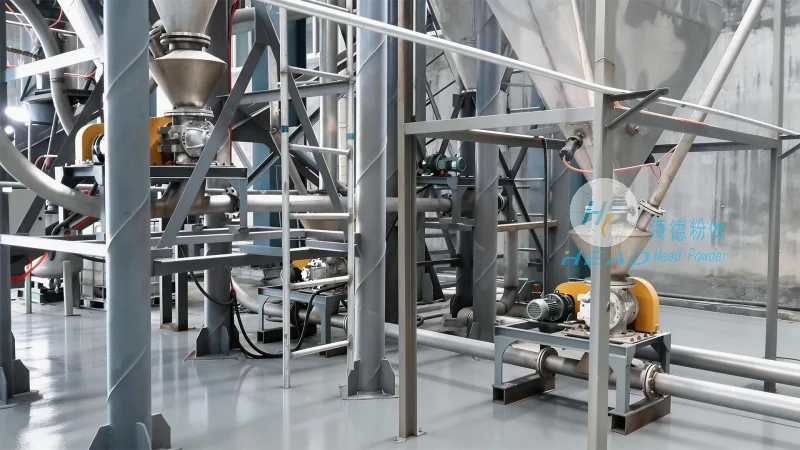
Installation and Maintenance of Pneumatic Conveying Systems
The successful implementation of a pneumatic conveying system requires careful planning and professional installation. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive installation services, including site assessment, system layout design, and on-site assembly. The company’s technicians are trained to handle the complexities of pneumatic systems, ensuring that all components are properly aligned and connected to achieve the desired performance. Regular maintenance is also crucial to prolong the lifespan of the system and prevent downtime. HeadPowder offers maintenance services, including routine inspections, component replacement, and system tuning, to keep the equipment in optimal condition. By partnering with HeadPowder, fertilizer manufacturers can rely on a reliable partner for both the initial installation and long-term maintenance of their pneumatic conveying systems.
Conclusion: Enhancing Efficiency with Pneumatic Conveying
Pneumatic conveying has revolutionized the way fertilizer granules and powders are transported, offering a more efficient, reliable, and cost-effective solution compared to traditional methods. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in this technology, providing customized solutions that meet the specific needs of the fertilizer industry. By leveraging advanced engineering and a customer-centric approach, HeadPowder helps fertilizer producers improve their operational efficiency, reduce costs, and ensure the safe and hygienic handling of their products. For those seeking to enhance their material handling capabilities, pneumatic conveying with HeadPowder Engineering Co., Ltd. is a smart investment in long-term productivity and success.




