HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust-free bulk material feeding solutions. Our product line includes the dust-free bulk material feeding station with pneumatic conveying system designed for small bag handling. This system is engineered to ensure efficient, clean, and safe material transfer in various industrial applications.
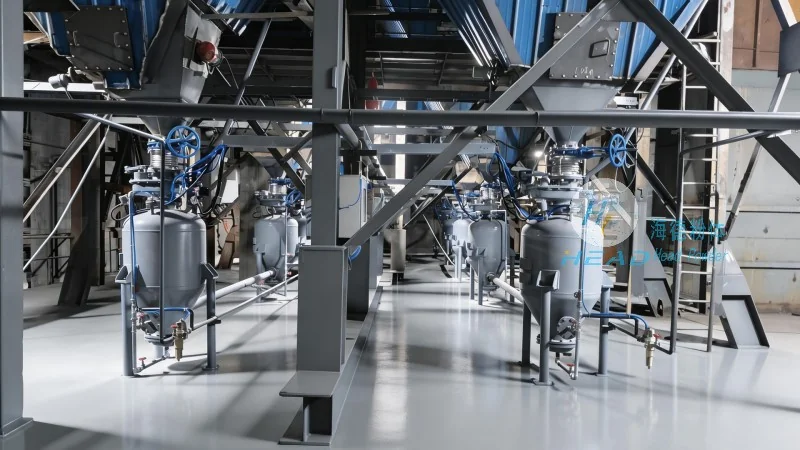
Overview of the Dust-Free Bulk Material Feeding Station with Pneumatic Conveying System
The dust-free bulk material feeding station is a critical component in modern material handling systems, particularly for industries dealing with powders, granules, and other bulk materials. The system is designed to minimize dust emissions, enhance operational safety, and improve overall efficiency. HeadPowder's solution integrates advanced technology and robust construction to meet the demanding requirements of contemporary manufacturing environments.
Key Components and Their Functions
The system comprises several key components, each playing a vital role in the material transfer process. These include the small bag hopper, pneumatic conveying ducts, dust collection filters, and control panels. The small bag hopper is designed to hold and store bulk materials from small bags, while the pneumatic conveying system uses compressed air to transport the material from the hopper to the processing equipment. The dust collection filters are essential for maintaining a clean working environment by capturing and removing airborne particles. The control panels allow operators to monitor and adjust the system's performance in real-time.
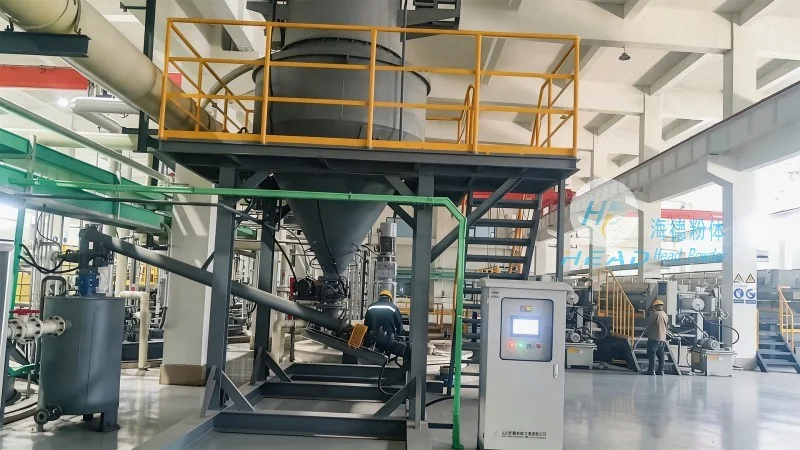
Operation Process: Step-by-Step Execution
The operation of the dust-free bulk material feeding station with pneumatic conveying system follows a systematic process to ensure smooth and continuous material transfer. First, small bags of bulk material are placed into the hopper. The system then uses an integrated feeder to open the bags and discharge the material into the hopper. Next, the pneumatic conveying system activates, and compressed air is introduced into the conveying ducts. This creates a pressure differential that propels the material through the ducts to the target destination, such as a mixer, reactor, or storage silo. The process is automated, allowing for consistent and reliable material flow without manual intervention. The system also includes safety features, such as pressure relief valves and emergency stop buttons, to prevent accidents and ensure operator safety.
Working Principle: How the System Transfers Materials
The working principle of the pneumatic conveying system is based on the movement of material particles using compressed air. When the system is activated, compressed air is introduced into the conveying ducts, creating a high-pressure environment. The material from the hopper is drawn into the ducts by the pressure differential, and the air flow carries the particles through the system. The system uses a combination of positive and negative pressure to transport materials over varying distances and elevations. The dust collection filters are strategically placed to capture any airborne particles, ensuring that the material is transferred in a clean and dust-free manner. The control system monitors the pressure, flow rate, and other parameters to maintain optimal performance and prevent blockages or other issues.
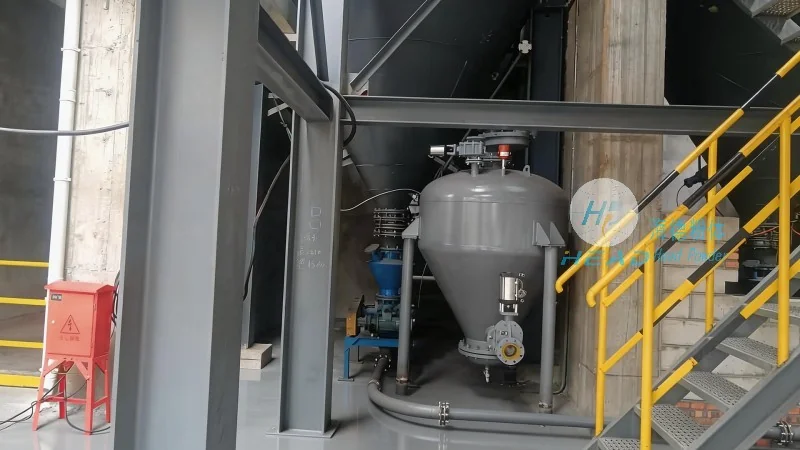
Benefits and Applications
HeadPowder's dust-free bulk material feeding station with pneumatic conveying system offers numerous benefits for industrial applications. The system minimizes dust emissions, reducing the risk of respiratory issues and contamination in the workplace. It also improves operational efficiency by automating the material transfer process, reducing labor costs and increasing production throughput. The system is suitable for a wide range of materials, including powders, granules, and fine particles, and can be customized to meet specific application requirements. Industries such as pharmaceuticals, food processing, chemicals, and plastics benefit from this technology, as it enhances product quality and safety while maintaining compliance with environmental regulations.
Conclusion
HeadPowder's dust-free bulk material feeding station with pneumatic conveying system is a reliable and efficient solution for handling small bag bulk materials. The system's advanced design and robust construction ensure long-term performance and minimal maintenance. By integrating dust collection and automation features, the system provides a clean, safe, and productive environment for material handling operations. HeadPowder, with its headquarters in Shandong, China, continues to innovate and provide high-quality solutions to meet the evolving needs of the industrial sector.




