Understanding the working principle and characteristics of pneumatic material transport systems is crucial for optimizing the handling of fly ash in industrial applications. This article provides a detailed overview of how such systems operate and their key attributes, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field based in China.
Working Principle of Pneumatic Material Transport from Fly Ash Silos
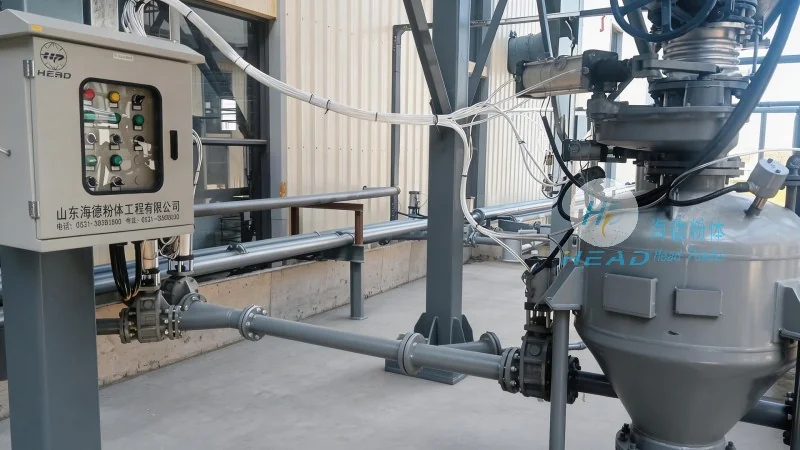
Pneumatic material transport from fly ash silos relies on the fundamental principle of using air flow to move bulk materials. The process typically involves several key components working in concert to ensure efficient and reliable material transfer. At the core of the system is the fly ash silo, which serves as the storage vessel for the material. From the silo, a pipeline network is connected, leading to a pneumatic conveying unit. This unit may utilize either positive pressure (air blowing) or negative pressure (air suction) to create the necessary air flow. In positive pressure systems, a blower or compressor generates compressed air that is introduced into the pipeline, pushing the fly ash particles forward. The air flow carries the material through the pipeline, often with the assistance of special devices like airlocks or rotary valves at the silo outlet to control the flow rate and prevent backflow. The material is then discharged at the receiving end, where a separator or filter may be used to separate the material from the air, allowing the air to be recirculated or vented. Negative pressure systems, on the other hand, use a vacuum pump to create a low-pressure environment that draws the material from the silo into the pipeline. Both methods aim to achieve a consistent and controlled flow of fly ash, minimizing the risk of blockages and ensuring smooth operation.
Key Characteristics of Pneumatic Material Transport Systems
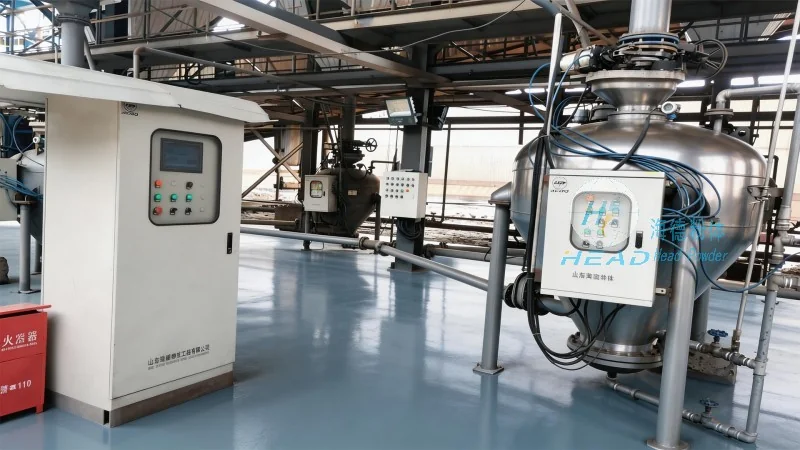
The characteristics of pneumatic material transport systems for fly ash handling are designed to address the specific challenges of this application. One of the most significant advantages is the ability to handle fine, dry materials like fly ash without the need for mechanical conveying equipment, which can be prone to wear and maintenance issues. The system's efficiency is highlighted by its ability to transport materials over long distances with minimal energy consumption compared to other methods like belt conveyors or trucks. Additionally, pneumatic transport offers a high degree of flexibility, as the pipeline layout can be easily adjusted to accommodate changes in plant layout or operational needs. Environmental considerations are also a key characteristic, as the enclosed system prevents dust emissions, reducing the risk of air pollution and ensuring compliance with environmental regulations. Automation is another important feature, with many systems incorporating sensors and control mechanisms to monitor flow rates, pressure, and material levels, allowing for real-time adjustments and reducing the need for manual intervention. The durability and reliability of the components, such as the blower, pipeline, and separation equipment, are also critical characteristics, as they must withstand the abrasive nature of fly ash and operate continuously without frequent breakdowns. Overall, these characteristics make pneumatic material transport an effective and sustainable solution for fly ash handling in power plants and other industrial facilities.
Application and Benefits in Industrial Settings
In industrial settings, the application of pneumatic material transport from fly ash silos offers numerous benefits that enhance operational efficiency and safety. The system's ability to handle large volumes of fly ash in a continuous manner supports the smooth operation of downstream processes, such as fly ash utilization or disposal. By eliminating the need for manual handling or external transport vehicles, the system reduces labor costs and improves workplace safety by minimizing exposure to dust and potential hazards. The enclosed nature of the system also contributes to better environmental management, as it prevents dust from being released into the atmosphere, which is particularly important in regions with strict air quality standards. Furthermore, the system's scalability allows it to be adapted to different plant sizes and capacities, making it suitable for both small-scale and large-scale industrial applications. The integration of advanced control systems enables operators to monitor and manage the transport process remotely, improving overall plant management and reducing downtime. The long-term cost-effectiveness of pneumatic transport, when compared to traditional methods, is also a significant benefit, as it reduces maintenance and operational costs over the system's lifespan. These benefits collectively make pneumatic material transport an attractive option for industries seeking to optimize their fly ash handling operations.
Conclusion and Company Overview
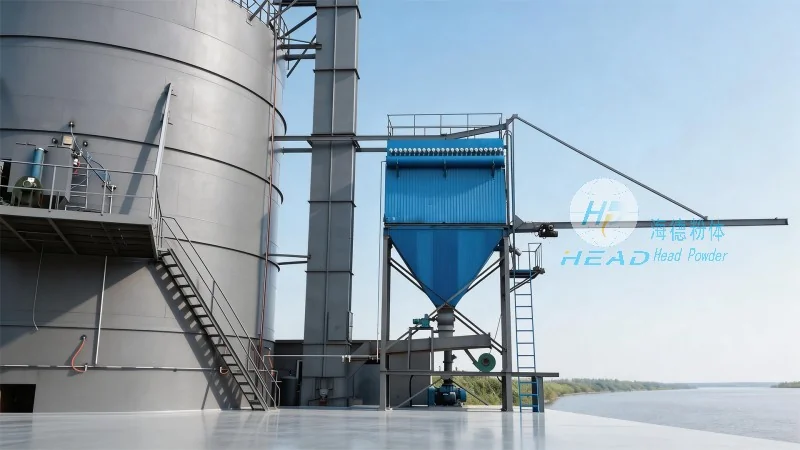
Summarizing, the working principle and characteristics of pneumatic material transport from fly ash silos provide a robust and efficient solution for handling bulk materials in industrial environments. The system's reliance on air flow to move material, combined with its key attributes such as efficiency, flexibility, and environmental friendliness, makes it a preferred choice for many facilities. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, offers comprehensive solutions tailored to the specific needs of clients. Based in China, the company leverages advanced technology and industry experience to deliver high-quality pneumatic transport systems that meet the demands of modern industrial operations. By understanding the working principle and characteristics of these systems, industries can make informed decisions to enhance their material handling processes and achieve operational excellence.




