When it comes to transporting silicate materials, selecting the right method is crucial for efficiency, cost-effectiveness, and operational safety. Silicates, such as kaolin, talc, and other mineral powders, present unique challenges due to their fine particle size, hygroscopic nature, and potential for dust generation. Traditional methods like belt conveyors or bucket elevators may struggle with these characteristics, leading to material degradation, increased maintenance, and environmental concerns. This article explores the various silicate transport methods available and highlights the advantages of pneumatic conveying systems, with a focus on the solutions offered by Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder.
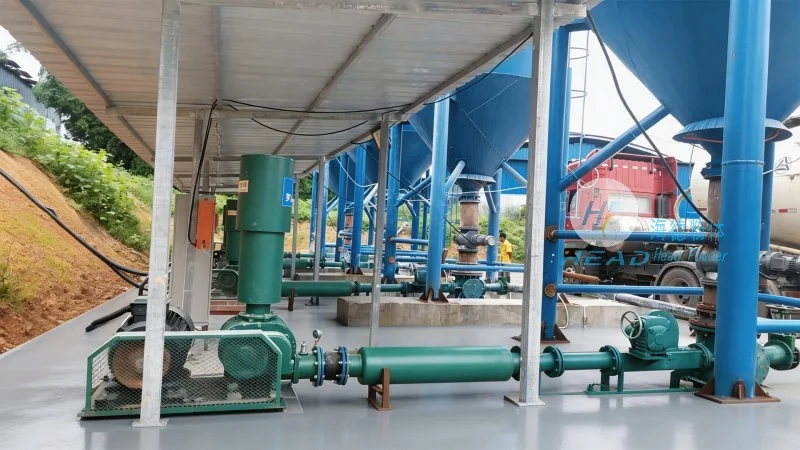
Understanding Silicate Material Properties and Conveying Challenges
Silicate materials are widely used in industries like ceramics, paints, plastics, and pharmaceuticals due to their excellent thermal stability and chemical inertness. However, their fine particle size (often in the micrometer range) and tendency to stick together or agglomerate make conventional bulk handling equipment less effective. Traditional mechanical conveyors can cause excessive wear and tear, leading to higher maintenance costs and downtime. Additionally, the hygroscopic nature of many silicates means they can absorb moisture from the air, affecting product quality and processing performance. Dust control is another critical issue, as fine silicate powders are hazardous when inhaled and can create environmental liabilities. These challenges necessitate specialized transport solutions that address the unique properties of silicate materials.
Overview of Common Silicate Conveying Methods
Several methods are commonly used for silicate material transport, each with its own set of advantages and limitations. The most prevalent include:
Belt Conveyors: These are widely used for bulk material handling but are less suitable for fine silicates. The high friction and potential for material buildup on belts can lead to uneven flow and increased wear. Belt conveyors also require significant space and may not effectively handle hygroscopic materials without additional moisture control measures.
Bucket Elevators: Vertical transport systems that use buckets to lift materials. While effective for vertical movement, bucket elevators can cause particle degradation due to impact and friction. They are also prone to material sticking, especially with cohesive silicates, leading to blockages and operational disruptions.
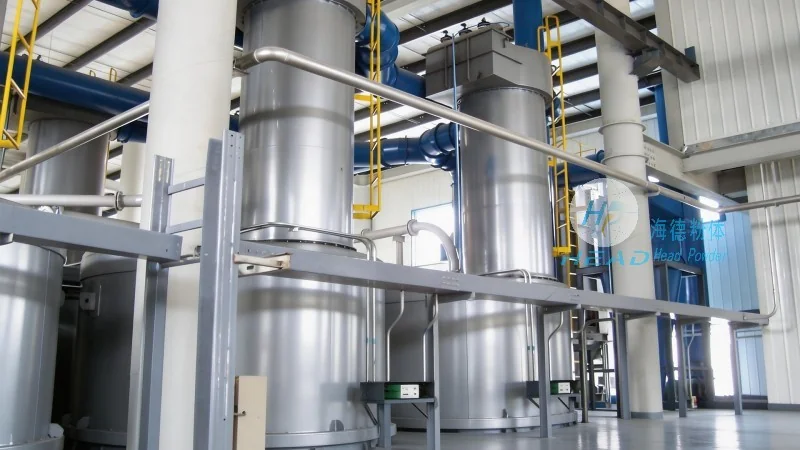
Pneumatic Conveying: This method uses air or gas to transport materials through a pipeline. It offers several advantages for silicates, including gentle handling, minimal material degradation, and effective dust control. Pneumatic systems can be designed to handle fine powders and hygroscopic materials while reducing the risk of contamination and environmental exposure.
HeadPowder's Silicate Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) specializes in providing advanced pneumatic conveying systems tailored to the needs of silicate industries. With headquarters in Shandong, China, HeadPowder leverages decades of experience in bulk material handling to develop customized solutions that address the unique challenges of silicate transport. The company's approach focuses on integrating technology, engineering expertise, and customer-centric design to deliver efficient, reliable, and cost-effective conveying systems.
HeadPowder's silicate pneumatic conveying systems are engineered to handle a wide range of silicate materials, including kaolin, talc, silica, and other mineral powders. The systems are designed with features such as:
Low-Pressure Pneumatic Conveying: Ideal for short-distance transport and handling of low to medium density materials. This method uses moderate air pressure to move materials through pipelines, reducing energy consumption and equipment complexity. Low-pressure systems are particularly effective for transporting fine silicates without causing excessive particle breakage.
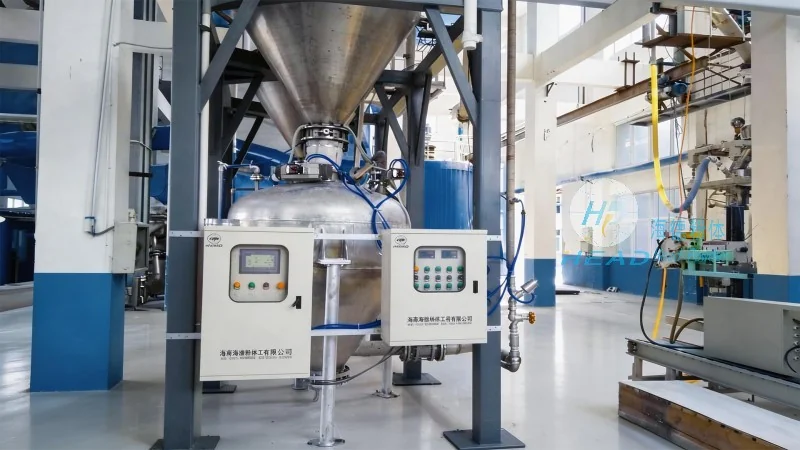
High-Pressure Pneumatic Conveying: Suitable for longer distances and higher material throughput. High-pressure systems use higher air pressure to achieve greater transport efficiency, making them ideal for large-scale industrial applications. These systems are designed to maintain material integrity and minimize pressure losses over longer pipeline runs.
Closed Loop Systems: A key feature of HeadPowder's solutions is the use of closed-loop pneumatic conveying, which recirculates air to maintain consistent pressure and reduce energy waste. This design enhances system efficiency and ensures stable material flow, even with hygroscopic silicates that may vary in moisture content.
Customized Design and Integration: HeadPowder works closely with clients to understand their specific operational requirements, such as material flow rates, pipeline layout, and environmental constraints. The company provides comprehensive engineering services, including system design, installation, and commissioning, to ensure that the conveying solution is optimized for the client's unique needs. This approach minimizes downtime during implementation and maximizes the system's performance from the start.
Advantages of HeadPowder's Silicate Pneumatic Conveying Systems
Implementing HeadPowder's pneumatic conveying systems offers several significant benefits for silicate handling operations:
Enhanced Material Integrity: The gentle handling of pneumatic systems minimizes particle degradation, ensuring that the silicate material retains its original properties. This is critical for applications where material quality directly impacts product performance, such as in ceramics or pharmaceuticals.
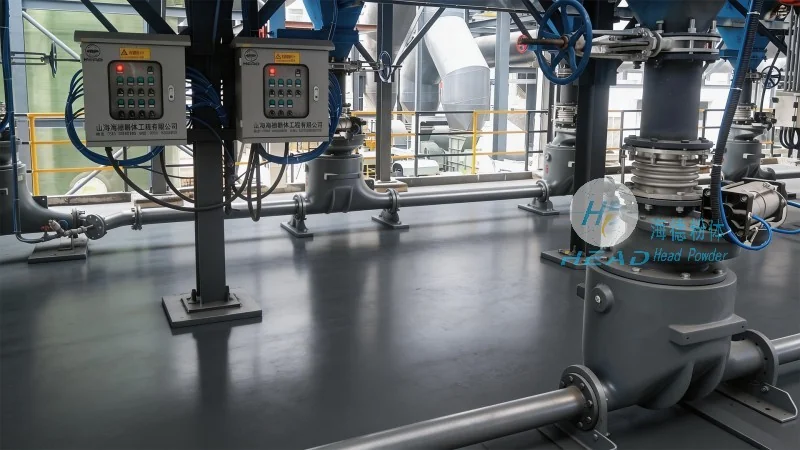
Improved Efficiency and Cost Savings: By reducing material loss, maintenance costs, and downtime, pneumatic conveying systems provide long-term cost savings. The closed-loop design of HeadPowder's systems further enhances energy efficiency, lowering operational expenses over time.
Effective Dust Control: Pneumatic systems are inherently dust-tight, preventing the release of fine silicate particles into the environment. This not only reduces environmental liabilities but also improves workplace safety by minimizing inhalation risks for operators.
Flexibility and Scalability: HeadPowder's solutions can be easily scaled to accommodate changes in production volume or material types. The modular design of the systems allows for future expansion without major overhauls, providing a flexible approach to meeting evolving operational needs.
Conclusion
For industries dealing with silicate materials, selecting the right transport method is essential to maintain product quality, operational efficiency, and safety. While traditional methods like belt conveyors and bucket elevators have their place, pneumatic conveying systems offer superior performance for fine, hygroscopic materials. Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) stands out as a leader in providing customized silicate pneumatic conveying solutions that address the unique challenges of silicate handling. With their focus on engineering excellence, customer satisfaction, and sustainable operation, HeadPowder's systems help clients achieve reliable, efficient, and cost-effective material transport, supporting their long-term success in the silicate industry.




