When it comes to the efficient handling and transportation of pearl salt granules, selecting the right conveying method is crucial for maintaining product quality, minimizing operational costs, and ensuring smooth production processes. Pearl salt, a vital ingredient in various industries such as food processing, chemical manufacturing, and pharmaceuticals, requires specialized equipment to handle its granular nature. This article explores the primary methods used for pearl salt granule conveying, highlighting the advantages and applications of each approach.
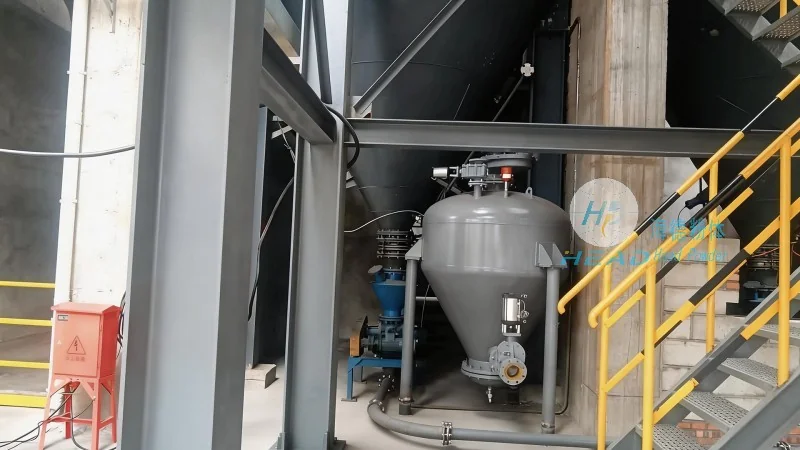
1. Screw Conveyors: A Versatile Solution for Horizontal and Inclined Transport
Screw conveyors, also known as auger conveyors, are among the most common and reliable methods for transporting pearl salt granules. These systems consist of a rotating screw (auger) enclosed in a U-shaped or cylindrical housing. As the screw rotates, it pushes the granules forward, making them suitable for both horizontal and inclined transport. The design allows for gentle handling of the salt, preventing breakage or segregation of particles. Screw conveyors are particularly effective for short to medium distances and can be integrated into existing production lines. They are also easy to install and maintain, making them a cost-effective choice for many applications.
2. Pneumatic Conveying Systems: Ideal for Long-Distance and Dust-Free Transport
Pneumatic conveying systems use air or gas to transport pearl salt granules through a pipeline. This method is highly effective for long-distance transport, as it can move materials over several hundred meters without the need for multiple transfer points. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the granules, while vacuum systems use suction to draw them. Pneumatic conveying offers a dust-free environment, which is essential for maintaining product purity and worker safety. Additionally, these systems can handle varying particle sizes and flow rates, making them adaptable to different production needs. However, they require proper air filtration and moisture control to prevent material degradation.
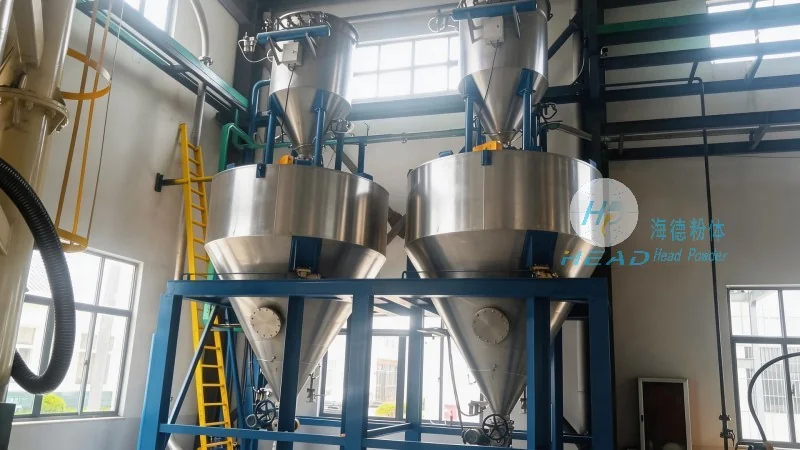
3. Belt Conveyors: High-Capacity and Continuous Transport Solutions
Belt conveyors are another popular choice for pearl salt granule conveying, especially in high-volume operations. These systems consist of a continuous belt that moves over rollers or pulleys, transporting the granules from one point to another. Belt conveyors are capable of handling large quantities of material and can be designed for both horizontal and inclined transport. They are ideal for long-distance applications and can be integrated with other equipment, such as hoppers and feeders, to create a seamless material flow. The design allows for minimal product degradation and is easy to clean, which is important for maintaining hygiene standards in food and pharmaceutical industries. However, belt conveyors require regular maintenance to ensure the belt remains in good condition and to prevent material buildup.
4. Bucket Elevators: Vertical Transport with High Efficiency
For vertical transport of pearl salt granules, bucket elevators are a preferred solution. These systems use a series of buckets attached to a chain or belt, which moves vertically to lift the granules from a lower to a higher level. Bucket elevators are highly efficient and can handle large volumes of material with minimal energy consumption. They are particularly useful in applications where vertical space is limited or when the material needs to be elevated to a significant height. The design ensures that the granules are transported in a controlled manner, preventing spillage or segregation. However, bucket elevators require proper alignment and maintenance to avoid mechanical failures and ensure consistent performance.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field of material handling equipment, specializes in providing customized solutions for pearl salt granule conveying. With years of experience and a commitment to quality, HeadPowder offers a range of conveying systems tailored to the unique needs of each client. The company’s products are designed to meet industry standards and are backed by rigorous testing and quality control. HeadPowder’s team of engineers and technicians work closely with clients to understand their specific requirements and develop optimal conveying solutions. The company’s headquarters is located in Shandong, China, where it maintains state-of-the-art manufacturing facilities and research centers. By leveraging advanced technology and innovative design, HeadPowder ensures that its conveying systems are efficient, reliable, and cost-effective for the transportation of pearl salt granules.
Conclusion: Choosing the Right Conveying Method for Pearl Salt Granules
Selecting the appropriate conveying method for pearl salt granules depends on several factors, including the distance of transport, the volume of material, the required speed, and the specific industry application. Each method has its own advantages and limitations, and the choice should be based on a thorough analysis of the operational requirements. By understanding the characteristics of each conveying system, businesses can optimize their material handling processes, reduce downtime, and improve overall productivity. Whether using screw conveyors, pneumatic systems, belt conveyors, or bucket elevators, the goal is to ensure efficient, safe, and cost-effective transport of pearl salt granules. With the right equipment and expertise, companies can enhance their production efficiency and maintain the quality of their products.




