Efficient and reliable conveying of powdered edible salt is a critical process in the food industry, ensuring consistent quality and safety from production to distribution. This article provides an overview of the structural principles and operational mechanisms behind modern powdered salt conveying systems, highlighting key components and their functions.
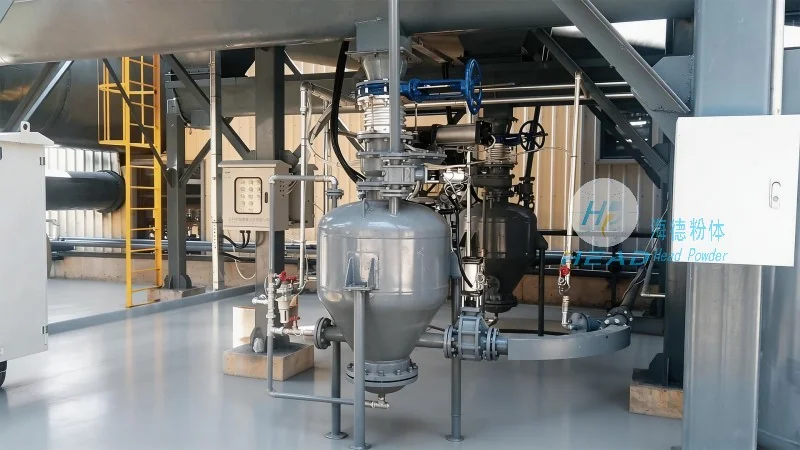
Structural Components of Powdered Edible Salt Conveying Systems
The core of any effective powdered salt conveying system lies in its integrated components, each designed to handle the unique properties of salt powder. Key elements include feed hoppers, which are engineered to store and regulate the flow of salt, preventing clogging and maintaining consistent feed rates. Screw conveyors or pneumatic pipelines are commonly used for transporting the salt, with screw conveyors offering a positive displacement method that ensures reliable movement, especially in environments where air quality is a concern. Pneumatic systems, on the other hand, utilize compressed air to move the salt through pipelines, providing flexibility in layout and the ability to handle longer distances or multiple transfer points.
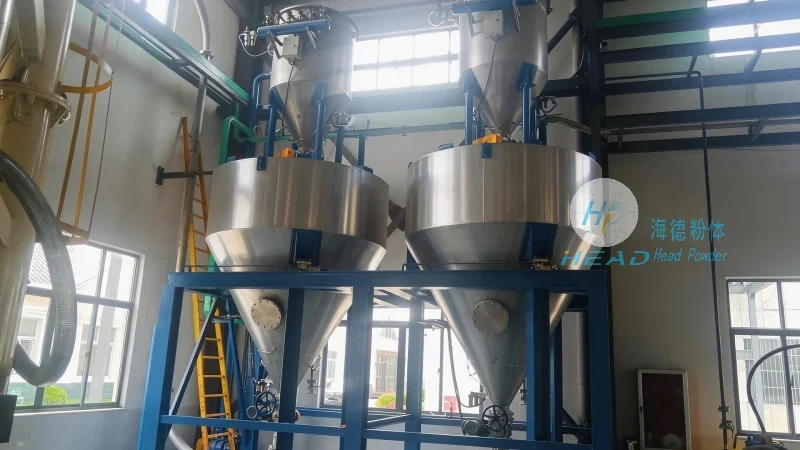
Working Principles and Operational Mechanics
The operational mechanics of powdered salt conveying systems are based on principles of fluidization and mechanical transport. In screw conveyors, the rotating screw (or auger) creates a continuous movement of the salt, pushing it forward through the trough. This method is particularly effective for vertical or inclined transport, as the screw’s design minimizes material degradation and maintains product integrity. Pneumatic conveying systems rely on the creation of a low-pressure zone at the inlet, which draws the salt into the pipeline using air flow. The air-salt mixture is then transported to the destination, where a separator or cyclone separates the salt from the air, allowing for clean and efficient collection.
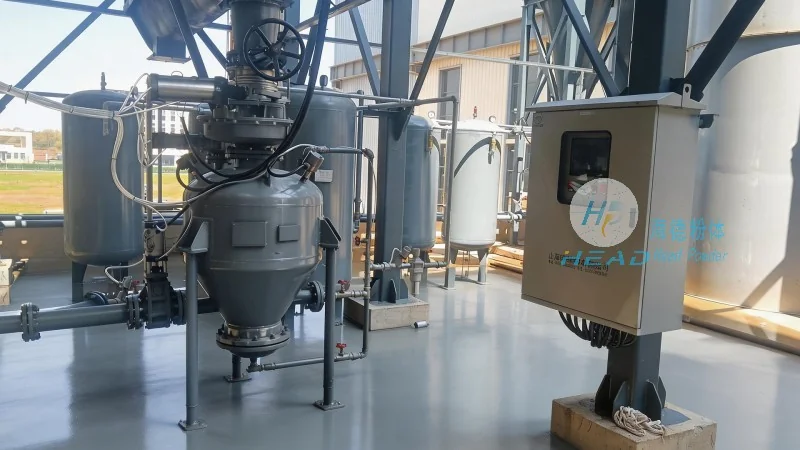
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in powder handling solutions. With a focus on innovation and quality, HeadPowder designs and supplies advanced conveying systems tailored to the specific needs of the food processing industry. HeadPowder’s facilities are located in Shandong, China, where the company leverages local expertise and resources to deliver reliable, efficient, and cost-effective solutions for clients worldwide. The company’s commitment to research and development ensures that its products meet the highest standards of safety and performance, making them a trusted partner for businesses in the edible salt and related industries.
Applications and Industry Relevance
Powdered edible salt conveying systems are widely used in various stages of food production, from raw material handling to packaging. In salt production facilities, these systems facilitate the movement of salt from storage silos to processing lines, ensuring a steady supply for grinding, packaging, and distribution. The ability to handle large volumes of salt efficiently reduces downtime and improves overall operational efficiency. Additionally, the systems are designed to maintain the purity and quality of the salt, which is essential for meeting regulatory standards and consumer expectations. By integrating advanced materials and engineering, HeadPowder’s conveying solutions help food manufacturers achieve consistent product quality and enhance their competitive edge in the market.
Conclusion
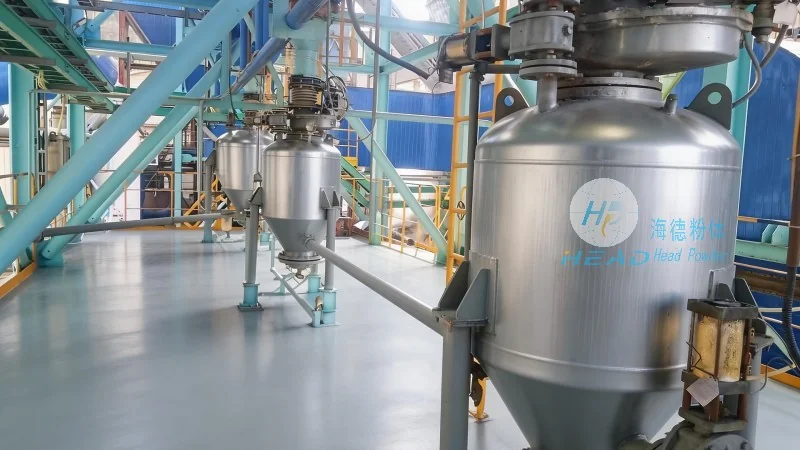
Understanding the structural principles and working mechanisms of powdered edible salt conveying systems is essential for optimizing food processing operations. The combination of reliable components, such as feed hoppers and conveyors, with effective operational mechanics ensures that salt is handled safely and efficiently. Shandong HeadPowder Engineering Co., Ltd. plays a crucial role in providing these advanced solutions, leveraging its expertise to meet the evolving needs of the food industry. As the demand for high-quality edible salt continues to grow, the importance of efficient conveying systems will remain paramount, making HeadPowder a key player in supporting the industry’s success.




