Pyrolytic carbon powder conveying systems are essential in industrial processing for efficiently transporting materials with unique properties. These systems are designed to handle the challenges posed by pyrolytic carbon, including its fine particle size, low bulk density, and tendency to generate static charge. The primary goal of such systems is to ensure reliable and consistent transport of the powder, which is critical for maintaining product quality and operational efficiency across various applications. The structural and operational principles of these conveying systems are tailored to address these specific material characteristics, providing a robust solution for industrial powder handling.
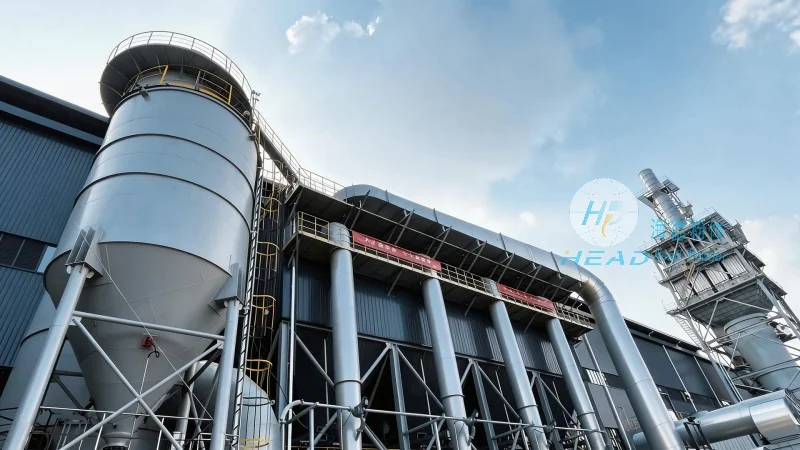
Structural Design and Operational Principles of Pyrolytic Carbon Powder Conveying Systems
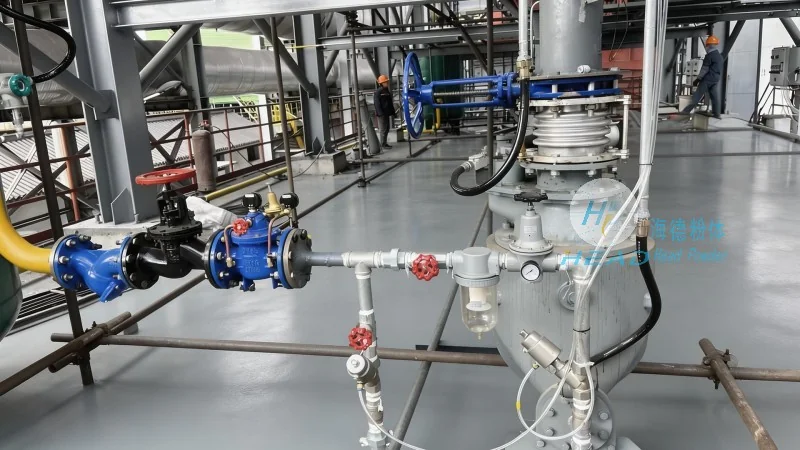
The structural design of pyrolytic carbon powder conveying systems typically includes several key components that work together to facilitate smooth material transport. These components include feed hoppers, conveying pipes, and control mechanisms, each engineered to handle the unique properties of pyrolytic carbon. The feed hopper is designed to store and meter the powder, ensuring a consistent flow rate that prevents clogging and maintains system stability. Conveying pipes, often made from materials resistant to chemical corrosion and wear, are configured to minimize particle degradation and preserve the integrity of the pyrolytic carbon. Control mechanisms, such as variable speed drives and pressure sensors, allow for real-time adjustments to the conveying process, optimizing performance based on operational conditions. Additionally, these systems may incorporate features like static elimination devices and dust collection systems to enhance safety and environmental compliance. Depending on the application, different types of conveying technologies may be employed, including screw conveyors, pneumatic systems, or belt conveyors, each chosen based on factors like material flow rate, distance, and environmental requirements.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of advanced powder handling solutions. The company specializes in the design, manufacturing, and integration of customized conveying systems for specialty powders, with a particular focus on pyrolytic carbon. Headpowder leverages years of industry experience and state-of-the-art technology to deliver high-quality products that meet the specific needs of clients. The company's facilities are located in Shandong, China, where they maintain rigorous quality control processes and technical expertise to ensure that their products are reliable, efficient, and tailored to enhance operational performance. Headpowder's commitment to innovation and customer satisfaction has established them as a trusted partner in the industrial powder handling sector.
Advantages of Pyrolytic Carbon Powder Conveying Systems
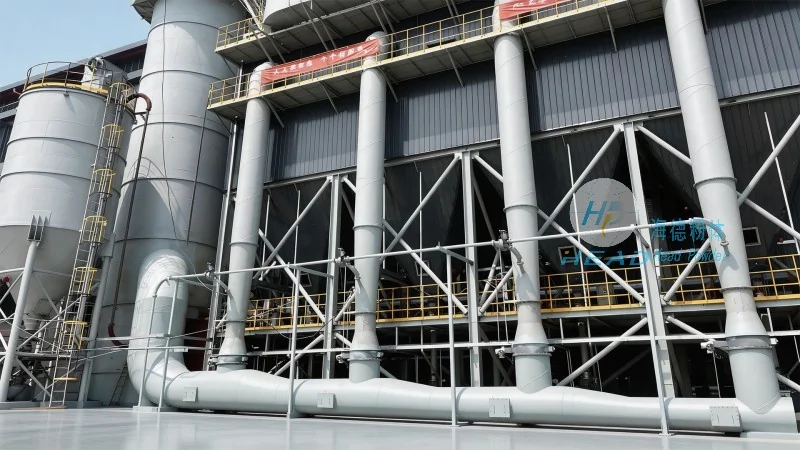
Pyrolytic carbon powder conveying systems offer several key advantages that make them indispensable in industrial applications. These systems are engineered to minimize material loss and contamination, which is crucial for maintaining the purity of pyrolytic carbon—a material often used in high-value applications such as medical devices, aerospace components, and specialty chemicals. The systems also enhance safety by incorporating static control measures and explosion-proof designs, reducing the risk of dust-related hazards. Furthermore, the efficient design of these conveying systems improves overall productivity by reducing downtime and maintenance requirements, leading to significant cost savings for industrial operations. By optimizing the transport process, these systems ensure that pyrolytic carbon is handled with precision, preserving its properties and extending its usability in various industrial processes.




