For industrial applications involving the handling of soap granules, efficient and reliable material transport is crucial. The pneumatic conveying system, particularly designed for soap granules, offers a solution that combines performance with operational simplicity. This article delves into the operation process and working principle of such a system, highlighting the key components and the systematic approach to material movement within industrial settings.
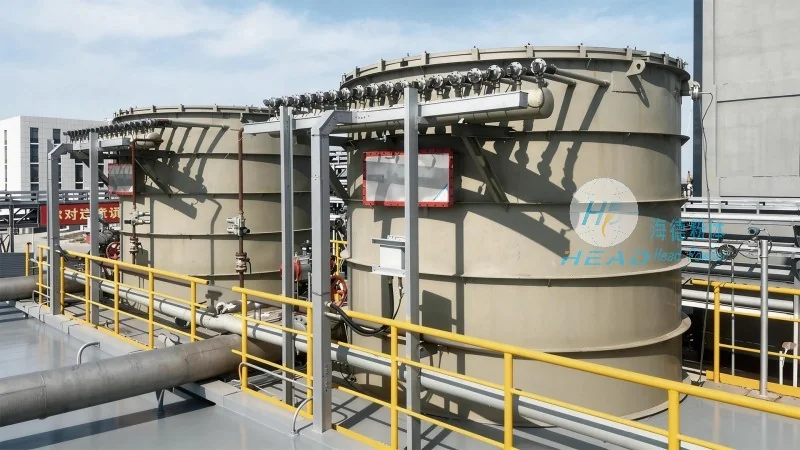
Key Components of the Soap Granule Pneumatic Conveying System
The soap granule pneumatic conveying system comprises several essential components that work in tandem to ensure smooth material transport. These include the material feed hopper, the air supply unit (typically a blower or compressor), the conveying pipeline, and the discharge hopper. Each component plays a vital role in the overall functionality of the system. The feed hopper is responsible for storing and feeding the soap granules into the system, while the air supply unit generates the necessary air pressure to move the material through the pipeline. The conveying pipeline, often made of durable materials like stainless steel or plastic, ensures the safe and efficient transport of the granules. Finally, the discharge hopper collects the material at the destination point, completing the transport cycle.
Working Principle of the Pneumatic Conveying System
The working principle of the soap granule pneumatic conveying system is based on the use of air as the conveying medium. The system operates by creating a pressure differential between the inlet and outlet of the pipeline. When the air supply unit is activated, it generates a flow of air that moves through the pipeline. As the air flows, it entrains the soap granules, lifting them from the feed hopper and transporting them to the discharge hopper. The air velocity within the pipeline is carefully controlled to ensure that the granules are carried without excessive wear or degradation. This principle allows for a continuous and controlled movement of the material, minimizing the need for manual handling and reducing the risk of contamination or spillage.
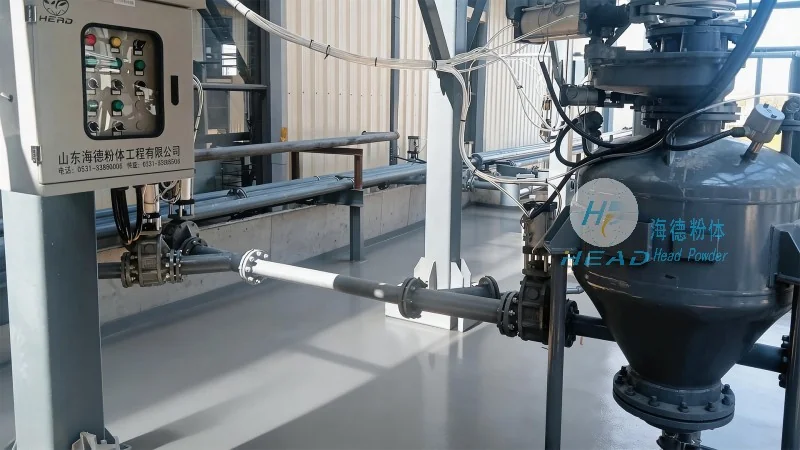
Operation Process: Step-by-Step Guide
The operation process of the soap granule pneumatic conveying system can be broken down into several key steps. First, the soap granules are loaded into the feed hopper. The system is then started by activating the air supply unit, which generates the required air pressure. The air flow begins to move through the pipeline, and the granules are entrained and transported. As the material reaches the discharge hopper, it is collected and ready for further processing or use. The system continues to operate until the feed hopper is emptied or the required amount of material has been transported. The process is typically automated, with sensors and controls ensuring that the system operates efficiently and safely. Regular maintenance checks are also performed to ensure the longevity and reliability of the system.
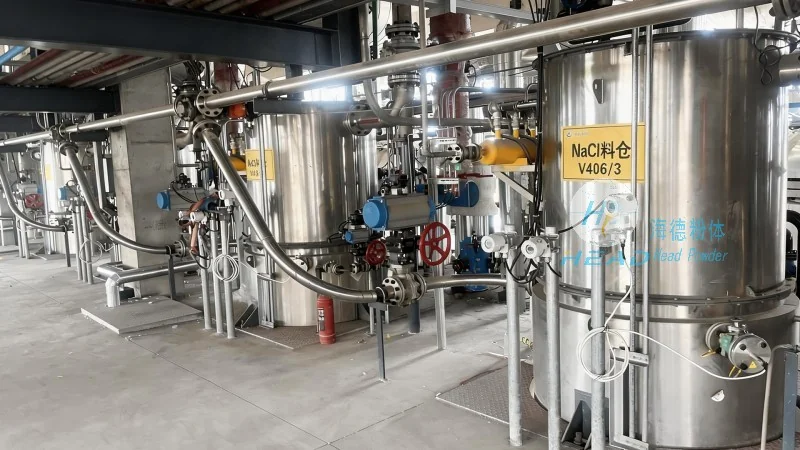
Advantages of Using a Pneumatic Conveying System for Soap Granules
Implementing a pneumatic conveying system for soap granules offers several advantages over traditional methods such as belt conveyors or manual handling. One of the primary benefits is the reduction in labor costs, as the system automates the material transport process. Additionally, the system minimizes the risk of product contamination, as the material is enclosed within the pipeline, preventing exposure to external elements. The system also reduces the risk of product degradation due to the controlled air flow and minimal contact with surfaces. Furthermore, the system can handle varying material flow rates and can be easily integrated into existing industrial processes. The durability of the components, such as the pipeline and air supply unit, ensures long-term operation with minimal downtime.
Conclusion and Company Overview
The operation process and working principle of the soap granule pneumatic conveying system demonstrate a sophisticated approach to material handling in industrial applications. By leveraging the principles of pneumatic transport, the system ensures efficient, reliable, and safe movement of soap granules. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing such systems tailored to the specific needs of industrial clients. With a focus on quality and performance, the company ensures that its systems meet the highest standards of efficiency and reliability. Based in Shandong, China, HeadPowder has established itself as a trusted partner in the industry, providing comprehensive solutions for material transport and processing needs.




