For industrial applications involving sodium bicarbonate, efficient and reliable material handling equipment is crucial. This equipment is designed to ensure the safe and effective transport of sodium bicarbonate, a widely used chemical in various industries such as food processing, pharmaceuticals, and chemical manufacturing. The proper operation of these systems not only enhances productivity but also maintains product quality and safety standards.
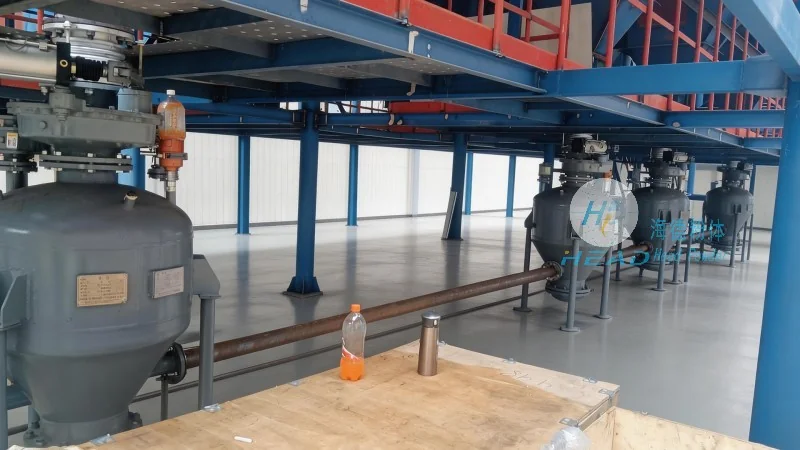
Key Components of the Material Handling System
The material handling equipment for sodium bicarbonate typically consists of several key components that work in tandem to facilitate the transport process. These components include feed hoppers, conveyor systems (often using belt or screw conveyors), control panels, and discharge mechanisms. Each component plays a vital role in ensuring smooth operation and minimizing the risk of material degradation or spillage.
Operation Process: Step-by-Step Overview
The operation of the sodium bicarbonate material handling equipment follows a systematic process to ensure consistent and efficient material transport. The process begins with the loading of sodium bicarbonate into the feed hopper. The hopper is designed to hold a sufficient quantity of material, allowing for continuous feeding without interruptions. Once the material is in the hopper, an automated feeding mechanism, such as a screw or vibratory feeder, gradually releases the sodium bicarbonate into the conveyor system.
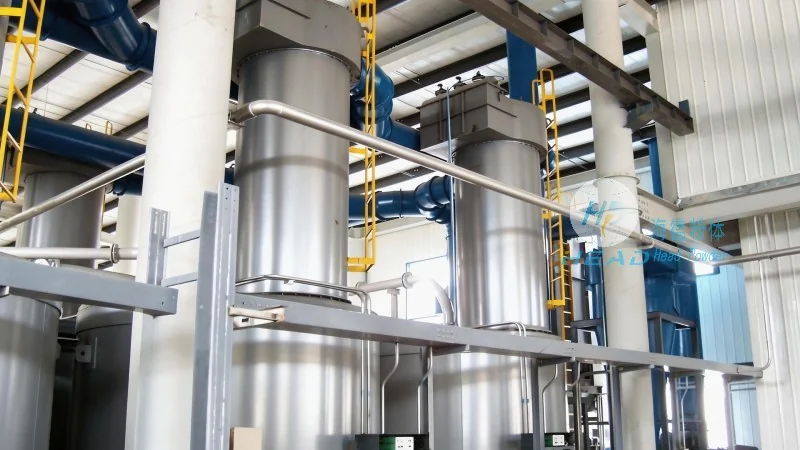
The conveyor system then transports the sodium bicarbonate through the processing line. Depending on the specific design, this may involve belt conveyors for bulk material movement or screw conveyors for more precise control over the flow rate. The conveyor is equipped with sensors and controls that monitor the material level and flow rate, ensuring that the system operates within optimal parameters. As the material moves through the conveyor, it may pass through additional processing stages, such as screening or blending, before reaching the discharge point.
At the discharge end, the sodium bicarbonate is released into a storage bin or directly into packaging equipment. The discharge mechanism is designed to prevent blockages and ensure a smooth flow of material. The entire operation is typically controlled by a centralized control panel, which allows operators to monitor and adjust the system parameters as needed. This control system ensures that the material handling process is consistent, efficient, and safe.
Working Principle: Mechanical and Control Systems
The working principle of the sodium bicarbonate material handling equipment relies on a combination of mechanical and control systems. The mechanical components, such as conveyors and feeders, are designed to handle the physical properties of sodium bicarbonate, including its density, flowability, and potential for caking. The conveyor system uses motor-driven mechanisms to move the material along the designated path, while the feeders regulate the flow rate to maintain a steady supply.
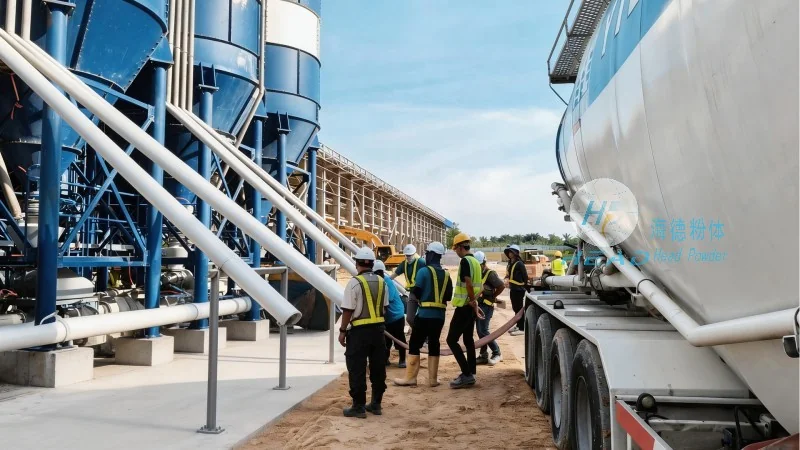
The control system is integral to the equipment's operation, providing real-time monitoring and adjustment capabilities. Sensors are installed at various points in the system to detect material levels, flow rates, and any potential blockages. These sensors send signals to the control panel, which processes the data and adjusts the motor speeds or feeder settings accordingly. This closed-loop control system ensures that the material handling process is optimized for efficiency and safety.
In addition to mechanical and control systems, the equipment may also incorporate features such as dust suppression and material separation to maintain product quality. Dust suppression systems help to minimize airborne particles, which is important for maintaining a clean working environment and preventing product contamination. Material separation mechanisms, such as screens or classifiers, can be integrated to remove impurities or adjust the particle size of the sodium bicarbonate, ensuring that the final product meets the required specifications.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized material handling equipment for the chemical industry. With a focus on innovation and quality, the company has developed advanced solutions for handling sodium bicarbonate and other bulk materials. Headpowder's equipment is designed to meet the specific needs of various industries, ensuring reliable and efficient material transport while maintaining product integrity.
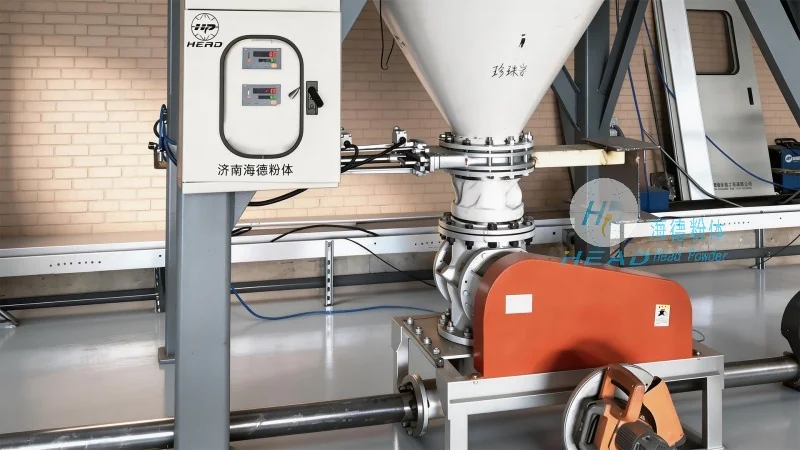
Headpowder is committed to providing high-quality, durable equipment that is built to withstand the demands of industrial environments. The company's products are engineered with precision and attention to detail, ensuring long-term performance and minimal maintenance requirements. By leveraging advanced technology and industry expertise, Headpowder delivers solutions that enhance operational efficiency and reduce downtime for its clients.
Headquartered in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. serves a global customer base with its comprehensive range of material handling solutions. The company's dedication to customer satisfaction and product excellence has established it as a trusted partner in the chemical processing industry. Whether for new installations or equipment upgrades, Headpowder offers tailored solutions that meet the unique requirements of each project.




