HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for handling sintered ash. This article provides a detailed overview of the operation process and working principles of such systems, highlighting the key components, operational steps, and technical advantages that make them efficient for industrial applications.
Key Components of the Pneumatic Conveying System
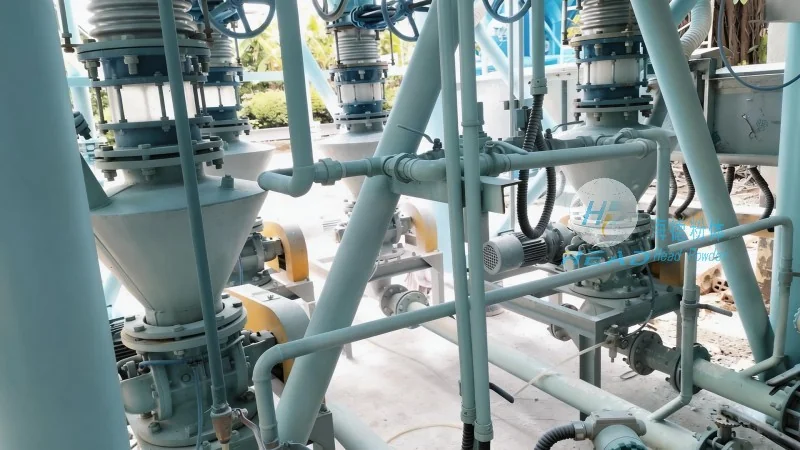
The sintered ash pneumatic conveying system typically consists of several critical components that work in tandem to ensure smooth material transport. These include a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, a pressure vessel or receiver for material collection, and a blower or air compressor to generate the necessary air pressure. Each component plays a vital role in maintaining the system's efficiency and reliability.
Operation Process of the Sintered Ash Pneumatic Conveying System
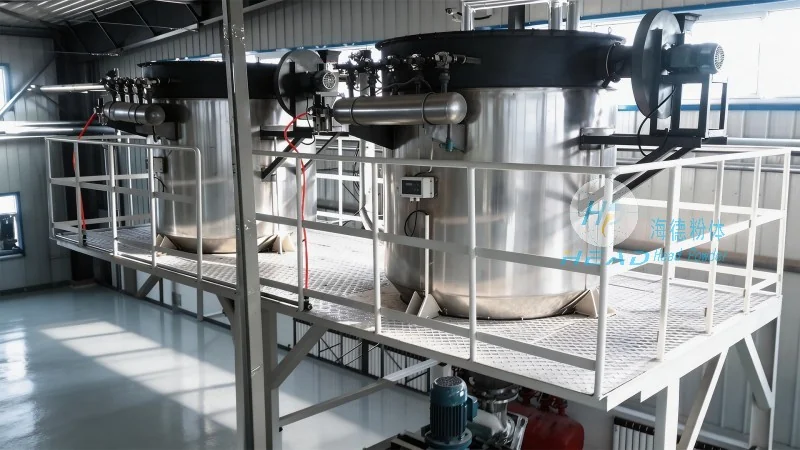
The operation of the system begins with the loading of sintered ash into the hopper. The feeder then regulates the material flow into the conveying pipeline, ensuring a consistent feed rate. Simultaneously, the blower generates high-pressure air, which is introduced into the pipeline. The air and material mixture travels through the pipeline under pressure, reaching the receiver where the material is deposited. The air, now separated from the material, is either recirculated or vented, depending on the system design. This continuous cycle allows for efficient and uninterrupted transport of sintered ash from the source to the destination.
Working Principle of the Pneumatic Conveying System
The core working principle of the sintered ash pneumatic conveying system is based on the use of air as the conveying medium. The system operates under pressure, where the air flow creates a negative pressure or positive pressure environment within the pipeline. In positive pressure systems, the air pressure is higher than the ambient air pressure, pushing the material forward. In negative pressure systems, the air is drawn from the pipeline, creating a vacuum that pulls the material along. For sintered ash, a positive pressure system is commonly used due to its ability to handle abrasive and dusty materials effectively. The air velocity within the pipeline is carefully controlled to prevent material deposition and ensure smooth transport.
Technical Advantages and Applications
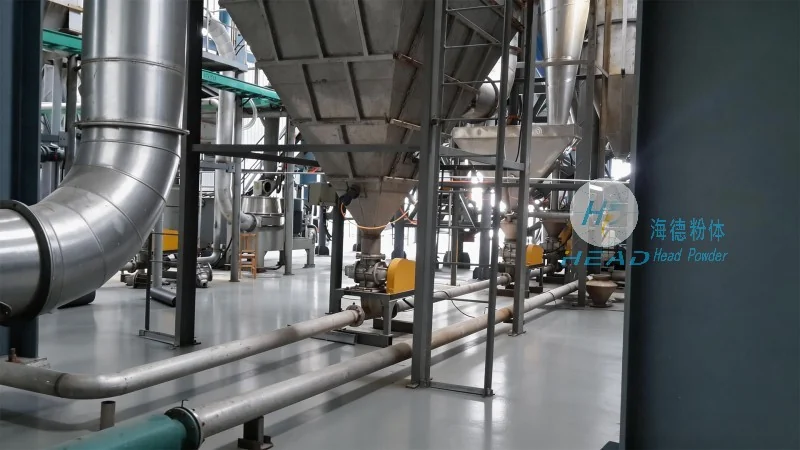
HeadPowder's sintered ash pneumatic conveying systems offer several technical advantages that make them ideal for industrial use. These include high efficiency in material transport, minimal material loss, and reduced labor costs compared to traditional methods like belt conveyors or trucks. The systems are also designed to handle abrasive and dusty sintered ash without causing wear and tear on components. Additionally, the enclosed pipeline system helps in controlling dust emissions, improving workplace safety and environmental compliance. These systems are widely used in power plants, steel mills, and other industrial facilities where sintered ash needs to be transported over long distances or to different processing units.
Conclusion
HeadPowder Engineering Co., Ltd., based in Shandong, China, provides comprehensive solutions for sintered ash pneumatic conveying systems. By understanding the operation process and working principles, industrial facilities can optimize their material handling processes, enhance efficiency, and reduce operational costs. The advanced design and robust construction of these systems ensure reliable performance, making them a preferred choice for handling sintered ash in various industrial applications.




