Barley powder pneumatic conveying equipment is a specialized system designed for the efficient transport of barley powder and other similar bulk powders. This technology utilizes air as the medium to move material from one location to another, offering advantages such as reduced contamination, improved hygiene, and the ability to handle materials in a closed system. The equipment is widely used in the food processing industry, particularly in facilities that handle barley-based products, ensuring that the material is transported safely and effectively without exposure to external contaminants.
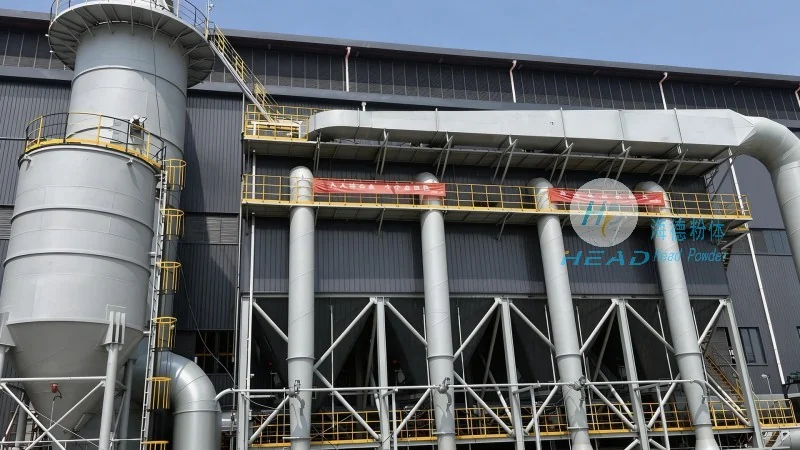
Core Principle of Pneumatic Conveying Systems
The fundamental principle behind pneumatic conveying is the use of compressed air to create a flow that propels the powder particles through a pipeline. In the case of barley powder, the system typically operates under positive pressure, where air is forced into the conveying line, carrying the powder along with it. The equipment includes components like a hopper for material storage, a feeder to control the flow rate, a compressor to generate the necessary air pressure, and a receiver to collect the material at the destination. The design of the system is tailored to the specific characteristics of barley powder, including its particle size, density, and flowability, to ensure optimal performance and minimal degradation of the product.
Key Components and Their Functions
Several critical components make up a barley powder pneumatic conveying system. The hopper serves as the storage vessel, holding the barley powder until it is needed for transport. The feeder, often a rotary valve or a screw feeder, regulates the amount of powder released into the conveying line, ensuring a consistent flow rate. The compressor is responsible for generating the high-pressure air required to move the powder, with the pressure levels adjusted based on the distance and resistance in the pipeline. The conveying line itself is typically made of materials like stainless steel or plastic, chosen for their resistance to corrosion and ability to maintain product purity. The receiver, or discharge hopper, collects the material at the end of the conveying process, allowing for further processing or storage. Each component plays a vital role in the overall efficiency and reliability of the system.
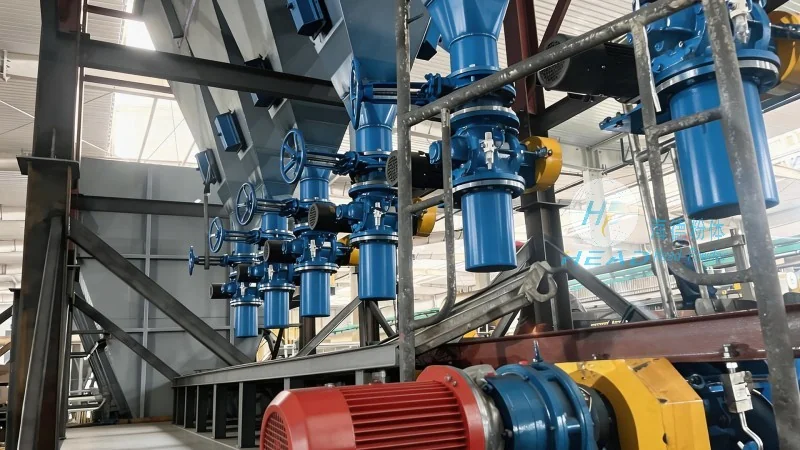
Working Scene Characteristics and Applications
The working scene characteristics of barley powder pneumatic conveying equipment are tailored to the specific needs of food processing facilities. In a typical grain processing plant, the equipment is used to transport barley powder from storage silos to milling or mixing areas, ensuring that the material is moved without breaking the product's integrity. The closed system design prevents dust and contaminants from entering the environment, which is crucial for maintaining food safety standards. Additionally, the system can be integrated into larger production lines, allowing for seamless material transfer between different processing stages. The equipment is also suitable for applications where hygiene is paramount, such as in the production of barley-based beverages or baked goods, where any contamination could affect the final product quality. The flexibility of the system allows it to be adapted to various production scales, from small-scale artisanal operations to large industrial facilities.
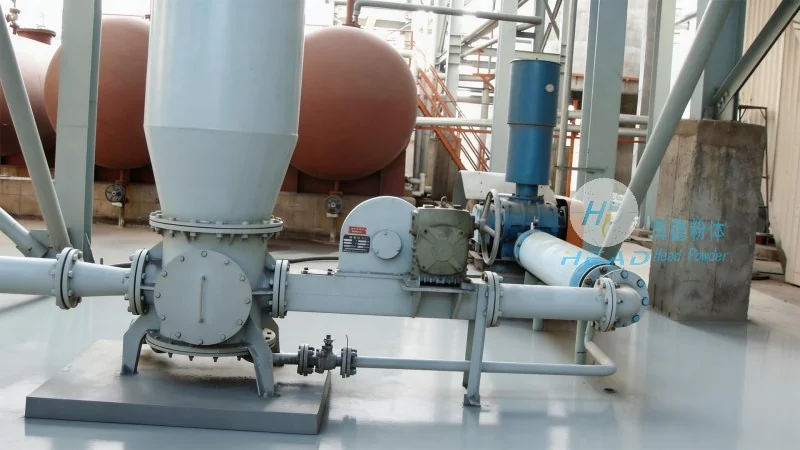
Advantages and Benefits in Practical Use
Implementing barley powder pneumatic conveying equipment offers several advantages in real-world applications. One of the primary benefits is the reduction in labor costs, as the system automates the material transport process, eliminating the need for manual handling of bulk powders. This not only improves efficiency but also enhances workplace safety by minimizing the risk of dust exposure and material spills. The closed system design also helps maintain product quality by preventing moisture absorption or contamination from external sources, which is particularly important for barley powder used in food products. Furthermore, the system's ability to handle materials in a continuous flow allows for consistent production output, reducing downtime and improving overall operational efficiency. The compact design of the equipment makes it suitable for facilities with limited space, and the low maintenance requirements contribute to long-term cost savings.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of pneumatic conveying equipment for the food and bulk material processing industries. With a focus on innovation and quality, the company has developed specialized solutions for handling barley powder and other similar materials. HeadPowder's products are designed to meet the stringent requirements of the food industry, including compliance with hygiene standards and the ability to handle sensitive materials without degradation. The company's engineering expertise ensures that each system is tailored to the specific needs of the client, whether it's a small-scale operation or a large industrial facility. HeadPowder's commitment to customer satisfaction and product reliability has made it a trusted partner for facilities worldwide, providing efficient and effective pneumatic conveying solutions.




