Understanding the working principle and features of negative pressure powder conveying systems is crucial for industries that handle bulk powders efficiently and safely. This article delves into the core mechanisms and advantages of such systems, highlighting how they enhance operational performance and reliability.
Introduction to Negative Pressure Powder Conveying
Negative pressure powder conveying systems are designed to transport dry powders and granules from a source to a destination using a vacuum or reduced pressure environment. Unlike positive pressure systems that force air and material through a pipeline, negative pressure systems draw material into the system by creating a vacuum, which helps minimize dust emissions and improve material containment. This approach is particularly beneficial for applications requiring strict environmental control and material integrity preservation.
Core Working Principle of Negative Pressure Powder Conveying
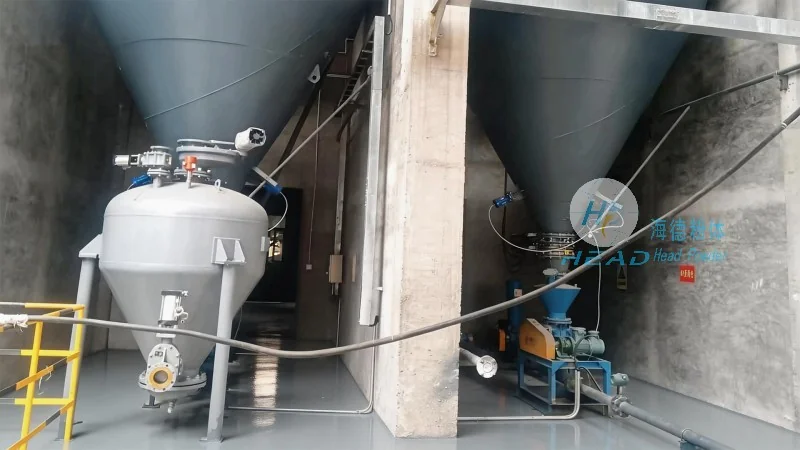
The fundamental working principle of negative pressure powder conveying involves the creation of a pressure differential between the source and the destination. The system operates by generating a vacuum at the receiving end or along the pipeline, which draws the powder material from the source into the conveying line. Key components include a vacuum pump, a filter system, and a conveying pipeline. The vacuum pump creates the necessary suction force, while the filter system ensures that the air being drawn in is clean and free from particulate matter. The conveying pipeline transports the material from the source to the destination, often using flexible hoses or rigid pipes depending on the application requirements.
Key Features and Advantages of Negative Pressure Powder Conveying Systems
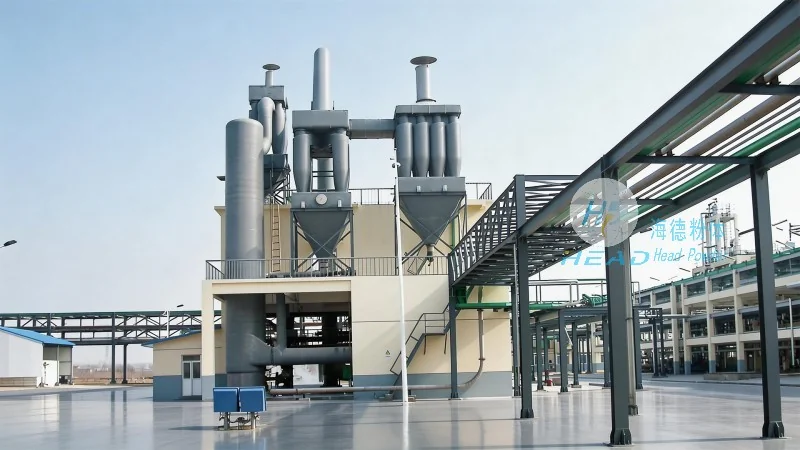
One of the primary advantages of negative pressure powder conveying is its ability to maintain a clean and dust-free environment. By drawing material into the system rather than expelling it, these systems significantly reduce the risk of dust contamination in the surrounding area. This is especially important in industries such as pharmaceuticals, food processing, and electronics, where product purity and environmental compliance are paramount. Additionally, negative pressure systems offer improved material handling efficiency, as they can transport powders over longer distances with less energy consumption compared to positive pressure systems.
Another notable feature is the enhanced safety provided by these systems. The vacuum environment reduces the likelihood of material spillage or leakage, minimizing the risk of accidents and health hazards. Furthermore, the enclosed nature of the conveying line prevents cross-contamination between different materials, ensuring that each batch remains pure and consistent. This is a critical factor for manufacturers who need to maintain high standards of quality control in their production processes.
Application-Specific Benefits and Considerations
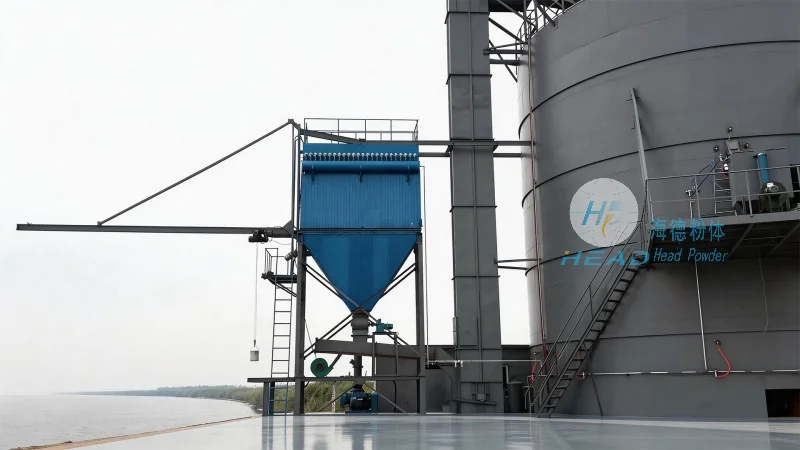
Negative pressure powder conveying systems are versatile and can be adapted to various industrial applications. For example, in the chemical industry, these systems are used to transport reactive powders safely, while in the food industry, they help maintain hygienic conditions during the handling of sensitive ingredients. The flexibility of the system allows for customization based on the specific characteristics of the powder, such as particle size, moisture content, and flowability. However, it is important to consider factors like material compatibility with the conveying components and the need for regular maintenance to ensure optimal performance.
Conclusion and Company Overview
Overall, negative pressure powder conveying systems represent a sophisticated solution for efficient and safe powder handling. Their ability to maintain a clean environment, enhance operational efficiency, and ensure product quality makes them a preferred choice in many industries. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality negative pressure powder conveying systems tailored to meet the diverse needs of its clients. With a commitment to innovation and customer satisfaction, the company continues to advance the technology and application of powder handling solutions, helping businesses achieve their operational goals while adhering to strict industry standards.




