The sorghum distiller's grains powder conveying system is a specialized equipment designed for the efficient transportation of powder materials, particularly sorghum distiller's grains, which are byproducts from the distillation process in the alcohol industry. This system is crucial for optimizing material handling in distilleries, ensuring consistent and reliable flow of the powder while maintaining operational efficiency and safety standards. The system is engineered to handle the unique characteristics of sorghum distiller's grains, such as their fine particle size and potential for dust generation, which require advanced conveying solutions to prevent material loss and environmental contamination.
Working Principle of the Powder Conveying System
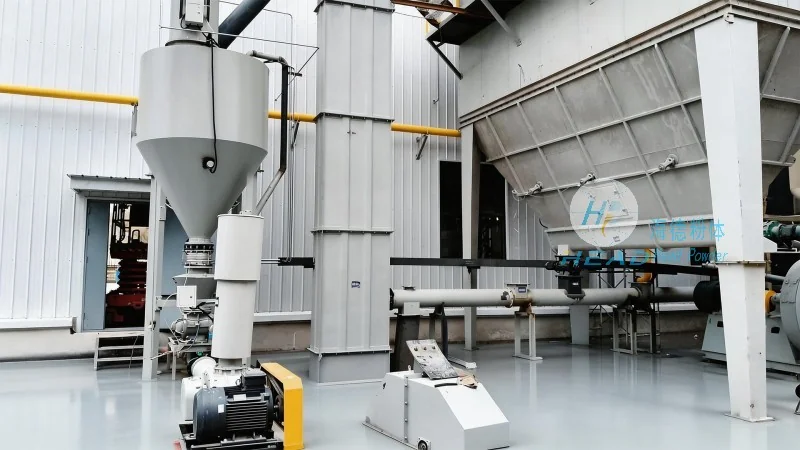
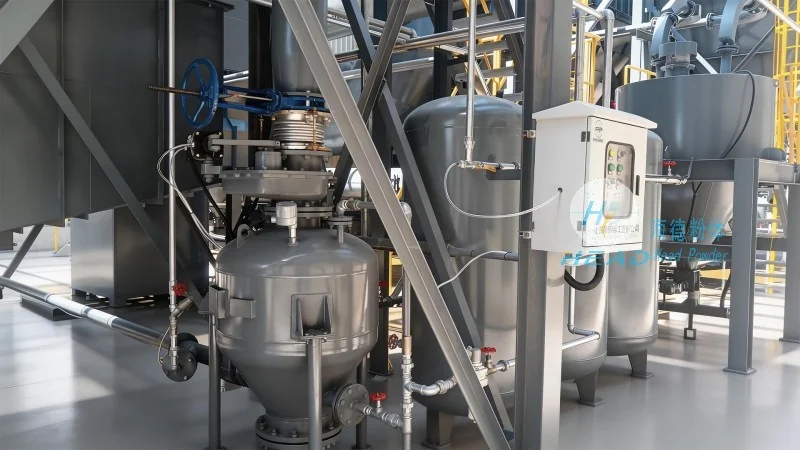
The core working principle of the sorghum distiller's grains powder conveying system involves a combination of mechanical and pneumatic components working in tandem to move the powder from the source to the destination. The system typically starts with a hopper or storage silo where the sorghum distiller's grains are stored. From there, a rotary valve or feeder is used to control the flow rate of the material into the conveying line. The conveying mechanism can be either a positive displacement blower or a vacuum pump, which generates the necessary air pressure or suction to transport the powder through a pipeline. The pipeline is equipped with appropriate fittings, such as elbows and tees, to direct the flow and maintain the velocity required to prevent material settling or blockages. At the discharge end, a receiver or silo is used to collect the conveyed powder, and a rotary valve or gate valve controls the release of the material to downstream processes. The entire system operates under controlled pressure and flow conditions, ensuring that the powder is transported without degradation or loss of quality.
Key Features and Advantages of the Conveying System
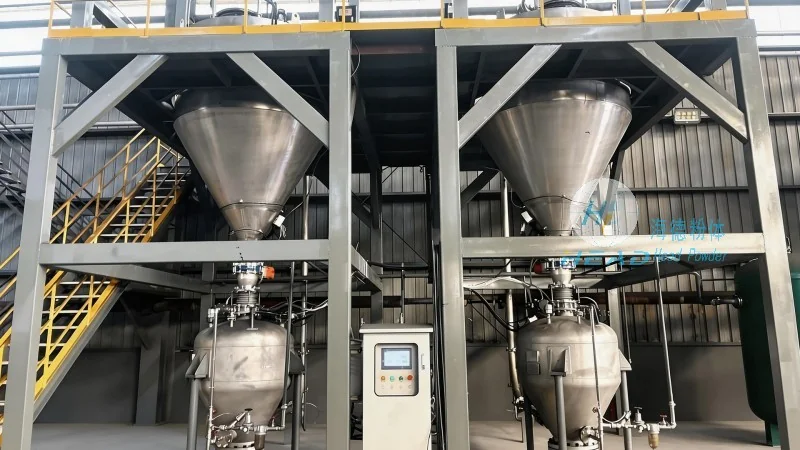
The sorghum distiller's grains powder conveying system from Shandong HeadPowder Engineering Co., Ltd. (headpowder) is designed with several key features that enhance its performance and reliability. One of the primary features is the use of a closed-loop system, which minimizes dust emissions and prevents environmental contamination, a critical consideration for industrial operations. The system incorporates advanced control technology, allowing for precise regulation of flow rates and pressure, which ensures consistent material handling and reduces the risk of overloading or underloading the conveying line. Another important feature is the robust construction of the components, including the hopper, feeder, and pipeline, which are made from corrosion-resistant materials to withstand the acidic and abrasive nature of sorghum distiller's grains. The system also includes safety features such as pressure relief valves and overcurrent protection, ensuring safe operation in industrial settings. Additionally, the system is designed for easy maintenance and cleaning, with removable components that can be cleaned without disassembling the entire system, reducing downtime and maintenance costs. The combination of these features makes the system highly efficient, reliable, and cost-effective for distilleries looking to optimize their material handling processes.
Company Information and Application
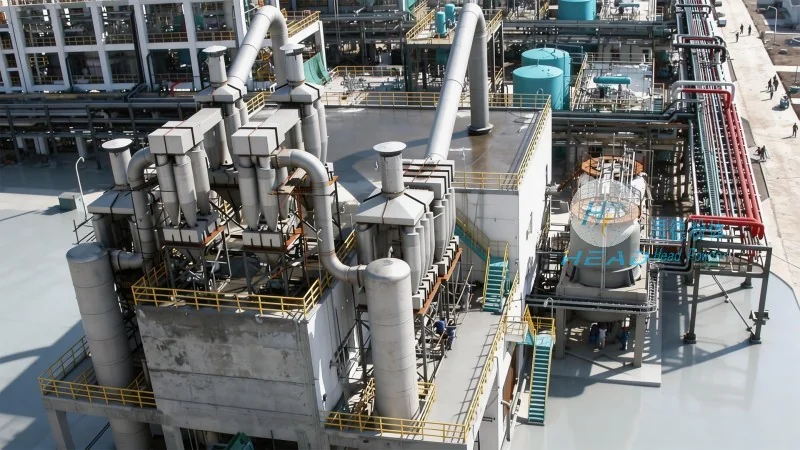
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized powder handling equipment, including the sorghum distiller's grains powder conveying system. The company is headquartered in Shandong, China, and has extensive experience in designing and manufacturing equipment for the food, pharmaceutical, and chemical industries. The company's commitment to quality and innovation has made its products widely recognized in the market for their reliability and efficiency. The sorghum distiller's grains powder conveying system is particularly well-suited for distilleries that need to handle large volumes of sorghum distiller's grains efficiently and safely. The system's ability to maintain consistent flow rates and minimize dust emissions makes it an ideal solution for modern distilleries seeking to improve their operational efficiency and comply with environmental regulations. With its robust construction and advanced control technology, the system provides long-term value and reliability for distilleries looking to optimize their material handling processes.




