

Working Principle and Features of the Camellia Seed Pneumatic Conveying System
Camellia seed processing is a critical stage in the production of edible oil and other valuable products. The pneumatic conveying system for camellia seeds is a sophisticated technology that facilitates the efficient and hygienic transport of these seeds within a processing facility. This system is essential for preserving the quality and integrity of the seeds during handling, preventing damage or contamination. By utilizing air as the conveying medium, the system ensures a clean and controlled transfer of the material, which is vital for downstream processing steps.
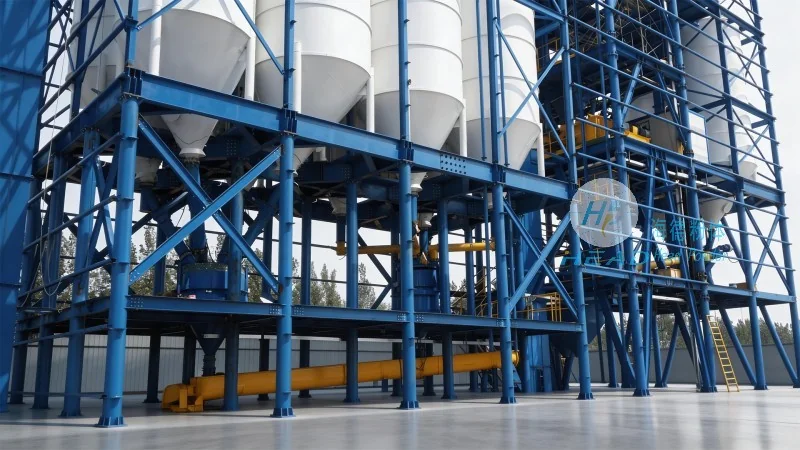
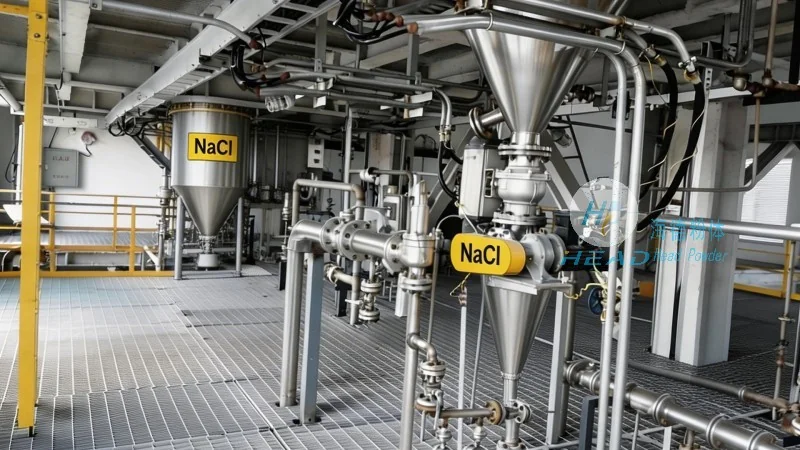
Working Principle of the Camellia Seed Pneumatic Conveying System
The camellia seed pneumatic conveying system operates based on the principle of air movement to transport the seeds. The system typically comprises several key components: a hopper for seed storage, a rotary valve to regulate seed flow, a blower to generate air pressure, and a network of pipes to direct the seed-air mixture. The process initiates when camellia seeds are fed into the hopper. The rotary valve then controls the amount of seeds entering the blower, which creates a high-pressure air stream. This air stream carries the seeds through the pipes to the destination point, such as a storage silo or a processing unit. The system maintains consistent pressure and flow rates to ensure smooth and uninterrupted transport. The use of air as the conveying medium is particularly advantageous as it prevents mechanical crushing or abrasion of the seeds, preserving their quality and market value. Additionally, the system can accommodate various seed sizes and types, making it versatile for different processing needs. Some systems may employ a combination of positive and negative pressure to optimize performance, depending on the specific requirements of the facility.
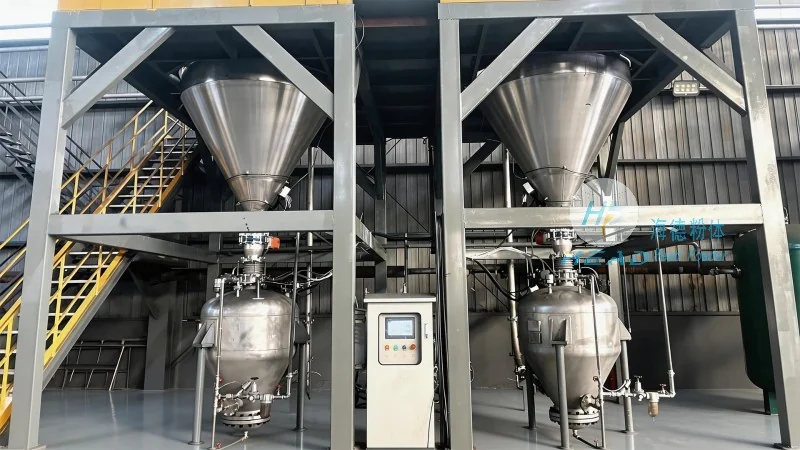
Key Features and Advantages of the System
The camellia seed pneumatic conveying system offers several key features that enhance its performance and reliability. Firstly, it provides a hygienic and clean handling environment, which is critical in food processing applications. The absence of mechanical contact reduces the risk of contamination, ensuring that the seeds remain in their natural state. Secondly, the system is highly flexible and can be customized to fit the specific layout and requirements of a processing facility. It can be expanded or reconfigured as the plant grows, allowing for scalability. Thirdly, the system is energy-efficient, with the blower and other components designed to operate at optimal efficiency, reducing energy consumption and operational costs. Fourthly, the system is durable and low-maintenance, with robust construction and high-quality materials that can withstand continuous operation. Regular maintenance is minimal, contributing to long-term cost savings. Furthermore, the system ensures consistent and uniform seed flow, which is essential for maintaining the quality of the final product. The ability to control the speed and pressure of the air stream allows for precise handling, preventing overloading or blockages in the pipes. The system also minimizes dust generation and improves workplace safety by containing the seeds within the air stream, reducing exposure to airborne particles.
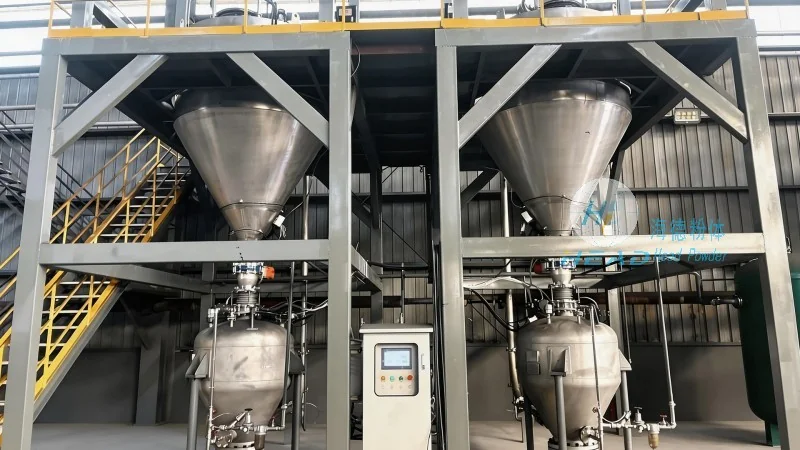
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of pneumatic conveying systems, specializes in providing customized solutions for the camellia seed industry. With years of experience in the field, HeadPowder has developed a reputation for producing high-quality, reliable, and efficient equipment that meets the needs of its customers. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians who are dedicated to providing excellent customer service and support. HeadPowder's commitment to quality and innovation has made it a trusted partner for many camellia seed processing facilities around the world. The company's products are designed to enhance operational efficiency, reduce downtime, and improve overall productivity. HeadPowder offers comprehensive after-sales support, including installation, training, and maintenance services, ensuring that customers receive long-term value and satisfaction. The company adheres to international standards and undergoes rigorous testing to ensure the performance and durability of its systems. HeadPowder's solutions are tailored to the unique requirements of each client, ensuring optimal performance and cost-effectiveness.