

[Pneumatic Conveying System for Camellia Seeds: An Analysis]
Camellia seed processing is a critical step in the production of edible oil and other value-added products. Efficient material handling is essential to maintain product quality and operational efficiency. This article provides an in-depth analysis of a pneumatic conveying system designed specifically for camellia seeds, highlighting its components, operational principles, and benefits.
System Overview and Core Components
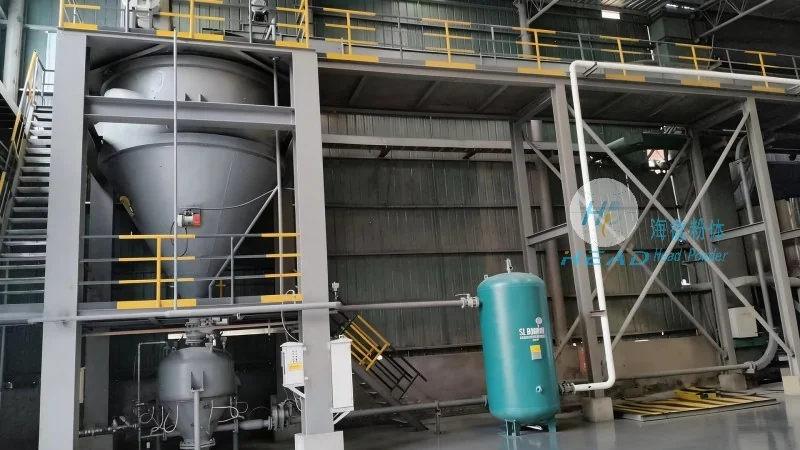
The pneumatic conveying system for camellia seeds, developed by Shandong HeadPowder Engineering Co., Ltd., is engineered to handle the unique characteristics of camellia seeds, such as their size, density, and moisture content. The system comprises several key components that work in tandem to ensure smooth and reliable material transport. These include a hopper for seed storage, a feeder to control the flow rate, a conveying pipeline, and a receiver for the processed seeds. Each component is carefully selected and integrated to optimize performance and minimize downtime.
Operational Principles and Working Mechanism
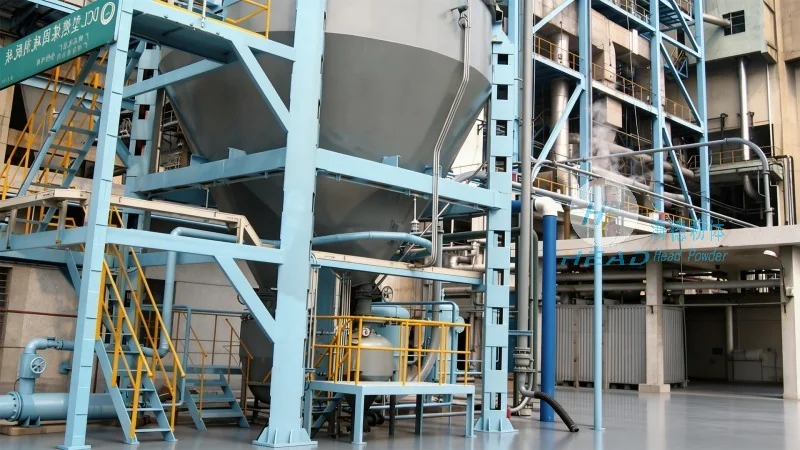
The system operates on the principle of pneumatic transport, where air is used to move the camellia seeds through a pipeline. The process begins with the seeds being fed from the hopper into the feeder, which regulates the flow based on the required processing rate. The feeder then delivers the seeds into the conveying pipeline, where they are propelled by a stream of air generated by a blower or fan. The air pressure and flow rate are precisely controlled to ensure the seeds move efficiently without causing damage or degradation. The conveying pipeline is typically made of durable materials like stainless steel or high-density polyethylene to withstand the abrasive nature of the seeds and maintain hygiene standards.
Advantages and Performance Benefits
Compared to traditional mechanical conveying methods, the pneumatic system offers several advantages that enhance operational efficiency and product quality. One of the primary benefits is the ability to handle the seeds in a closed system, which reduces exposure to contaminants and maintains consistent moisture levels. This is particularly important for camellia seeds, as moisture control is crucial for preventing spoilage and ensuring optimal oil extraction. Additionally, the system minimizes product breakage and dust generation, which helps preserve the seed's integrity and reduces the risk of health hazards. The automated control features allow for precise adjustment of flow rates and pressure, enabling operators to adapt to varying production demands without manual intervention. This flexibility enhances the system's adaptability and reduces the need for frequent maintenance.
Application and Integration in Processing Facilities
The pneumatic conveying system is designed to be easily integrated into existing camellia seed processing facilities. Its modular design allows for flexible installation, whether as a standalone unit or as part of a larger processing line. The system can be configured to handle different stages of the processing workflow, such as transferring seeds from storage to the extraction unit or moving processed seeds to packaging areas. The integration is facilitated by standard interfaces and connections that ensure seamless communication with other equipment in the facility. This adaptability makes the system suitable for both small-scale and large-scale processing operations, providing scalability and cost-effectiveness.
Maintenance and Operational Considerations
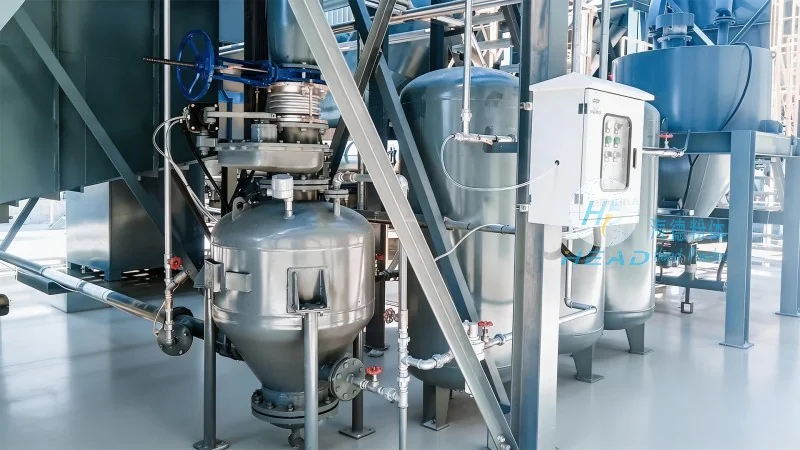
To ensure the long-term reliability and performance of the pneumatic conveying system, regular maintenance is essential. The system includes features such as air filtration to prevent dust accumulation in the pipeline and blower, which helps maintain air quality and reduce maintenance costs. Regular cleaning of the hopper, feeder, and pipeline is recommended to prevent clogging and ensure consistent flow. The system's control panel provides real-time monitoring of key parameters, such as pressure, flow rate, and temperature, allowing operators to detect and address issues promptly. This proactive approach to maintenance helps minimize downtime and extends the system's operational life. Additionally, the use of durable materials in the construction of the components ensures resistance to wear and tear, reducing the frequency of replacements and overall maintenance expenses.
Conclusion
The pneumatic conveying system for camellia seeds, as developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution for efficient material handling in seed processing. By leveraging pneumatic transport principles, the system offers significant advantages in terms of product quality, operational efficiency, and flexibility. Its design and integration capabilities make it a valuable asset for processing facilities aiming to enhance their production processes. With proper maintenance and operational management, this system can contribute to improved productivity and profitability in the camellia seed industry.