

[H1]What is a High-Pressure Bin Pump Powder Conveying System Equipment? What Are Its Design Principl
High-pressure bin pump powder conveying systems are advanced industrial equipment designed to transport bulk powder materials efficiently and reliably over long distances. These systems are widely used in various industries, including chemical, pharmaceutical, food processing, and mining, where the safe and effective handling of powders is critical. The core component of such a system is the high-pressure bin pump, which operates on the principle of creating a pressure differential to move powders through pipelines.
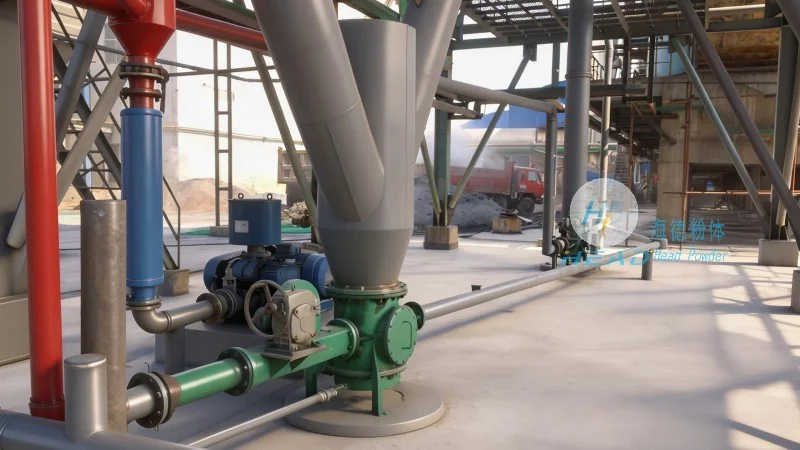
Design Principles of High-Pressure Bin Pump Systems
The design of a high-pressure bin pump powder conveying system is based on several key principles that ensure optimal performance and reliability. The primary design principle is the generation of sufficient pressure to overcome the resistance of the pipeline and the powder's friction within the system. This is achieved through the use of a high-pressure pump that can deliver pressures ranging from several hundred to several thousand pounds per square inch (psi), depending on the system's requirements and the characteristics of the powder being conveyed.
Another critical design principle is the consideration of the powder's flow properties. Different powders have varying flowability, such as cohesive or free-flowing materials. The system's design must account for these properties to prevent issues like blockages, agglomeration, or uneven flow. This often involves incorporating features like a hopper with a specific geometry, a feeder mechanism that can handle the powder's characteristics, and a pump chamber designed to maintain consistent pressure and flow rates.
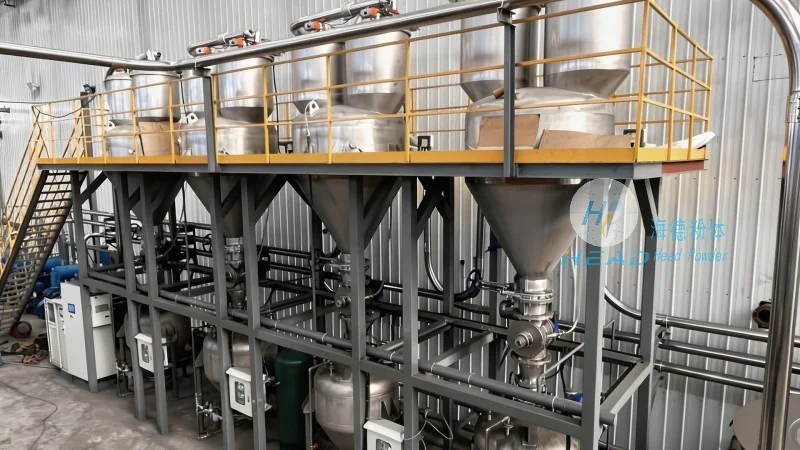
Key Components and Their Functions
A typical high-pressure bin pump powder conveying system consists of several key components, each playing a vital role in the overall operation. The main components include a storage bin or hopper, a feeder (such as a rotary valve or a screw feeder), a high-pressure pump, a pipeline system, and a control system. The storage bin is used to hold the bulk powder, while the feeder regulates the flow of powder into the pump. The high-pressure pump then pressurizes the powder and forces it through the pipeline to the destination point. The pipeline system transports the powder, and the control system monitors and adjusts the system's operation to maintain optimal performance.
Applications and Benefits
High-pressure bin pump powder conveying systems are used in a wide range of applications where the transportation of powders is essential. These systems are particularly beneficial in industries where the powder needs to be transported over long distances or through complex layouts, such as in chemical plants, pharmaceutical manufacturing facilities, and food processing plants. The benefits of using such systems include improved efficiency in material handling, reduced labor costs, increased safety due to enclosed systems, and the ability to handle a variety of powder types with different flow characteristics.
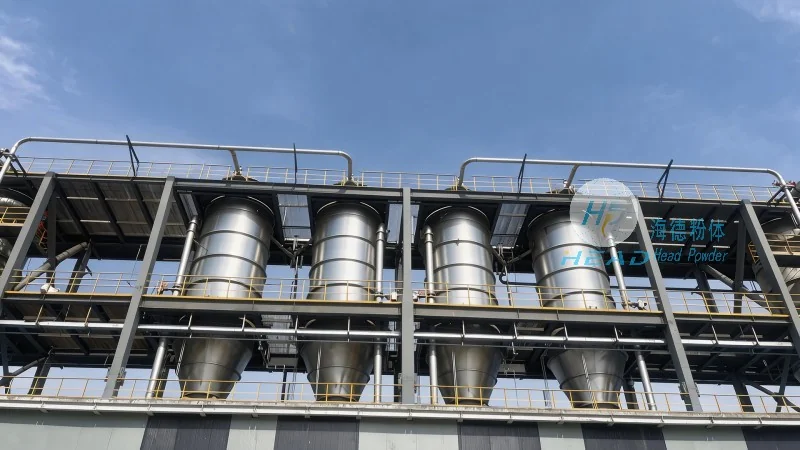
About HeadPowder: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of high-quality powder conveying equipment. With its headquarters located in Shandong, China, the company specializes in the design, manufacturing, and installation of high-pressure bin pump systems tailored to meet the specific needs of various industries. HeadPowder's team of experienced engineers and technicians utilizes advanced technology and rigorous quality control processes to ensure that each system meets the highest standards of performance, reliability, and safety. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and reliable powder handling solutions.
Conclusion
In summary, high-pressure bin pump powder conveying systems are sophisticated industrial solutions that play a crucial role in the efficient transportation of bulk powders. The design principles, key components, and applications of these systems are carefully considered to ensure optimal performance and reliability. Companies like HeadPowder, with their expertise and dedication to quality, provide the necessary equipment and support to help businesses achieve their material handling goals. Whether in chemical, pharmaceutical, or food processing industries, these systems offer a reliable and efficient way to handle powders, contributing to improved productivity and safety in industrial operations.