HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and supply of advanced pneumatic conveying systems. This article provides an overview of the ash bin pneumatic conveying equipment, detailing its structural components and operational principles to help users understand its functionality and benefits.
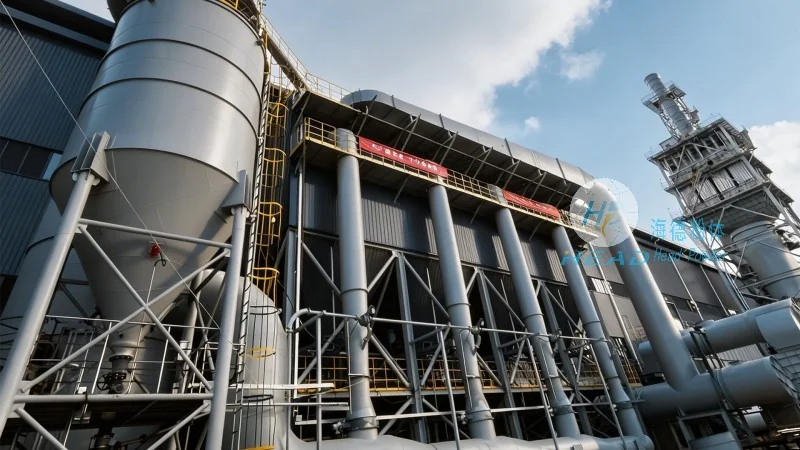
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, with its headquarters located in Shandong, China, is committed to delivering high-quality engineering solutions for industrial material transport. The company's expertise lies in the development of efficient and reliable pneumatic conveying systems, including the ash bin pneumatic conveying equipment, which is designed to meet the demands of modern industrial applications.
Introduction to Ash Bin Pneumatic Conveying Equipment
The ash bin pneumatic conveying equipment is a specialized system used for the efficient transport of bulk materials, such as fly ash, from storage bins to processing or disposal locations. This equipment is particularly valuable in power plants and other industrial facilities where large volumes of ash need to be moved safely and effectively. The system operates by utilizing compressed air or other gases to create a flow that propels the material through a pipeline network.
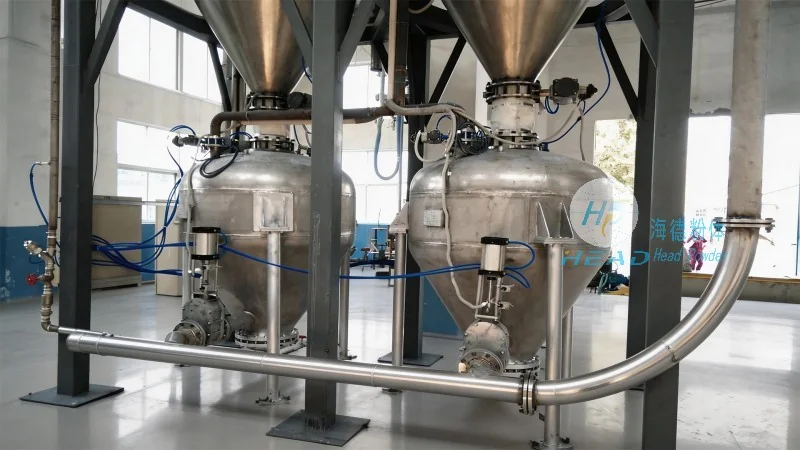
Structural Components and Working Principles
The ash bin pneumatic conveying equipment consists of several key components that work in tandem to ensure smooth material transport. These components include the ash bin, which serves as the material source; the feeder, responsible for controlling the flow of material into the conveying system; the air compressor or blower, which generates the necessary air pressure; the pipeline system, which transports the material and air mixture; and the receiver or discharge unit, where the material is deposited.
The working principle of the system involves the feeder drawing material from the ash bin and feeding it into the pipeline. Simultaneously, the air compressor supplies compressed air to the pipeline, creating a low-pressure zone that draws the material into the air stream. The material is then carried through the pipeline by the air flow, which can be either positive or negative pressure, depending on the specific design and application requirements. The receiver at the end of the pipeline collects the conveyed material, completing the transport process.
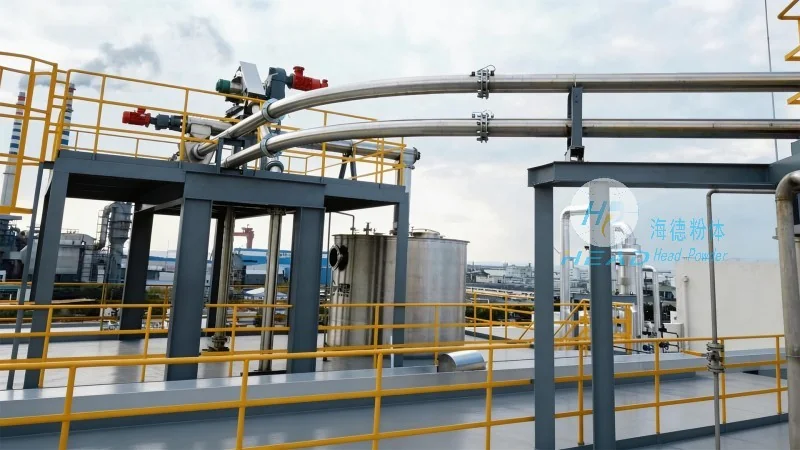
Key Features and Advantages
HeadPowder's ash bin pneumatic conveying equipment offers several advantages that make it a preferred choice for industrial applications. These include high efficiency in material transport, minimal maintenance requirements, and the ability to handle a wide range of material types and particle sizes. The system is also designed for safety and reliability, with features such as air filtration to prevent dust contamination and pressure relief valves to ensure safe operation. Additionally, the equipment is customizable to meet specific customer requirements, ensuring optimal performance for each application.
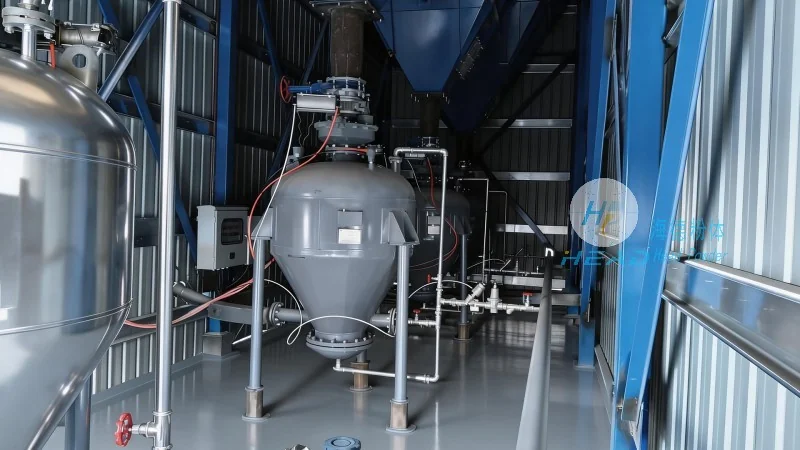
Applications and Industries
The ash bin pneumatic conveying equipment is widely used in various industries, including power generation, cement production, and waste management. In power plants, it is used to transport fly ash from the boiler ash bin to storage silos or disposal sites. In cement plants, it helps move raw materials and finished products between processing stages. The equipment is also utilized in waste management facilities for the transport of ash and other bulk waste materials.
Conclusion
HeadPowder's ash bin pneumatic conveying equipment represents a reliable and efficient solution for bulk material transport in industrial settings. With its robust design, advanced operational principles, and commitment to quality, the equipment is well-suited to meet the demands of modern industrial applications. By understanding the structural components and working principles of this system, users can make informed decisions about its application and benefits in their respective industries.




