Operation Process and Working Principle of Dust-Free Tote Bag Loading Station Material Conveying Sys
Release time:2026-09-20 23:01:41
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
This article provides an in-depth overview of the operation process and working principle of the dust-free tote bag loading station material conveying system, a critical piece of equipment in industrial material handling. The system is designed to handle bulk materials efficiently while maintaining a clean and controlled environment, which is essential for industries such as pharmaceuticals, food processing, and chemical manufacturing where contamination control is paramount.
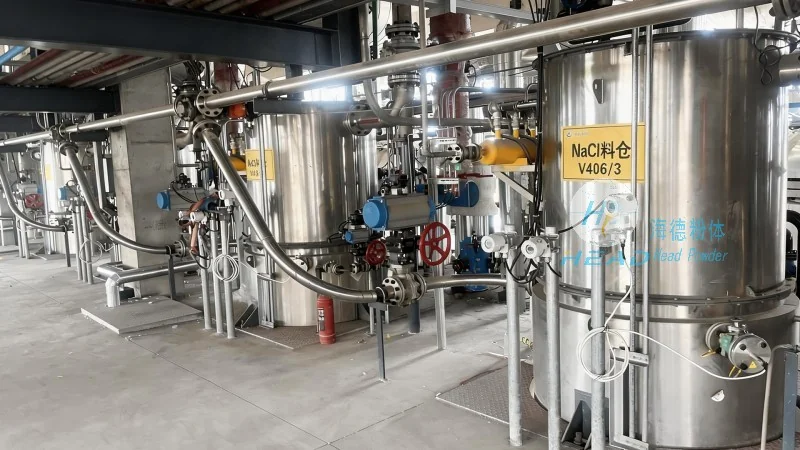
Key Components and Structure of the System
The dust-free tote bag loading station material conveying system typically consists of several key components that work in tandem to ensure smooth material transfer. At the core of the system is the tote bag itself, which is a large, flexible container used for storing and transporting bulk materials. The system is equipped with a hopper or a receiving hopper that is designed to receive material from the tote bag. This hopper is often equipped with a sealing mechanism to prevent dust from escaping during the transfer process. Additionally, the system includes a conveyor system, which may be a belt conveyor or a screw conveyor, that transports the material from the receiving hopper to the processing equipment or storage area. The conveyor system is usually enclosed to maintain a dust-free environment and is equipped with filters or other dust control measures to ensure that no particles are released into the air.
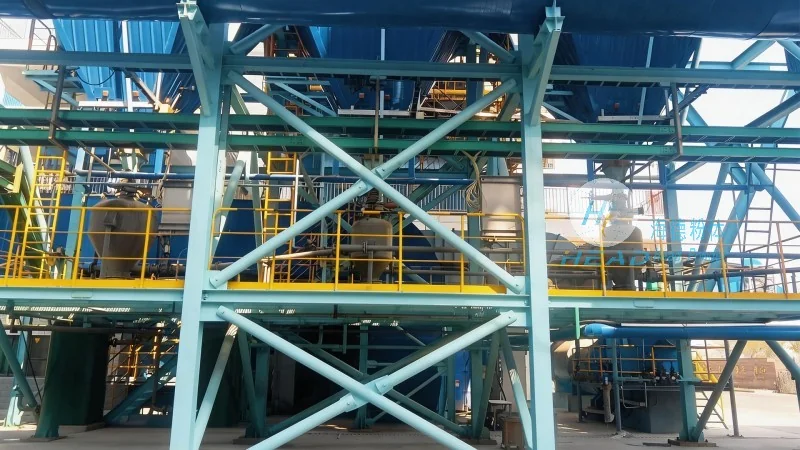
Operation Process of the Material Conveying System
The operation process of the dust-free tote bag loading station material conveying system involves several steps. First, the tote bag is positioned at the loading station, and the material inside is transferred from the bag into the receiving hopper. This is typically done using a pneumatic or mechanical system that draws the material from the bag and moves it into the hopper. The material is then conveyed from the receiving hopper to the processing equipment or storage area using the conveyor system. The system is designed to operate continuously, with the tote bag being replaced as needed to maintain a steady flow of material. The entire process is automated to minimize human intervention and reduce the risk of contamination.
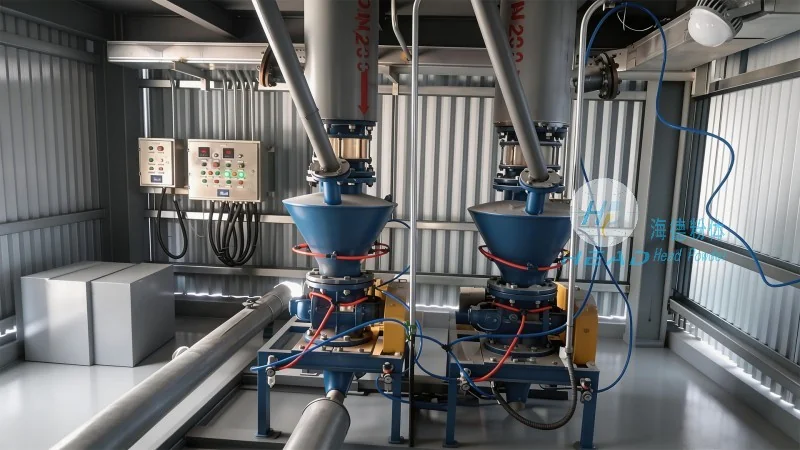
Working Principle of the System
The working principle of the dust-free tote bag loading station material conveying system is based on the principles of material handling and dust control. The system uses a combination of mechanical and pneumatic components to transfer material from the tote bag to the processing equipment while maintaining a clean environment. The receiving hopper is equipped with a sealing mechanism that prevents dust from escaping when the material is being transferred. The conveyor system is enclosed and equipped with filters to ensure that no particles are released into the air. The system is also designed to be easy to clean and maintain, which is important for industries where hygiene is a critical factor.
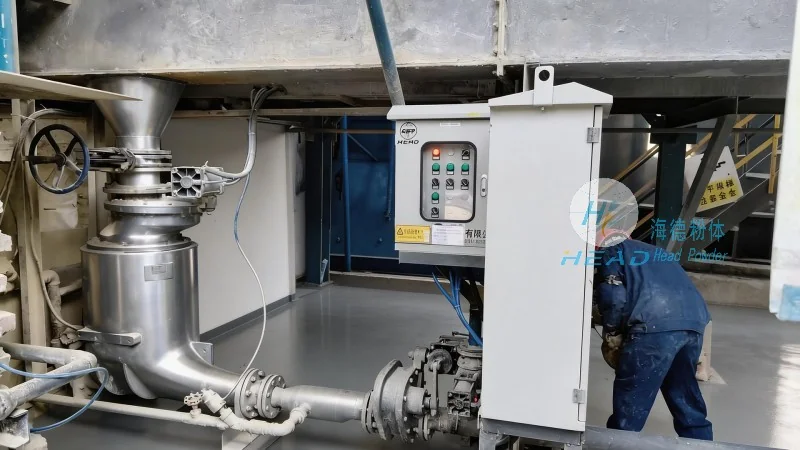
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial material handling equipment. The company specializes in the design, development, and production of dust-free systems, including tote bag loading stations, material conveying systems, and other related equipment. HeadPowder has a strong reputation in the industry for its high-quality products and reliable performance. The company is committed to providing customers with solutions that meet their specific needs and help them improve their operational efficiency and product quality. HeadPowder's products are used in a wide range of industries, including pharmaceuticals, food processing, chemical manufacturing, and more.




