Sugar powder pneumatic conveying machines are critical equipment in the sugar processing industry, designed to efficiently transport granular or powdered sugar through a pneumatic system. These machines leverage the principles of fluid dynamics and material handling to ensure safe, reliable, and efficient movement of sugar from storage to processing units. The technology is particularly suited for applications where traditional mechanical conveyors may face challenges due to the physical properties of sugar, such as its fine particle size, hygroscopic nature, or tendency to clog conventional systems.
Principles of Pneumatic Conveying for Sugar Powder
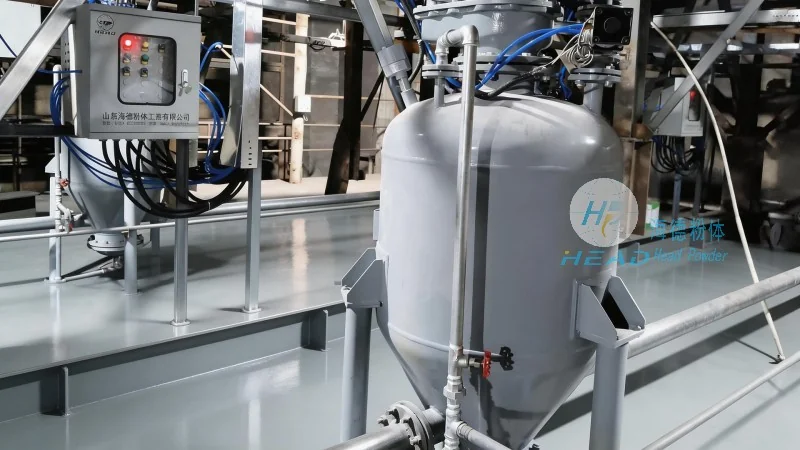
The core principle of sugar powder pneumatic conveying involves transporting the material using a pressurized or vacuum air stream within a closed pipeline system. There are two primary modes of operation: pressure conveying and vacuum conveying. In pressure conveying, compressed air is introduced into the conveying line, pushing the sugar powder forward. This method is ideal for short to medium distances and when the material needs to be delivered to multiple points. Vacuum conveying, on the other hand, uses a vacuum pump to draw the sugar powder into the pipeline, making it suitable for longer distances or when the material must be collected from multiple sources.
Within the pipeline, the sugar powder and air form a two-phase flow. The air acts as the medium that propels the powder, while the powder particles are suspended and transported. The design of the conveying system, including the size of the pipeline, the velocity of the air, and the pressure differential, is crucial for maintaining the flow and preventing blockages. For sugar powder, which is often fine and prone to agglomeration, specialized components such as cyclones, filters, and air locks are incorporated to ensure smooth operation and prevent material degradation.
Working Scene Characteristics in Sugar Processing
The working scene characteristics of sugar powder pneumatic conveying machines are tailored to the specific demands of the sugar industry. In sugar factories, these machines are commonly used in several key applications, including: transferring raw sugar from storage silos to refining equipment, moving refined sugar from the refining process to packaging lines, and handling byproducts or waste materials. The equipment is designed to handle the varying moisture content and particle size of sugar, ensuring consistent performance even under fluctuating conditions.
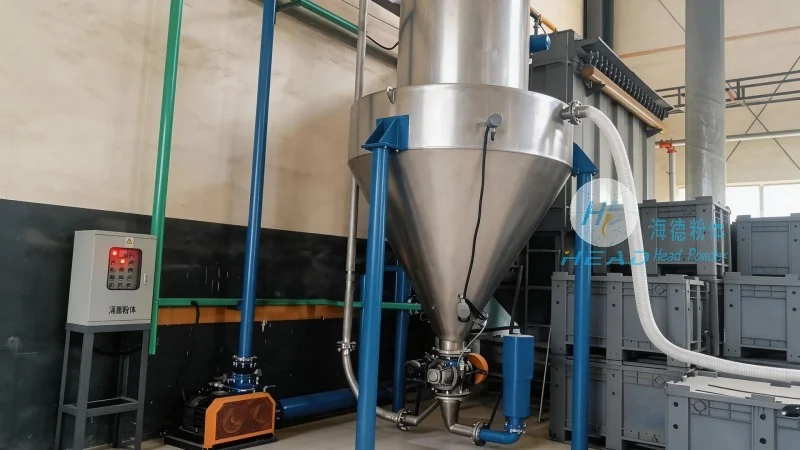
One of the key advantages of pneumatic conveying in sugar processing is its ability to maintain product purity and prevent contamination. Unlike mechanical conveyors, which may introduce dust or particles into the product stream, pneumatic systems keep the sugar enclosed within the pipeline, reducing the risk of cross-contamination. This is particularly important in food processing environments where hygiene and product quality are paramount. Additionally, the system can be integrated with other processing equipment, such as mixers or classifiers, to create a seamless production line.
HeadPowder Engineering: Custom Solutions for Sugar Conveying
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and installation of sugar powder pneumatic conveying systems tailored to the unique needs of the sugar industry. With a focus on innovation and quality, HeadPowder provides comprehensive solutions that address the specific challenges of handling sugar powder, including its hygroscopic properties and fine particle size. The company’s expertise lies in developing customized systems that optimize efficiency, reduce downtime, and ensure compliance with industry standards.
HeadPowder’s engineers work closely with clients to understand their production requirements, process flow, and material characteristics. This collaborative approach ensures that the final conveying system is optimized for performance, reliability, and cost-effectiveness. The company’s products are built with high-quality materials and advanced technology, ensuring long-term durability and minimal maintenance. By leveraging years of experience in the industry, HeadPowder delivers solutions that enhance productivity and improve overall operational efficiency in sugar processing facilities.
Key Features and Benefits of Sugar Powder Pneumatic Conveying Machines
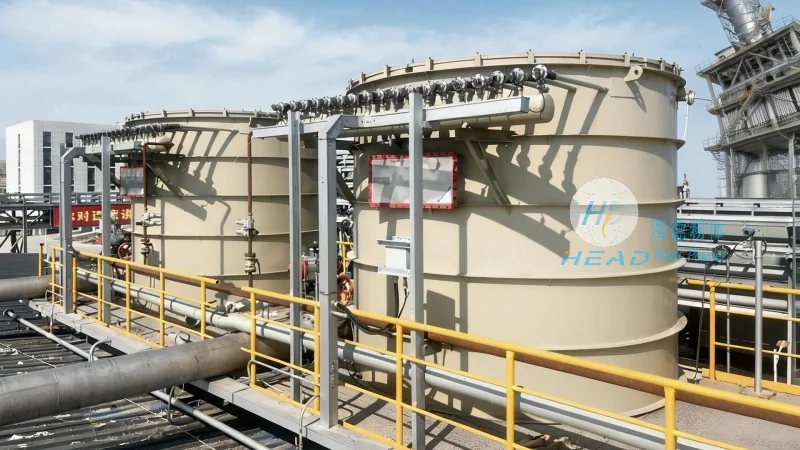
Sugar powder pneumatic conveying machines offer several distinct advantages over traditional conveying methods. These include: flexibility in layout, as the pipeline can be installed in various configurations to suit the factory layout; hygienic operation, which is essential for food-grade products; and energy efficiency, as the system can be optimized to use minimal air pressure while maintaining effective transport. Additionally, the system is less prone to clogging and can handle a wide range of particle sizes, making it suitable for both raw and refined sugar applications.
Another significant benefit is the ability to integrate the conveying system with other processing equipment, such as drying or cooling units, to create a fully automated production line. This integration reduces manual handling, minimizes the risk of human error, and improves overall product consistency. For sugar processing plants, these features translate into increased productivity, reduced labor costs, and improved product quality.
Conclusion: Enhancing Efficiency in Sugar Processing
In conclusion, sugar powder pneumatic conveying machines are indispensable tools for modern sugar processing facilities. By leveraging the principles of pneumatic transport and tailored to the specific characteristics of sugar powder, these machines ensure efficient, reliable, and hygienic movement of sugar throughout the production process. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing customized solutions that meet the evolving needs of the sugar industry, helping manufacturers enhance productivity and maintain high standards of quality and safety.




