Working Principle and Characteristics of Coal Ash Powder Pneumatic Conveying Systems
Release time:2026-09-18 02:01:27
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced pneumatic conveying systems. With a focus on industrial applications involving coal ash and other fine powders, the company has established itself as a reliable partner for clients seeking efficient and reliable material transport solutions. HeadPowder's expertise lies in optimizing the performance of pneumatic conveying systems, ensuring high efficiency, low maintenance, and durability in demanding industrial environments.
Working Principle of Coal Ash Powder Pneumatic Conveying Systems
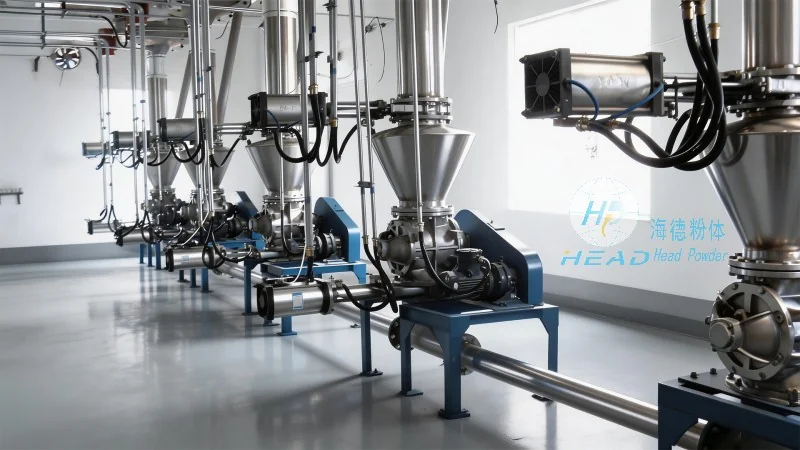
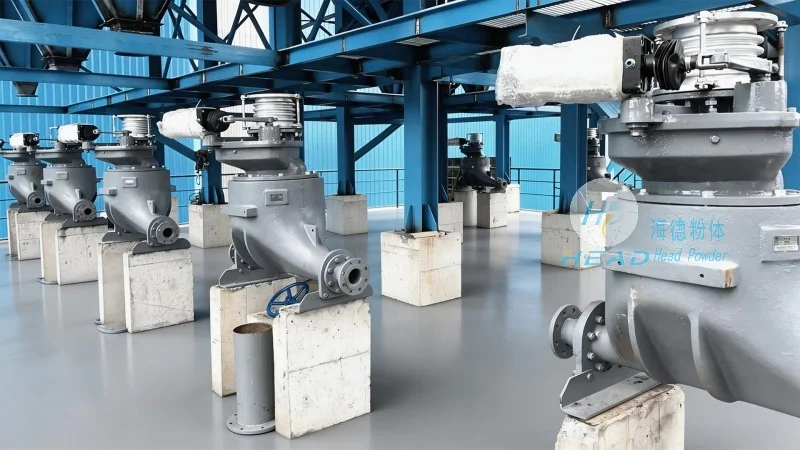
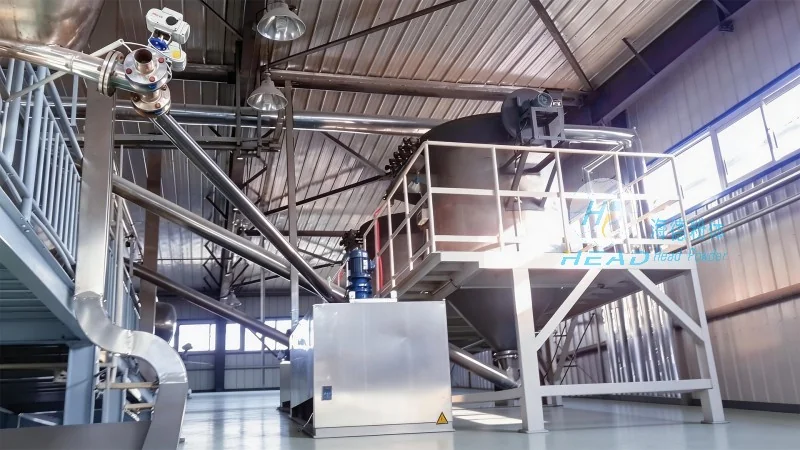
The working principle of a coal ash powder pneumatic conveying system involves the use of an air stream to transport fine particles of coal ash through a pipeline. The system operates by creating a pressure differential between the inlet and outlet of the conveying line. In positive pressure systems, an air compressor generates the necessary pressure to push the coal ash particles through the pipeline. The air velocity is maintained at a level that ensures the particles are fully entrained, preventing settling or blockages. The conveying line is typically made of materials such as stainless steel or plastic, chosen for their resistance to corrosion and wear from the coal ash particles. At the discharge end, a separator and filter system removes the air from the coal ash, allowing the material to be collected in a designated container. The air is then filtered to remove any residual ash particles before being released back into the environment or recirculated. This closed-loop system minimizes waste and ensures that the coal ash is handled in a controlled manner, reducing environmental impact. The system's efficiency is further enhanced by the use of optimized pipeline layouts and components, such as bends with low pressure drop and efficient valves for controlling the flow rate.
Key Characteristics and Advantages of Coal Ash Powder Pneumatic Conveying Systems
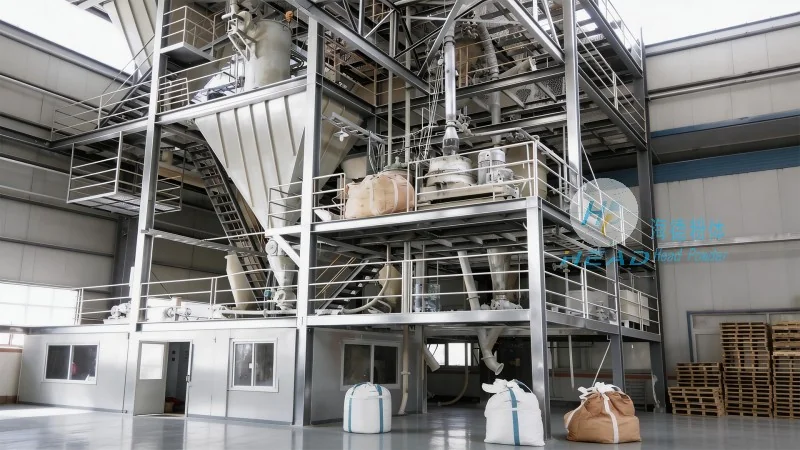
Key characteristics of coal ash powder pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. include high efficiency and low energy consumption. The systems are designed to transport large quantities of coal ash over long distances with minimal power input, making them cost-effective for industrial operations. The closed system design prevents dust emissions, which is essential for maintaining a safe and clean working environment. This is particularly important in power plants and cement factories where coal ash is a byproduct and needs to be transported to processing facilities. Another key characteristic is the flexibility and adaptability of the system. HeadPowder's engineers can customize the system to meet specific client needs, including varying the pipeline length, diameter, and configuration to suit the layout of the industrial site. The modular design allows for easy installation and modification, reducing the time and cost associated with system integration. The systems also offer precise control over the material flow, enabling accurate dosing of coal ash in processes such as cement production or concrete mixing. This control is achieved through advanced control systems that monitor the pressure, flow rate, and particle size, ensuring consistent performance. Additionally, the systems are built for durability and low maintenance. High-quality materials and robust construction ensure that the equipment can withstand the harsh conditions of industrial environments, including high temperatures and abrasive particles. This reduces the need for frequent repairs and replacements, lowering the total cost of ownership. The safety features of the system are also noteworthy. By eliminating manual handling of coal ash, the system minimizes the risk of dust inhalation and related health issues. The closed system also prevents accidental spills or leaks, protecting both the environment and the workforce. Overall, the characteristics of these systems make them a preferred choice for industries that require reliable, efficient, and environmentally friendly material transport solutions.




