

Principle and Working Scene Characteristics of Ammonium Nitrate Pneumatic Conveying Machines
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for handling ammonium nitrate. The company's expertise lies in developing efficient solutions that ensure safe and reliable material transport in industrial settings.
Principle of Ammonium Nitrate Pneumatic Conveying Systems
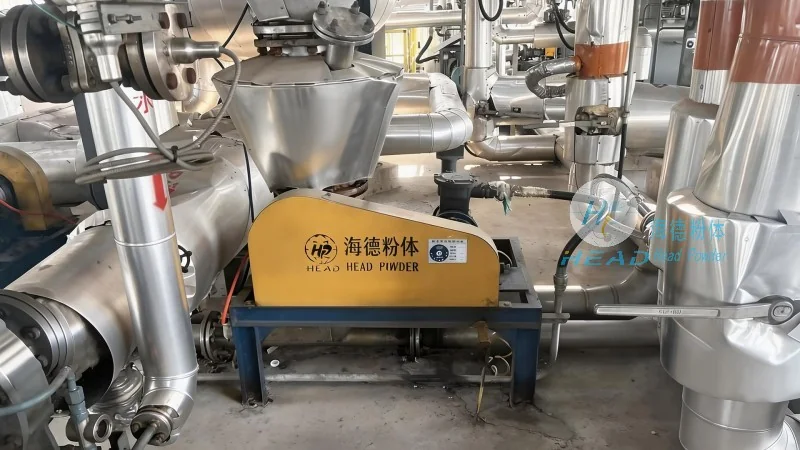
The core principle of ammonium nitrate pneumatic conveying machines involves using a pressurized air stream to transport bulk materials through a pipeline. In this system, a blower or compressor generates the necessary air pressure, which then propels the ammonium nitrate particles along the conveying line. The process typically operates under positive pressure, where the air flow moves the material from the source to the destination, minimizing the risk of dust dispersion and ensuring a clean transfer. The design incorporates features such as air filtration and material separation to maintain product purity and operational safety. The system's efficiency is enhanced by adjustable air flow rates and pressure controls, allowing for precise control over the conveying speed and material handling capacity.
Working Scene Characteristics and Application Scenarios
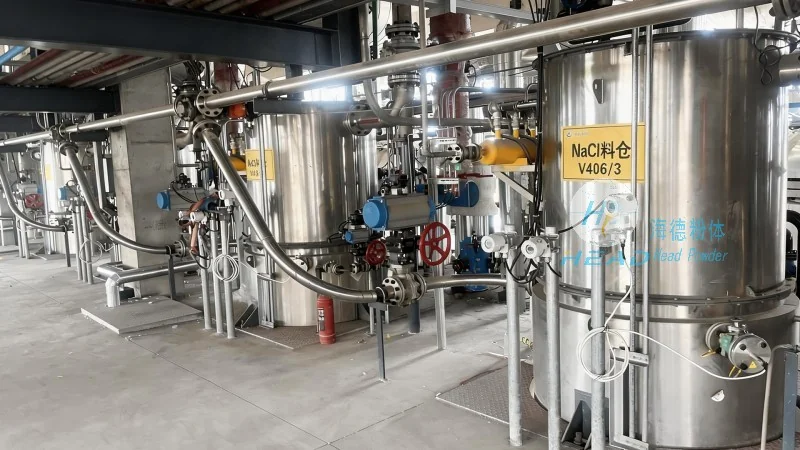
Ammonium nitrate pneumatic conveying machines are widely utilized in various industrial environments, particularly in fertilizer production, chemical processing, and material handling facilities. The working scene characteristics of these systems are tailored to meet the specific demands of each application. For instance, in fertilizer manufacturing plants, the equipment is designed to handle large volumes of ammonium nitrate, ensuring seamless integration with production lines and storage systems. The compact design and low maintenance requirements make it suitable for both new installations and retrofitting existing facilities. In chemical processing plants, the system's ability to transport materials under controlled conditions is crucial for maintaining product quality and adhering to safety regulations. The working scene also includes applications in mining and construction industries, where the equipment is used to transport ammonium nitrate from storage silos to processing units or loading areas. The adaptability of the system allows it to operate in diverse environments, from indoor processing facilities to outdoor storage and handling areas, ensuring flexibility in industrial operations.
Key Features and Advantages in Practical Applications
When considering the practical application of ammonium nitrate pneumatic conveying machines, several key features stand out. The positive pressure system effectively prevents dust leakage and maintains a controlled environment, which is critical for handling ammonium nitrate, a material that requires strict safety measures due to its potential hazards. The system's ability to handle abrasive materials without causing excessive wear to the equipment is another significant advantage. This durability ensures long-term operational efficiency and reduces maintenance costs over the equipment's lifespan. Additionally, the flexibility in conveying distances and the ability to integrate with existing infrastructure make these machines a cost-effective solution for many industrial needs. The design also incorporates safety features such as pressure relief valves and emergency shutdown systems, ensuring compliance with industry standards and protecting personnel and equipment from potential risks. These features collectively contribute to the reliability and performance of the system in real-world working scenarios.
Conclusion on Working Efficiency and Industry Integration
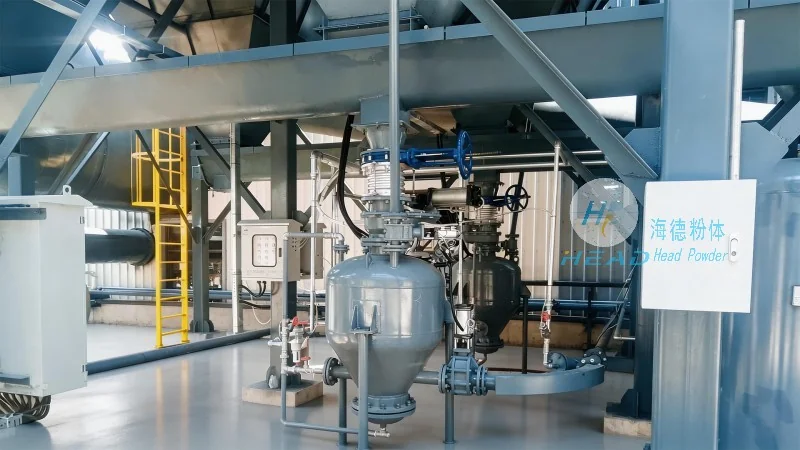
In conclusion, the ammonium nitrate pneumatic conveying machines developed by Shandong HeadPowder Engineering Co., Ltd. represent a sophisticated solution for efficient and safe material handling in industrial applications. The combination of advanced engineering principles and practical design considerations ensures that these systems meet the demanding requirements of modern industrial operations. By leveraging the company's expertise in pneumatic conveying technology, users can expect enhanced productivity, reduced operational risks, and improved overall performance in their working environments. The working scene characteristics and application scenarios highlight the versatility and adaptability of these machines, making them an essential component in various industrial settings where ammonium nitrate is processed and transported.