For industrial applications involving the transport of dry pebble powders, specialized conveying systems are essential to ensure efficient and reliable material handling. This article provides an in-depth look at the working principle and key features of dry pebble powder conveying systems, with a focus on the technology offered by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field.
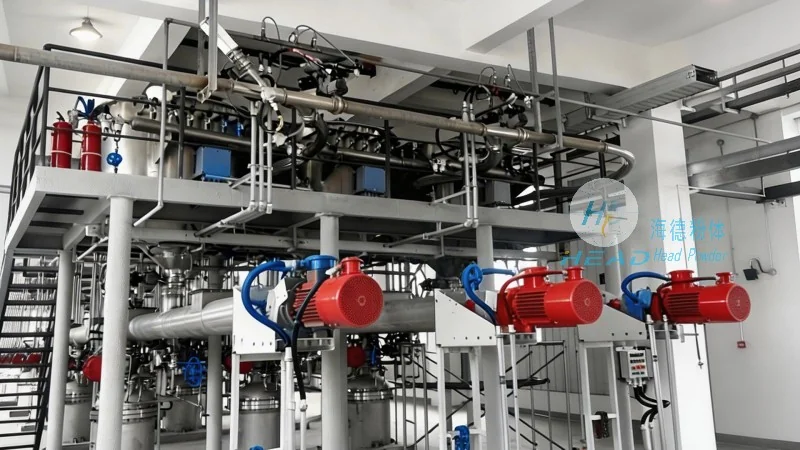
Introduction to Dry Pebble Powder Conveying Systems
Dry pebble powder conveying systems are designed to move bulk materials such as crushed stone, gravel, or other granular powders without the use of water or other binding agents. These systems are critical in industries like mining, construction, and chemical processing, where the efficient transport of these materials is vital for operational productivity. The systems typically consist of components like feeders, conveyors, and control mechanisms that work together to ensure smooth and continuous material flow.
The Working Principle of Dry Pebble Powder Conveying Systems
The core working principle of dry pebble powder conveying systems revolves around the use of mechanical forces to move the material from the source to the destination. A common method involves the use of screw conveyors or pneumatic systems, depending on the specific requirements of the application. In screw conveyors, a rotating screw or auger pushes the material forward through a trough or pipe. This method is particularly effective for materials that are free-flowing and non-abrasive. For more challenging materials or longer distances, pneumatic conveying systems use air pressure to transport the powder through a pipeline. The system typically includes a hopper to feed the material, a blower to generate the air flow, and a receiver to collect the material at the end of the line.
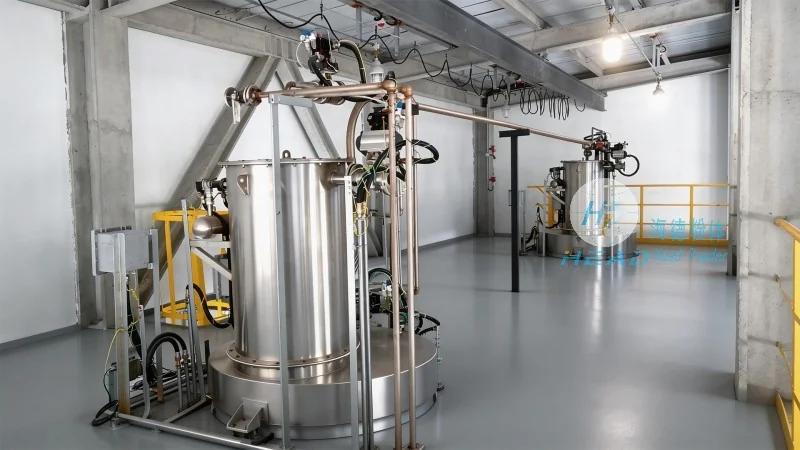
Key Features of Dry Pebble Powder Conveying Systems
Shandong HeadPowder Engineering Co., Ltd. offers dry pebble powder conveying systems with several notable features that enhance performance and reliability. One key feature is the robust construction, which is designed to withstand the abrasive nature of pebble powders and the mechanical stresses associated with continuous operation. The systems are often equipped with adjustable speed controls, allowing operators to modulate the flow rate based on the specific needs of the process. This flexibility is crucial for maintaining consistent material delivery and preventing overloading or underloading of downstream equipment.
Another important feature is the integration of dust control mechanisms. Since dry powders can generate significant dust during handling, the systems are typically equipped with sealed housings and dust collection systems to minimize environmental impact and ensure operator safety. Additionally, the systems may include monitoring and alarm systems that provide real-time feedback on operational parameters, such as flow rate and pressure, enabling proactive maintenance and reducing downtime.
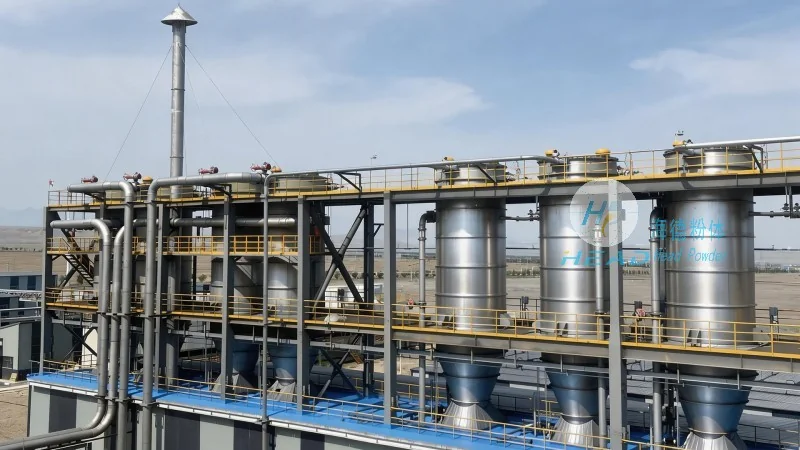
Application-Specific Design and Customization
HeadPowder Engineering recognizes that different industrial applications have unique requirements. Therefore, their dry pebble powder conveying systems are designed with modularity and adaptability in mind. Customers can choose from a range of configurations, including horizontal, vertical, or inclined conveyors, to suit their specific layout and operational constraints. The company also offers customization options, such as the use of special materials for the conveyor components to resist corrosion or wear, ensuring the system's longevity and performance in harsh environments.
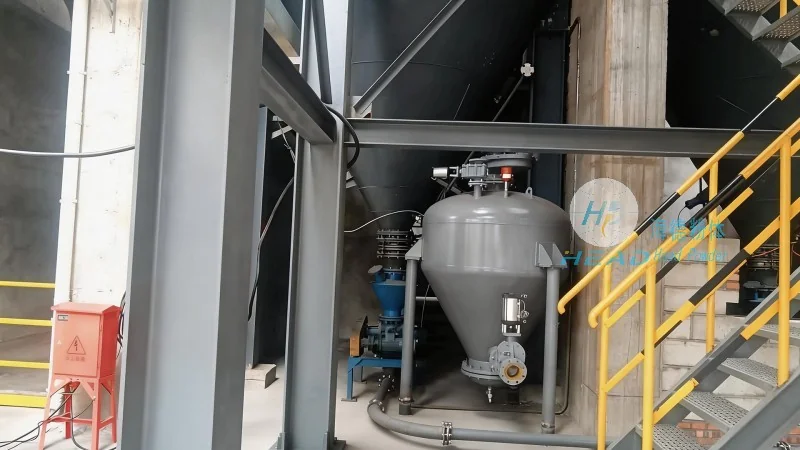
Benefits of Using Dry Pebble Powder Conveying Systems
Implementing a dry pebble powder conveying system from Shandong HeadPowder Engineering Co., Ltd. offers several significant benefits for industrial operations. The primary advantage is improved efficiency, as these systems can handle large volumes of material with minimal labor intervention. This leads to increased productivity and reduced operational costs. Additionally, the systems contribute to better safety by minimizing manual handling of powders and reducing dust exposure for workers. The reliability of the equipment, with features like automatic controls and monitoring systems, further reduces the risk of material loss or system failures, ensuring consistent and dependable performance.
Conclusion
In summary, dry pebble powder conveying systems are essential equipment for industries dealing with bulk dry materials. The working principle, which often involves mechanical or pneumatic forces, is designed to efficiently transport these materials while maintaining product integrity. The key features offered by manufacturers like Shandong HeadPowder Engineering Co., Ltd., including robust construction, adjustable controls, and dust management, enhance the system's performance and reliability. By understanding these principles and features, industrial operators can make informed decisions when selecting the most suitable conveying system for their specific needs, ultimately improving operational efficiency and safety.




