HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced dust collection and powder material handling solutions. The dust collection powder material handling system equipment is a critical component in industrial processes that require efficient and safe transportation of fine powders and dust particles. This system is designed to capture airborne particles, transport them through a network of pipes or other conduits, and deposit them in a designated storage or disposal area. Understanding the design principles behind such systems is essential for optimizing performance, ensuring compliance with environmental regulations, and maintaining operational efficiency.
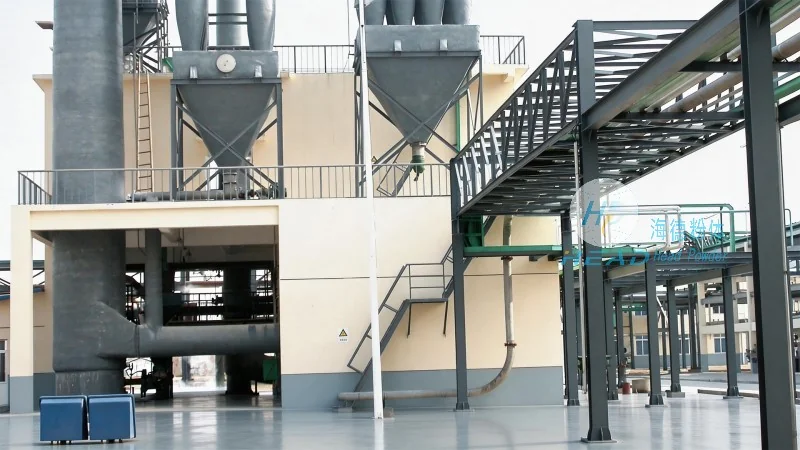
Key Components of the Dust Collection Powder Material Handling System
The system typically consists of several key components that work in tandem to achieve effective material handling. The primary components include a dust collector, which captures and filters the airborne particles; a conveying system, such as a pneumatic or mechanical conveyor, that transports the collected material; and a storage or discharge unit where the material is deposited. Each component plays a crucial role in the overall functionality of the system. The dust collector may utilize various filtration technologies, including bag filters, cartridge filters, or electrostatic precipitators, depending on the specific application and the nature of the dust particles. The conveying system, on the other hand, may employ positive or negative pressure systems to move the material through the pipeline. The storage or discharge unit ensures that the material is handled safely and efficiently, preventing re-entrainment and ensuring proper disposal or reuse.
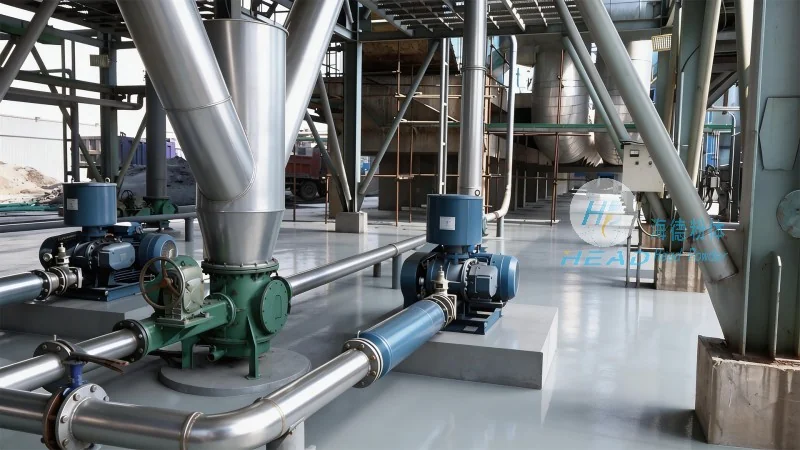
Design Principles for Efficient Material Handling
The design principles of a dust collection powder material handling system are centered on several key factors, including efficiency, reliability, and safety. One of the fundamental principles is the selection of appropriate filtration technology that matches the characteristics of the dust particles, such as particle size, moisture content, and chemical composition. This ensures optimal filtration efficiency and minimizes the risk of filter clogging or failure. Another critical principle is the design of the conveying system, which must be able to handle the specific flow rates and pressure requirements of the material. The system should be designed to minimize pressure drop and energy consumption, as these factors directly impact operational costs and efficiency. Additionally, the system must be constructed from materials that are compatible with the material being handled, to prevent corrosion or contamination. The layout and configuration of the system, including the placement of the dust collector, conveying lines, and storage units, are also crucial for maximizing efficiency and minimizing the risk of blockages or leaks.
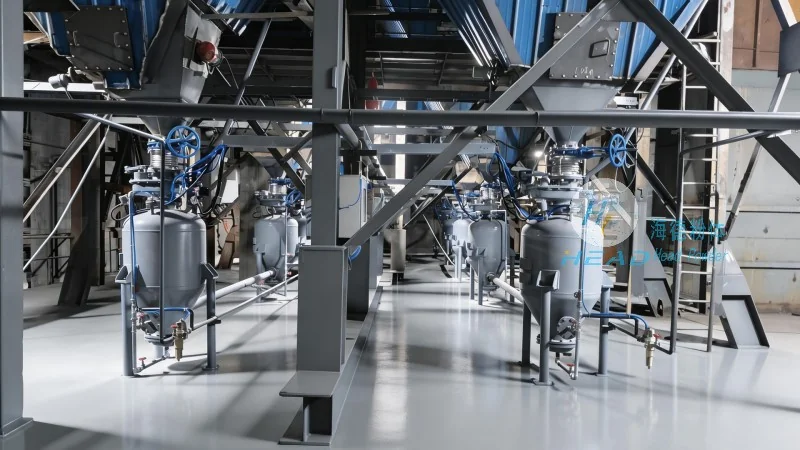
Applications and Benefits of the System
The dust collection powder material handling system equipment is widely used in various industrial sectors, including manufacturing, mining, and food processing. In manufacturing, it is used to handle powders such as plastics, chemicals, and pharmaceuticals, ensuring a clean and safe working environment. In mining, it is used to transport and store dust and ore particles, improving operational efficiency and reducing environmental impact. The benefits of using such a system include improved air quality, reduced health risks for workers, and increased productivity due to the efficient handling of materials. Additionally, the system helps in complying with environmental regulations by minimizing dust emissions and ensuring proper disposal of waste materials. The design principles discussed above contribute to these benefits by ensuring that the system operates efficiently and reliably, with minimal downtime and maintenance requirements.
Conclusion
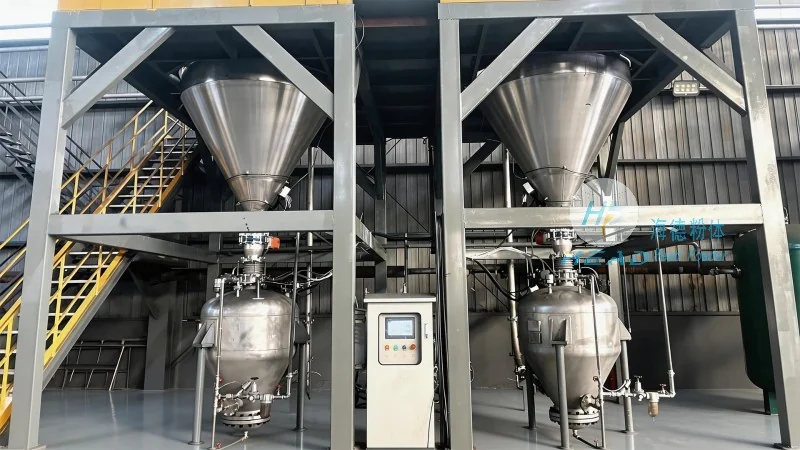
HeadPowder's dust collection powder material handling system equipment is designed to meet the diverse needs of industrial applications, combining advanced technology with robust engineering principles. By adhering to the design principles outlined above, the system ensures optimal performance, reliability, and safety, making it an essential solution for industries dealing with fine powders and dust. With a focus on efficiency and compliance, this equipment helps businesses maintain a clean, safe, and productive working environment while minimizing environmental impact.




