High-calcium stone powder, widely utilized in industrial sectors such as cement production, steel manufacturing, and chemical processing, demands specialized material handling systems to ensure efficient and safe transport. The design of a high-calcium stone powder material handling system involves meticulous consideration of the material's properties, operational requirements, and safety standards. This article delves into the core components and design principles behind such systems, emphasizing the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading entity in the material handling engineering field.
Understanding High-Calcium Stone Powder and Its Handling Challenges
High-calcium stone powder is defined by its fine particle size, high density, and abrasive characteristics. These traits render conventional handling methods—like manual loading or basic conveyor setups—inadequate for maintaining efficiency and preventing equipment wear. The material's reactivity and propensity for dust generation further necessitate advanced solutions to ensure environmental compliance and worker safety. Shandong HeadPowder Engineering Co., Ltd. addresses these challenges by designing systems tailored to the unique demands of high-calcium stone powder, leveraging decades of experience in material handling engineering.
Core Components of a High-Calcium Stone Powder Material Handling System
The foundation of an effective high-calcium stone powder material handling system comprises several critical components, each integral to the overall operation. These components are selected and integrated based on specific application requirements, ensuring optimal performance and durability. Key elements typically include:
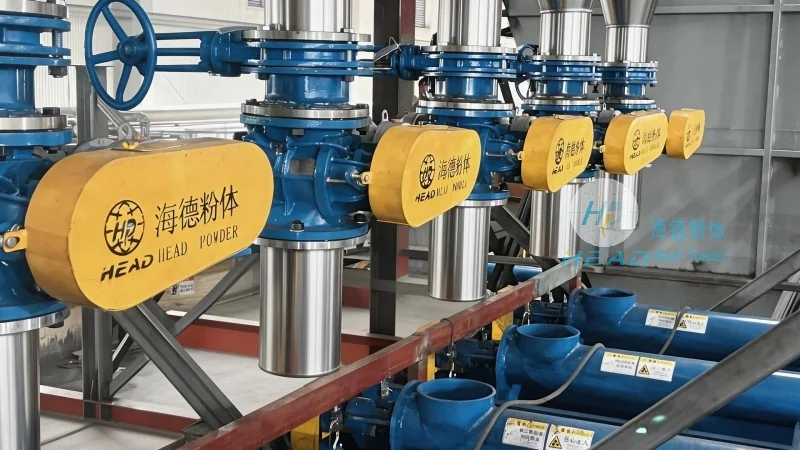
1. Feeding Equipment: This component, often a rotary valve or screw feeder, regulates the flow of high-calcium stone powder from storage silos or hoppers into the main conveyor system. The design of the feeding equipment is crucial to prevent material bridging and ensure a consistent feed rate, directly impacting downstream process efficiency.
2. Conveyor Systems: For long-distance transport, belt conveyors or pneumatic conveying lines are commonly employed. Belt conveyors are preferred for their ability to handle large volumes and maintain stable flow, while pneumatic systems suit finer powders or when dust control is a priority. The selection of the conveyor type depends on factors like particle size distribution, moisture content, and required transport distance.
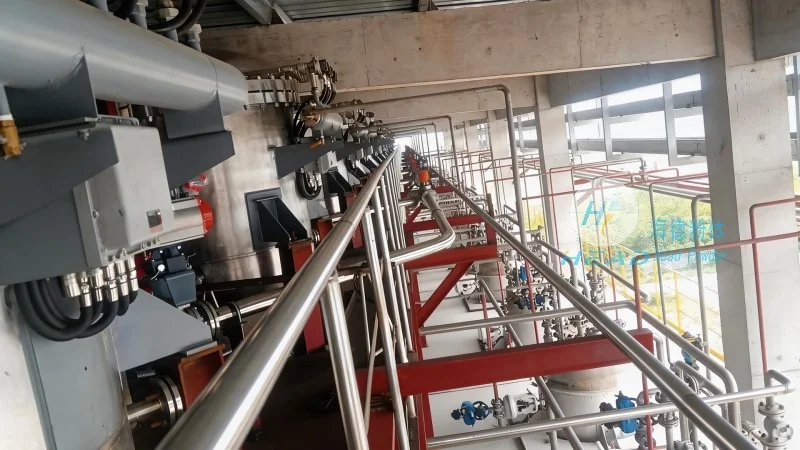
3. Dust Control Systems: High-calcium stone powder is prone to generating dust, posing health and environmental risks. Effective dust control is achieved through sealed equipment, air filtration systems, and proper ventilation. Shandong HeadPowder Engineering Co., Ltd. incorporates advanced dust suppression technologies, such as cyclone separators and baghouse filters, to minimize emissions and maintain a safe working environment.
4. Storage and Silo Systems: Large-scale operations often require storage silos to accommodate bulk quantities of high-calcium stone powder. These silos are designed with reinforced structures to withstand material weight and internal air pressure. They are equipped with level indicators and pressure relief valves to ensure safe operation and prevent overfilling.
Design Principles for Optimal Performance
The design of a high-calcium stone powder material handling system follows several key principles to ensure reliability, efficiency, and longevity. These principles are guided by the material's physical properties and operational goals. Primary considerations include:
1. Material Compatibility: All system components—conveyors, hoppers, and valves—must be constructed from materials resistant to the abrasive and corrosive nature of high-calcium stone powder. Stainless steel, special alloys, and wear-resistant coatings are commonly used to extend equipment lifespan and reduce maintenance costs.
2. Flow Optimization: The system is designed to minimize material buildup and ensure smooth flow through the entire process. This involves proper hopper design, conveyor incline angles, and the use of vibration or air-assisted feeding mechanisms. Optimizing flow reduces blockage risks and improves overall throughput.
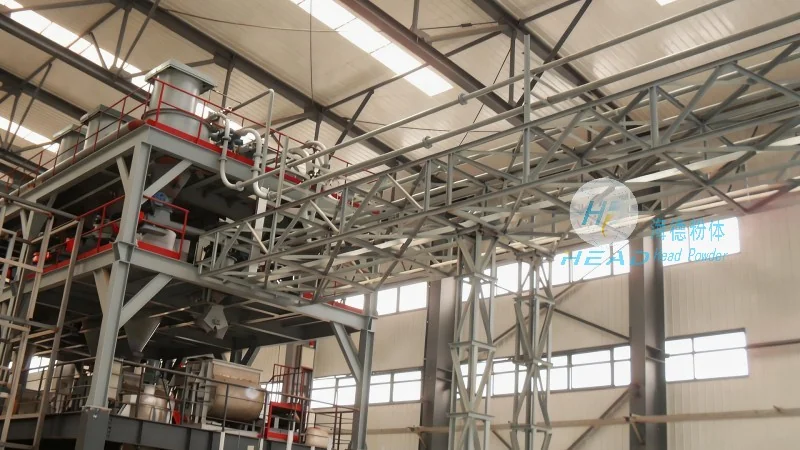
3. Safety and Environmental Compliance: Compliance with local regulations and industry standards is a top priority. The system incorporates safety features such as emergency stop buttons, interlocks, and monitoring systems to prevent accidents. Additionally, dust control measures are integrated to meet environmental emission standards, ensuring sustainable and responsible operation.
4. Modularity and Scalability: Modern high-calcium stone powder material handling systems are designed with modularity in mind, allowing for easy expansion or modification as production needs evolve. This flexibility enables users to adapt the system to future requirements without significant re-engineering, providing long-term value.
Case Study: A High-Calcium Stone Powder Handling Solution by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented high-calcium stone powder material handling systems for various clients across China. One notable project involved supplying a complete system to a cement manufacturing plant in Shandong province. The system included a 500-ton storage silo, a belt conveyor for long-distance transport, and a dust control unit. The design incorporated wear-resistant components to handle the abrasive nature of the high-calcium stone powder, resulting in a system with a service life exceeding 10 years. The client reported significant improvements in production efficiency and reduced maintenance costs, validating the effectiveness of the design principles applied.
Conclusion
High-calcium stone powder material handling systems are critical to the efficient operation of industries reliant on this material. The design principles, components, and expertise of companies like Shandong HeadPowder Engineering Co., Ltd. play a pivotal role in ensuring these systems meet the demands of modern industrial applications. By focusing on material compatibility, flow optimization, safety, and scalability, such systems provide reliable, cost-effective solutions that enhance productivity and sustainability. For businesses seeking to upgrade or install a high-calcium stone powder material handling system, partnering with a reputable engineering firm like Shandong HeadPowder Engineering Co., Ltd. is essential to achieve optimal results.




