When it comes to industrial material handling, especially in environments where dust control and efficient material transfer are critical, the tonne bag dust-free feeding station plays a pivotal role. This system is engineered to handle bulk materials from tonne bags with minimal dust generation and optimal operational efficiency. Understanding its core components and design principles is essential for industries such as pharmaceuticals, food processing, and chemical manufacturing, where maintaining a clean and safe working environment is paramount.
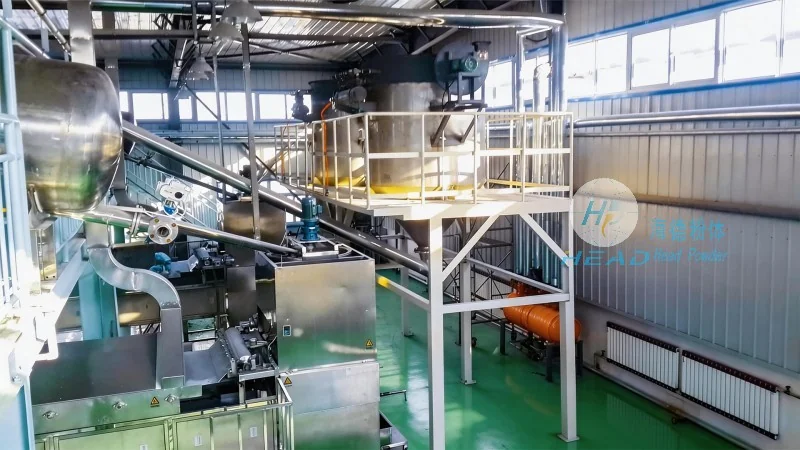
About HeadPowder: Your Trusted Partner in Material Handling Solutions
HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and supplying advanced material handling equipment. With a strong commitment to quality and innovation, HeadPowder has established itself as a reliable partner for businesses seeking efficient and dust-free material processing solutions. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to develop cutting-edge systems tailored to diverse industrial needs.
Design Principles of the Tonne Bag Dust-Free Feeding Station
The design of a tonne bag dust-free feeding station is centered around several key principles aimed at maximizing efficiency while minimizing dust exposure. The primary goal is to ensure that bulk materials are transferred from the tonne bag into the processing equipment without generating excessive airborne particles. This is achieved through a combination of sealed hopper designs, advanced filtration systems, and controlled material flow mechanisms.
One of the fundamental components is the sealed hopper, which is specifically designed to receive the tonne bag and maintain a closed environment. The hopper is equipped with a lid that can be securely fastened, preventing dust from escaping during material transfer. Additionally, the hopper is often integrated with a dust collection system that captures any particles that may be generated, ensuring that the air is clean and safe for the operators.
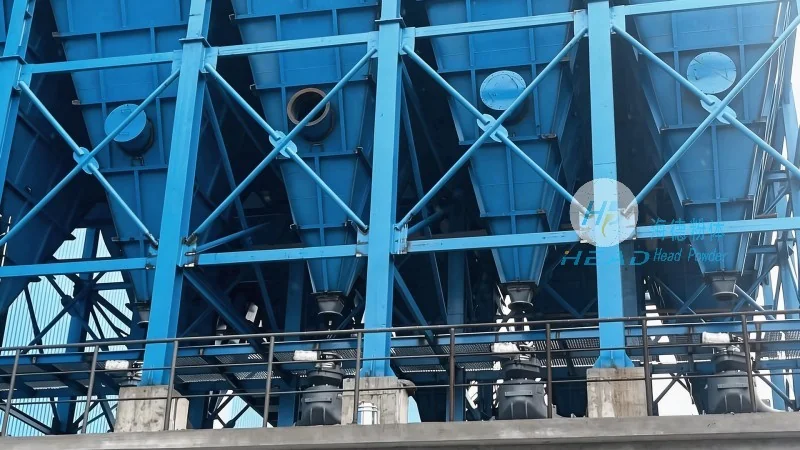
Material flow control is another critical aspect of the design. The system typically includes a screw conveyor or a rotary valve that regulates the flow of material from the hopper into the downstream equipment. This control mechanism allows for precise dosing and prevents overloading or underloading of the processing machinery. The design also considers the mechanical properties of the bulk material, ensuring that the equipment can handle various types of materials without causing blockages or wear.
Sealing and filtration are integral to the overall design. The feeding station is equipped with high-efficiency filters that capture dust particles, ensuring that the air is clean and compliant with environmental regulations. The sealing system is designed to maintain a negative pressure within the hopper, which helps to prevent dust from escaping into the surrounding environment. This negative pressure is maintained by the dust collection system, which continuously draws air through the filters, removing contaminants before releasing it back into the facility.
Key Features and Benefits of the Material Handling System
The tonne bag dust-free feeding station offers several key features that enhance operational performance and safety. The primary benefit is the reduction of dust exposure, which is crucial for maintaining a clean and safe working environment. By minimizing dust generation, the system helps to prevent respiratory issues among workers and reduces the risk of fire or explosion in flammable environments.
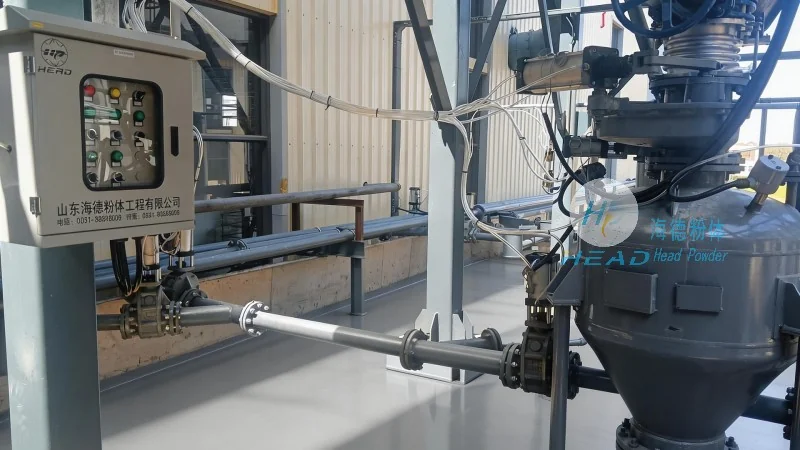
Another significant advantage is the improved material handling efficiency. The system allows for continuous and uninterrupted material transfer, reducing downtime and increasing overall productivity. The precise flow control ensures that the processing equipment receives the exact amount of material needed, preventing overloading or underloading, which can lead to equipment damage or product quality issues.
Additionally, the sealed design of the system helps to maintain the integrity of the material being handled. This is particularly important for sensitive materials, such as pharmaceuticals or food products, where contamination must be strictly avoided. The system also helps to prevent cross-contamination between different batches of materials, ensuring that each product remains pure and free from impurities.
Conclusion: Enhancing Material Handling with Advanced Solutions
In conclusion, the tonne bag dust-free feeding station material handling system is a sophisticated solution designed to address the challenges of bulk material transfer in industrial settings. By integrating advanced design principles, such as sealed hoppers, efficient filtration, and precise flow control, this system provides a reliable and safe method for handling tonne bags while minimizing dust exposure. HeadPowder, with its expertise in material handling equipment, offers these systems tailored to meet the specific needs of various industries, ensuring optimal performance and compliance with safety and environmental standards.




